Active ammonia denitration systems represent a critical technology in modern industrial emissions control, designed to reduce nitrogen oxide (NOx) emissions from combustion processes. These systems utilize ammonia as a reducing agent to chemically convert NOx into nitrogen and water, thereby meeting stringent environmental regulations. The following sections will explore the fundamental principles behind these systems and the specific working scenarios where they are most effectively applied, along with an overview of the company, Shandong HeadPowder Engineering Co., Ltd., which specializes in such advanced environmental solutions.
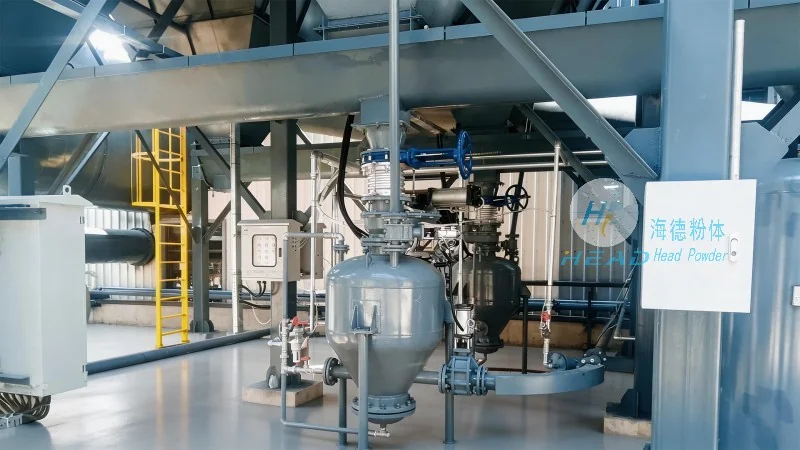
The active ammonia denitration system operates on the principle of selective catalytic reduction (SCR). In this process, ammonia (NH₃) is injected into the flue gas stream, where it reacts with NOx under specific temperature and catalyst conditions. The key chemical reactions involved are as follows: 4NH₃ + 4NO + O₂ → 4N₂ + 6H₂O and 8NH₃ + 6NO₂ → 7N₂ + 12H₂O. These reactions are facilitated by a catalyst, typically made of titanium dioxide (TiO₂) or other metal oxides, which accelerates the conversion rate while maintaining operational efficiency. The system is designed to achieve high NOx removal efficiencies, often exceeding 90% under optimal conditions. The control of ammonia slip is a critical aspect, as excessive ammonia can lead to secondary pollution, and thus precise dosing and monitoring are essential for maintaining compliance with environmental standards.
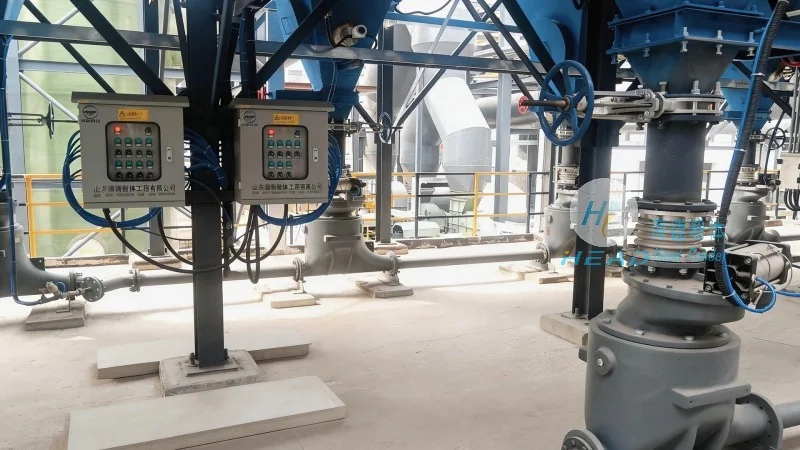
Active ammonia denitration systems are widely deployed in various industrial settings where NOx emissions are a concern. The primary working scenarios include power plants (both thermal and combined-cycle), industrial boilers, and industrial furnaces. In power plants, these systems are typically installed in the flue gas desulfurization (FGD) outlet or downstream of the boiler, where the gas temperature is optimized for efficient NOx reduction. The working environment involves high-temperature flue gases (usually between 300°C to 450°C) and requires robust system design to withstand the harsh conditions. For industrial boilers, the systems are often integrated into the exhaust system of boilers used in manufacturing, chemical processing, and other industrial sectors. The working scene also includes considerations such as the composition of the flue gas (e.g., presence of sulfur dioxide, particulate matter), which may affect the catalyst performance and system efficiency. Additionally, the system's adaptability to different fuel types, such as coal, natural gas, or biomass, makes it suitable for diverse industrial applications. The working characteristics emphasize continuous operation, with minimal downtime for maintenance, and the ability to handle varying load conditions in industrial processes.
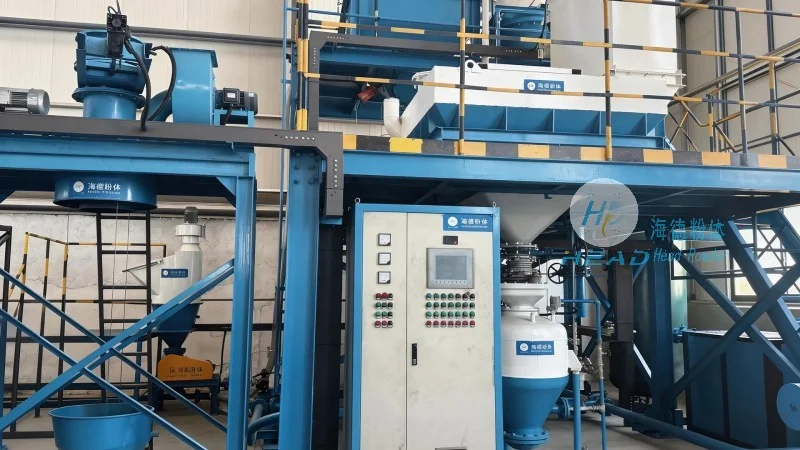
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading provider of environmental engineering solutions, specializing in the design, manufacturing, and installation of active ammonia denitration systems. With a strong focus on technological innovation and environmental compliance, the company has established itself as a trusted partner in the industrial emissions control sector. HeadPowder's headquarters is located in Shandong, China, where the company leverages local expertise and resources to deliver high-quality products and services. The company adheres to international standards and continuously invests in research and development to enhance the performance and efficiency of its denitration systems. By combining advanced engineering with practical application experience, HeadPowder ensures that its systems meet the specific needs of clients across various industries, contributing to cleaner air and sustainable industrial operations.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top