Pneumatic conveying systems have become a cornerstone in the handling and transportation of bulk materials, especially for industries dealing with granular substances like pearl salt. The technology offers a reliable, efficient, and often cost-effective solution for moving materials from one location to another without the need for mechanical components like belts or buckets. For companies in the food processing, chemical, or industrial sectors, understanding the working principle and key features of such systems is crucial for optimizing operations and ensuring product integrity.
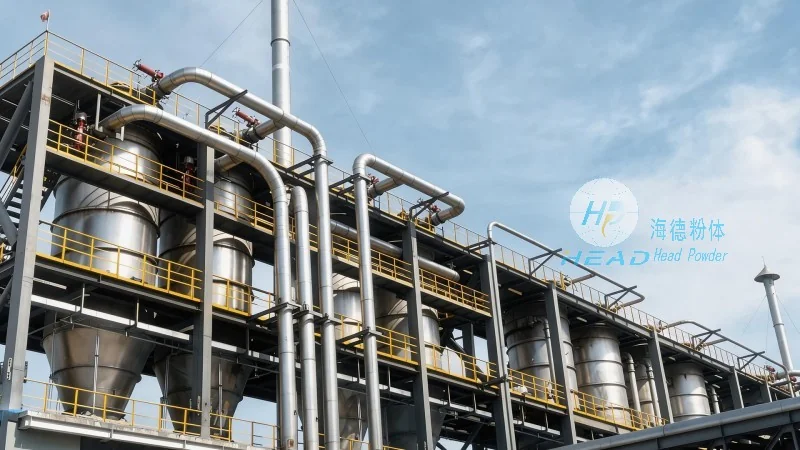
At the core of a pneumatic conveying system is the use of compressed air or gas as the primary transport medium. The system typically consists of a hopper or feeder where the pearl salt granules are stored, a blower or compressor that generates the air flow, and a pipeline network that guides the material from the source to the destination. The process begins when the material is introduced into the hopper, and a controlled amount of air is blown into the system. This creates a pressure differential that lifts the granules and propels them through the pipeline. The air velocity is carefully managed to ensure that the particles are carried without causing excessive wear or degradation, which is particularly important for delicate materials like pearl salt.
The system can operate in either dilute-phase or dense-phase modes. Dilute-phase conveying uses higher air velocities to transport the material in a dispersed state, suitable for short-distance or low-volume applications. Dense-phase conveying, on the other hand, uses lower air velocities and higher material concentration, which is ideal for longer distances or when maintaining product quality is paramount. For pearl salt, the choice of mode depends on factors such as the distance between the source and destination, the required flow rate, and the need to prevent segregation or attrition of the granules.
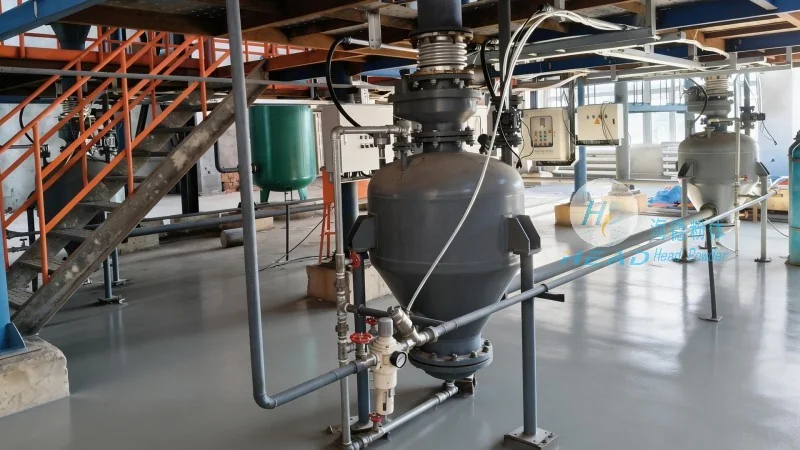
Several distinct features make pneumatic conveying systems particularly advantageous for handling pearl salt granules. First, the system offers a high degree of flexibility in terms of layout and installation. Unlike traditional mechanical conveyors, pneumatic systems can be easily reconfigured or expanded to accommodate changes in production volume or facility layout. This adaptability is crucial for dynamic industrial environments where processes may evolve over time.
Second, pneumatic conveying is inherently clean and hygienic, which is a critical consideration for food-grade materials like pearl salt. The enclosed pipeline system prevents contamination from external sources and minimizes dust exposure, ensuring that the product remains free from impurities and adheres to stringent quality standards. This is particularly important in industries where product purity directly impacts consumer safety and brand reputation.
Third, the system provides excellent control over the flow rate and pressure, allowing for precise regulation of material movement. This precision is essential for maintaining consistent production rates and preventing overloading or underloading of downstream equipment. For pearl salt processing, where uniformity in granule size and density is critical, this control feature helps maintain product quality and reduce waste.
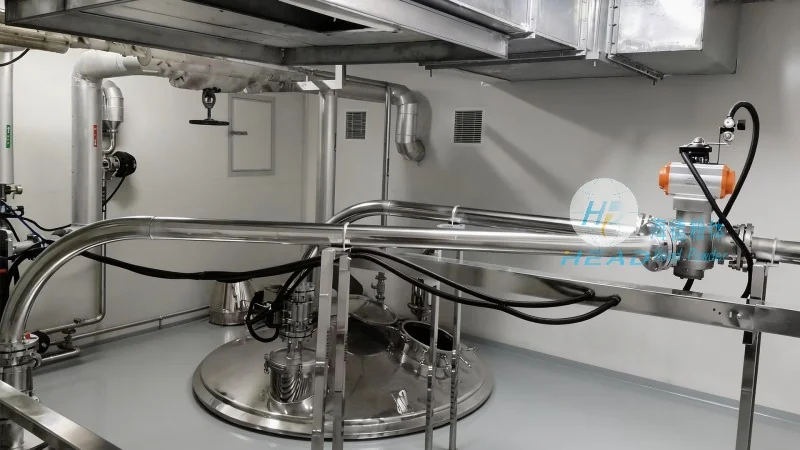
Fourth, pneumatic conveying systems are generally more energy-efficient compared to mechanical alternatives, especially over longer distances. The use of compressed air as the transport medium reduces the need for heavy machinery and maintenance, leading to lower operational costs in the long run. Additionally, the absence of moving parts in the pipeline itself minimizes wear and tear, extending the system's lifespan and reducing maintenance frequency.
Shandong HeadPowder Engineering Co., Ltd., a leading provider of engineering solutions for bulk material handling, specializes in designing and manufacturing customized pneumatic conveying systems tailored to the unique needs of clients. With years of experience in the industry, HeadPowder has developed a deep understanding of the challenges associated with handling delicate materials like pearl salt, and their solutions are engineered to address these challenges effectively.
HeadPowder's team of experts works closely with clients to assess their specific requirements, including the volume of material to be transported, the distance between source and destination, and any regulatory or quality standards that must be met. Based on this assessment, they design a system that incorporates the most suitable components, such as high-efficiency blowers, durable pipeline materials, and advanced control systems. The company's commitment to quality is evident in their use of premium materials and rigorous testing protocols, ensuring that each system meets or exceeds industry standards.
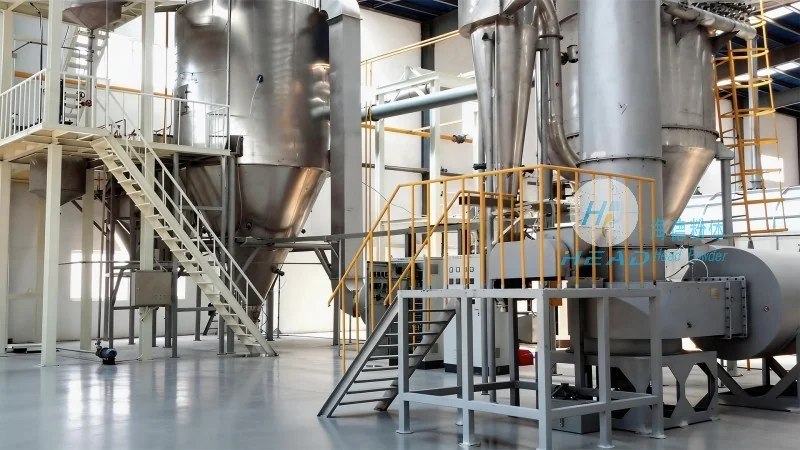
HeadPowder's pneumatic conveying systems are known for their reliability and durability, which are essential for continuous operation in industrial settings. The company's products are designed to withstand the rigors of daily use while maintaining optimal performance, reducing downtime and increasing overall productivity. Furthermore, HeadPowder provides comprehensive after-sales support, including maintenance services and technical assistance, to ensure that clients can maximize the lifespan and efficiency of their equipment.
By choosing HeadPowder Engineering, clients gain access to a partner who not only provides a high-quality pneumatic conveying system but also offers expert guidance and support throughout the entire process. Whether it's a new installation or an upgrade to an existing system, HeadPowder is dedicated to delivering solutions that enhance operational efficiency, improve product quality, and contribute to the long-term success of their clients' businesses.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top