When it comes to the efficient handling and transportation of bentonite powder, the selection of an appropriate pneumatic conveying system is crucial. This article provides an in-depth look at the classification and key components of bentonite powder pneumatic conveying systems, offering insights that can help businesses optimize their material handling processes.
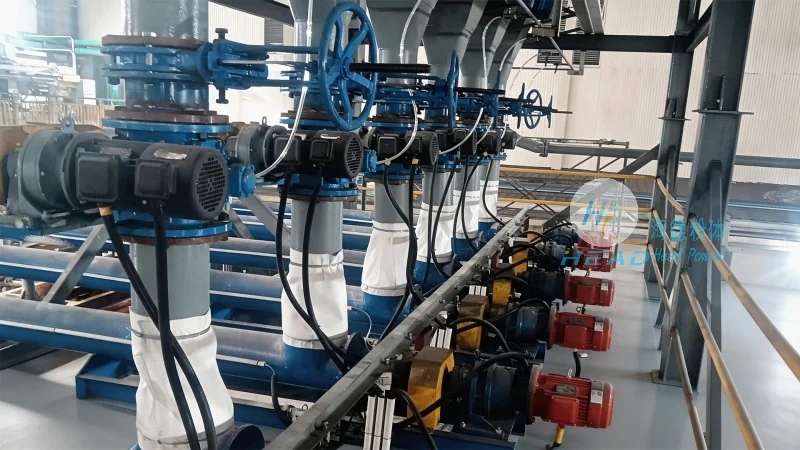
There are primarily two main categories of pneumatic conveying systems used for bentonite powder: positive pressure systems and negative pressure systems. Each type has distinct characteristics and is suitable for different operational requirements.
Positive pressure systems, also known as pressure conveying systems, operate by blowing air or gas into the conveying line under pressure. This method is effective for transporting materials over longer distances and through complex piping networks. The system typically includes a positive displacement blower or a rotary lobe pump that generates the necessary pressure to move the powder. Positive pressure systems are often preferred for applications where the material needs to be conveyed from a central storage to multiple destinations or where the process requires a high degree of control over the material flow.
Negative pressure systems, or vacuum conveying systems, work by creating a vacuum in the conveying line to draw the material from the source. This approach is commonly used for handling fine powders and is particularly suitable for applications that require gentle material handling to prevent product degradation or agglomeration. Negative pressure systems are ideal for short to medium distance conveying and for processes where the material is to be collected from various points and transported to a central collection point.
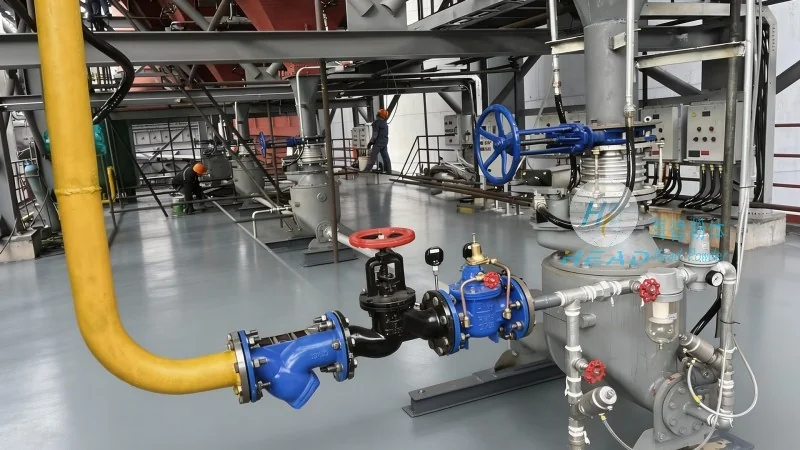
The effectiveness of a bentonite powder pneumatic conveying system depends on the integration of several critical components. Each component plays a vital role in ensuring the system operates efficiently and reliably.
Firstly, the feeding equipment is essential for introducing the bentonite powder into the conveying system. This may include hoppers, rotary valves, or screw feeders that can handle the bulk material and regulate the flow rate. Proper feeding equipment minimizes the risk of blockages and ensures a consistent feed to the conveyor.
Secondly, the conveying line is the main pathway for transporting the bentonite powder. The material is carried by the air stream within the pipeline, which can be made of stainless steel, plastic, or other materials depending on the properties of the powder and the operating conditions. The design of the conveying line, including the diameter and length, directly impacts the system's performance and efficiency.
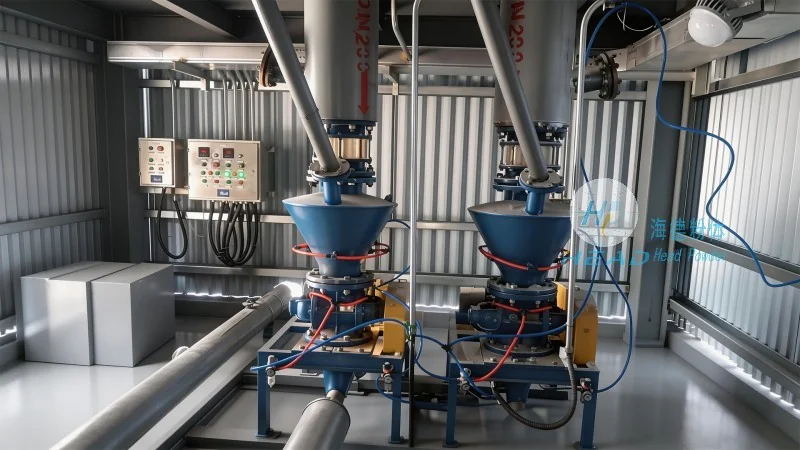
Thirdly, the air or gas source provides the necessary force to move the material. This can be a blower, a compressor, or a vacuum pump, depending on the system type. The air quality is also important, as contaminants can affect the performance and lifespan of the system components.
Fourthly, the separation and collection equipment is used to separate the bentonite powder from the air stream at the end of the conveying process. This typically involves cyclones, filters, or baghouses that capture the powder and return it to the process or storage. Proper separation is crucial to prevent dust emissions and maintain environmental compliance.
Finally, the control and monitoring systems help manage the operation of the pneumatic conveying system. These may include pressure sensors, flow meters, and control valves that allow operators to monitor and adjust the system parameters in real-time. Advanced control systems can also integrate with other process equipment to optimize the overall material handling workflow.
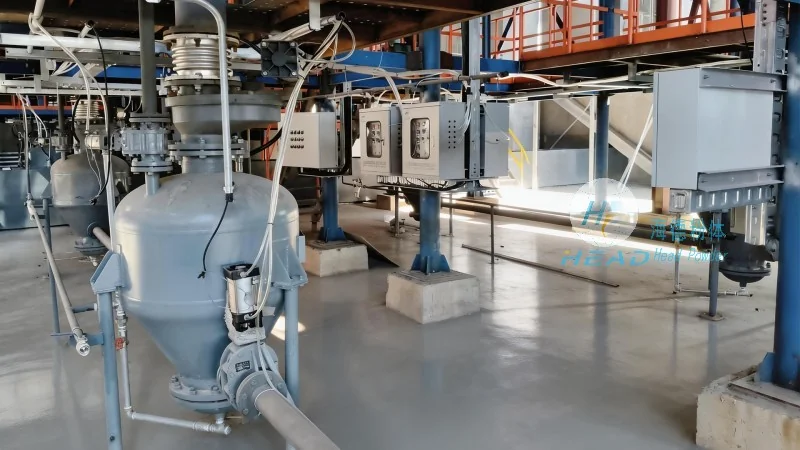
When selecting a bentonite powder pneumatic conveying system, several factors need to be considered to ensure optimal performance and cost-effectiveness. The characteristics of the bentonite powder, such as its particle size, moisture content, and flowability, are key determinants in choosing the appropriate system type and components.
For instance, if the bentonite powder is fine and prone to agglomeration, a negative pressure system with gentle handling features may be more suitable to prevent product degradation. Conversely, if the material needs to be transported over long distances with high throughput, a positive pressure system with robust feeding and conveying equipment may be the better choice.
Additionally, the operational environment and safety requirements should be taken into account. Pneumatic conveying systems must comply with local regulations regarding dust control and air quality. Proper maintenance and regular inspections are also essential to ensure the system operates efficiently and safely over its lifespan.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top