Red mud, a byproduct of bauxite processing in the aluminum industry, poses significant challenges for handling and disposal. Pneumatic conveying systems offer an efficient solution to transport this material over long distances with minimal environmental impact. This article provides an overview of the classification and key components of red mud pneumatic conveying systems, highlighting the technological advancements and practical applications in industrial settings.
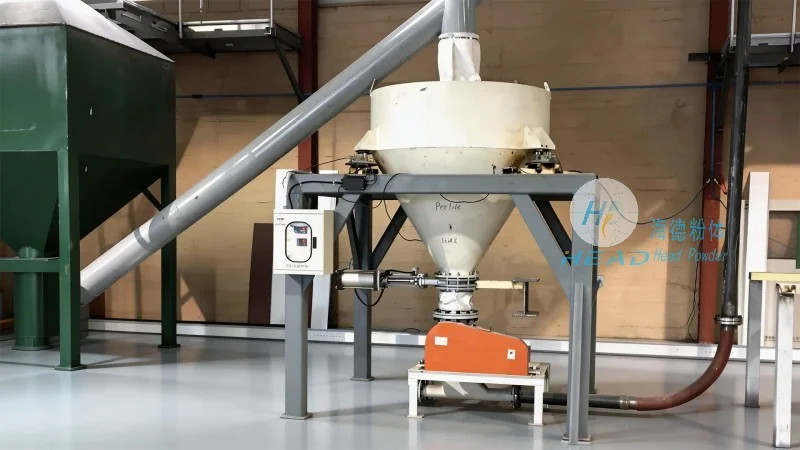
Red mud pneumatic conveying systems can be classified based on several key parameters, including the conveying medium, system pressure, and material characteristics. The primary classification includes positive pressure systems and negative pressure (vacuum) systems. Positive pressure systems utilize compressed air to push the material through the pipeline, while negative pressure systems use suction to draw the material from the source. Each type has distinct advantages and is selected based on the specific requirements of the application, such as the distance to be covered, the volume of material to be conveyed, and the need for dust control.
The core components of a red mud pneumatic conveying system are designed to ensure efficient and reliable operation. These components include the material feeder, which is responsible for introducing the red mud into the system at a controlled rate; the air compressor or vacuum pump, which provides the necessary pressure or suction; the conveying pipeline, which transports the material; and the separation and collection equipment, which removes the material from the air stream and returns it to the process or storage. Each component plays a critical role in maintaining the system's performance and preventing operational issues such as blockages or excessive wear.
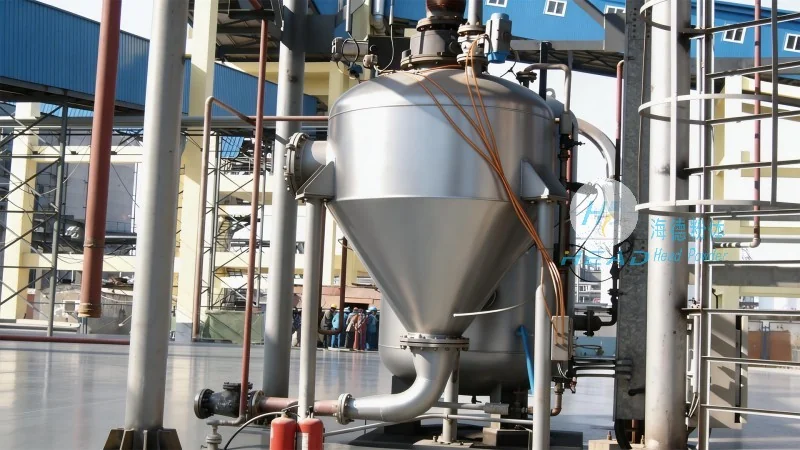
The material feeder is a critical component in red mud pneumatic conveying systems, as it directly influences the system's efficiency and reliability. For red mud, which is often a fine, abrasive material, specialized feeders are used to ensure consistent and controlled feeding. Common types include rotary valves, screw feeders, and vibratory feeders. These feeders are designed to handle the material's properties, such as its high moisture content and abrasive nature, while minimizing the risk of clogging or material degradation. The selection of the appropriate feeder depends on factors like the material's flowability, the required feeding rate, and the system's overall pressure requirements.
The air compressor or vacuum pump is the power source for the pneumatic conveying system, providing the necessary pressure or suction to move the red mud through the pipeline. Positive pressure systems typically use rotary screw or reciprocating air compressors, which can deliver high-pressure air to push the material. Negative pressure systems, on the other hand, rely on vacuum pumps, such as rotary vane or liquid ring pumps, to create a suction force that draws the material. The choice of compressor or pump is influenced by factors like the system's pressure requirements, the volume of material to be conveyed, and the need for energy efficiency. Modern systems often incorporate variable speed drives and advanced control systems to optimize energy consumption and maintain consistent performance.
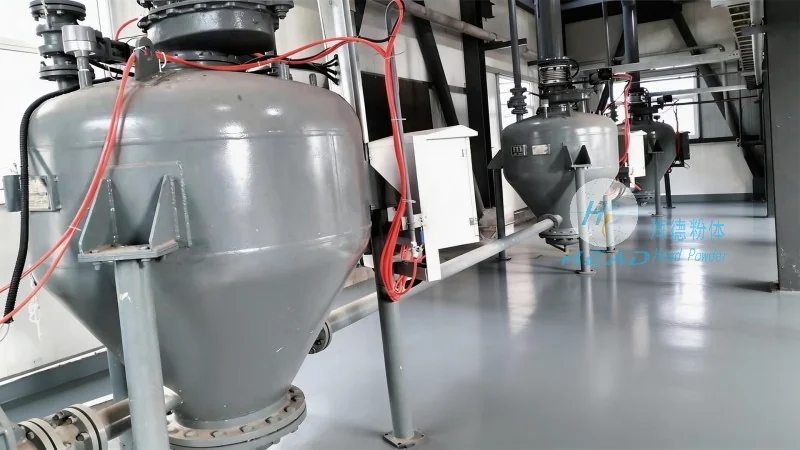
The conveying pipeline is a crucial part of the red mud pneumatic conveying system, responsible for transporting the material from the source to the destination. The pipeline is typically made of materials such as stainless steel or plastic, which are resistant to corrosion and abrasion caused by the red mud. The design of the pipeline, including the diameter, length, and layout, is critical to ensuring efficient material transport. Factors such as the material's density, flowability, and the required conveying velocity are considered during the design process. The pipeline may also include components like bends, elbows, and expansion joints to accommodate changes in direction and accommodate thermal expansion. Proper pipeline design and maintenance are essential to prevent blockages, reduce pressure losses, and ensure the longevity of the system.
At the receiving end of the pneumatic conveying system, separation and collection equipment is used to remove the red mud from the air stream and return it to the process or storage. This equipment typically includes cyclone separators, bag filters, or electrostatic precipitators, depending on the system's requirements. Cyclone separators use centrifugal force to separate the material from the air, while bag filters or electrostatic precipitators use filtration or electrostatic attraction to capture fine particles. The choice of separation equipment is influenced by factors like the material's particle size distribution, the required dust removal efficiency, and the system's overall capacity. Proper maintenance of the separation equipment is essential to ensure effective material recovery and prevent air pollution.
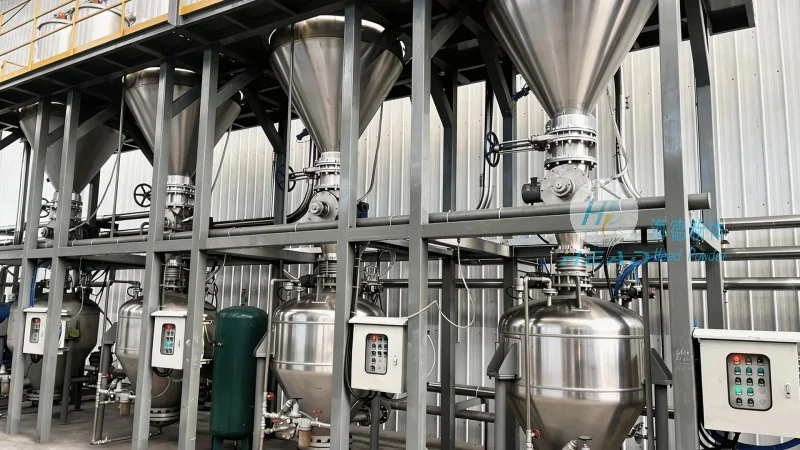
Red mud pneumatic conveying systems are widely used in the aluminum industry for transporting red mud from the digestion process to storage facilities or for further processing. For example, in a large aluminum smelter, a positive pressure system may be used to convey red mud over a distance of several kilometers to a dedicated storage area. The system is designed to handle high volumes of material while maintaining low pressure losses and minimal environmental impact. Another application is in the transportation of red mud to a disposal site, where a negative pressure system may be used to collect the material from a collection hopper and transport it to the site. These applications demonstrate the versatility and effectiveness of pneumatic conveying systems in handling red mud, which is often a challenging material to transport due to its abrasive and corrosive properties.
In conclusion, red mud pneumatic conveying systems are an essential technology for the efficient and environmentally friendly handling of red mud in the aluminum industry. The classification and key components of these systems, including the material feeder, air compressor, conveying pipeline, and separation equipment, are critical to their performance and reliability. As technology advances, there is a growing focus on improving energy efficiency, reducing maintenance costs, and enhancing the overall sustainability of these systems. Future developments may include the integration of advanced control systems, the use of more durable materials, and the adoption of green technologies to minimize the environmental impact of red mud handling. Companies like Shandong HeadPowder Engineering Co., Ltd., based in China, are at the forefront of developing and implementing these advanced systems, providing customized solutions to meet the specific needs of industrial clients.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top