HeadPowder, a leading enterprise in the field of pneumatic conveying technology, specializes in the design, manufacturing, and installation of cement powder pneumatic conveying systems. This article provides an in-depth overview of the classification and essential components of such systems, highlighting the technical aspects and practical applications that define their performance and reliability.
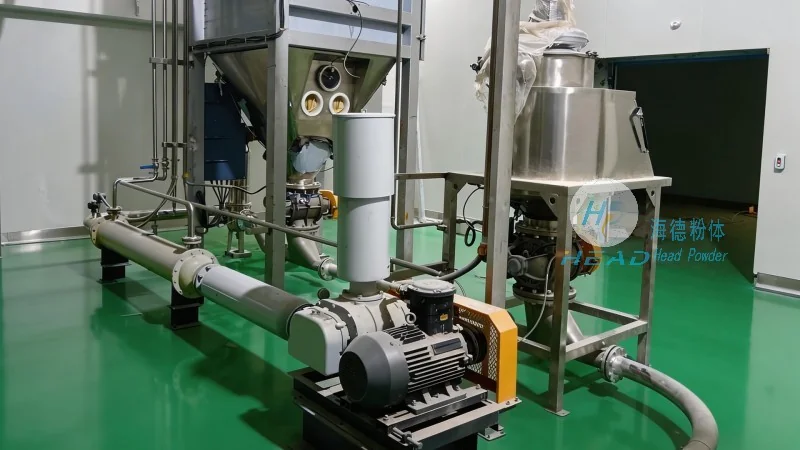
Cement powder pneumatic conveying systems are critical in industrial applications for transporting bulk materials like cement, powders, and granules over long distances with high efficiency and minimal loss. These systems utilize air or other gases to move material through a pipeline network, offering advantages such as reduced labor costs, improved safety, and enhanced process control compared to traditional mechanical conveying methods. The design and selection of the right system depend on various factors including material properties, distance, and operational requirements.
Based on the principle of air flow and material transport, cement powder pneumatic conveying systems are broadly classified into two main categories: dilute-phase and dense-phase systems. Each type has distinct characteristics and is suitable for different operational scenarios.
Dilute-phase systems operate by transporting material in a suspended state within the conveying air. The material is carried in a relatively low concentration, typically with a material-to-air ratio of less than 0.1. This method is ideal for short to medium distances and materials with good flow characteristics. The primary components of a dilute-phase system include a blower or compressor to generate the air flow, a hopper or feeder to feed the material, a pipeline network, and a receiver or silo to collect the material at the destination. The system's efficiency and performance are influenced by factors such as air velocity, material particle size, and the system's pressure drop.
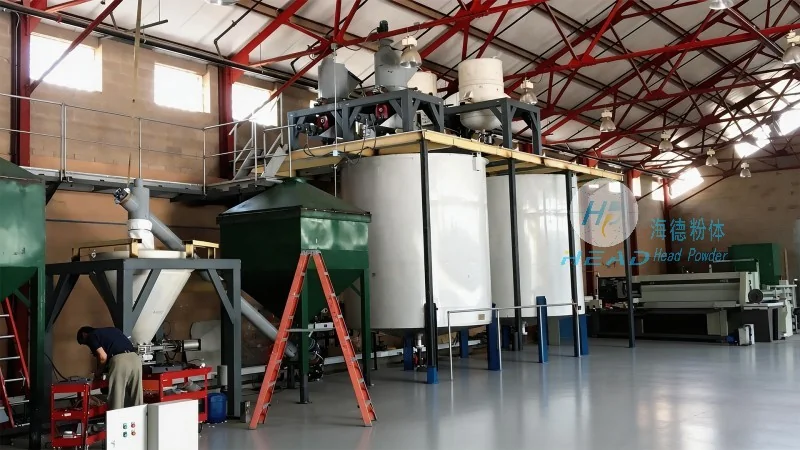
Dense-phase systems, also known as low-pressure or high-density systems, transport material in a more concentrated state, with a material-to-air ratio typically ranging from 0.1 to 0.5. This method is suitable for longer distances and materials that are prone to bridging or caking. Dense-phase systems often use a positive displacement blower or a rotary lobe pump to provide a more consistent and higher pressure flow, ensuring reliable material transport. The key components include a feeder, a pipeline with appropriate diameter and length, and a receiver. The system's design focuses on maintaining a stable flow and preventing material degradation or degradation during transport.
Regardless of the system type, several essential components are integral to the operation of cement powder pneumatic conveying systems. These components work in harmony to ensure efficient and reliable material transport.
The feeding and hopper system is the initial stage of the conveying process, responsible for storing and delivering the cement powder to the conveying line. The hopper is typically designed with a conical or rectangular shape to facilitate material flow and prevent bridging or arching. The feeder, often a rotary valve or a screw feeder, controls the material discharge rate, ensuring a consistent flow into the pipeline. Proper design of the hopper and feeder is crucial to maintain system efficiency and prevent material blockages.
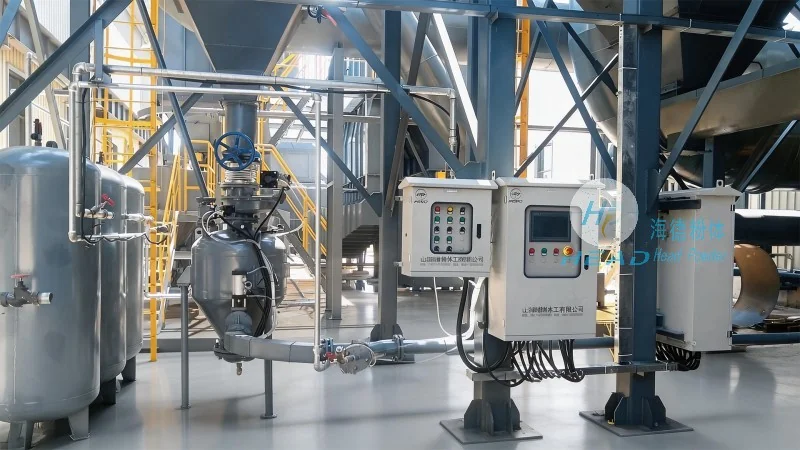
The air-flow generation component, such as a blower or compressor, is responsible for creating the necessary pressure and airflow to move the material. The choice of equipment depends on the system type and operational requirements. In dilute-phase systems, a centrifugal blower is commonly used due to its ability to handle large volumes of air at relatively low pressure. In dense-phase systems, a positive displacement blower or a rotary lobe pump is preferred to provide higher pressure and more consistent flow. The system also includes pressure regulators and valves to control the air pressure and flow rate, ensuring optimal performance and preventing overpressurization or underpressurization.
The pipeline network is the core of the conveying system, consisting of pipes, elbows, tees, and other fittings that guide the material and air from the source to the destination. The pipe material is typically selected based on the material being conveyed and the system's operating conditions. Common materials include stainless steel, carbon steel, or plastic, with stainless steel being preferred for its corrosion resistance and durability in handling cement powder. The pipeline design considers factors such as pressure drop, material velocity, and the need for cleaning and maintenance. Proper sizing of the pipeline is critical to ensure efficient transport and minimize energy consumption.
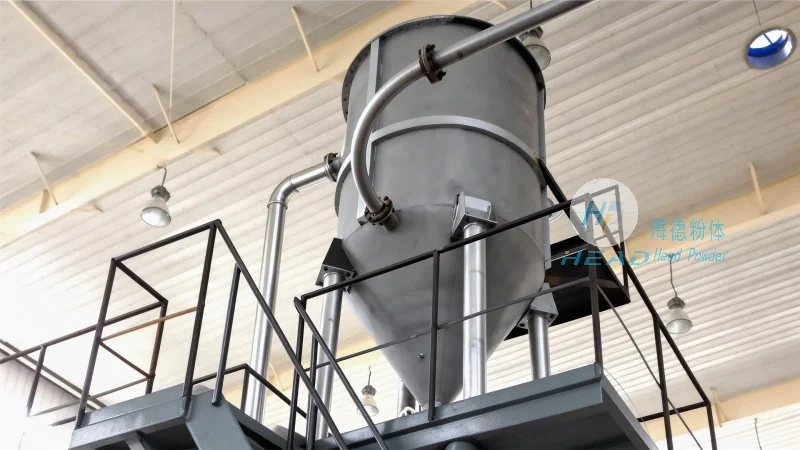
The receiver or silo system is the final stage of the conveying process, responsible for collecting the material at the destination. The receiver is designed to accommodate the material and may include a hopper or a bin to store the material until it is used. The system may also include a discharge valve or a rotary valve to control the material release. The receiver's design ensures that the material is collected without spillage or contamination, and it may include features such as level indicators and pressure relief valves for safety and operational monitoring.
The performance and longevity of cement powder pneumatic conveying systems depend on proper operation and regular maintenance. Key operational considerations include monitoring air pressure and flow rates, checking for blockages or leaks in the pipeline, and ensuring the feeder and hopper are functioning correctly. Regular maintenance activities include cleaning the system, inspecting components for wear and tear, and replacing worn parts as needed. Proper maintenance helps to prevent system downtime, reduce energy consumption, and extend the system's service life.
HeadPowder Engineering Co., Ltd., with its headquarters in Shandong, China, is a trusted provider of cement powder pneumatic conveying systems. The company's expertise in system design, manufacturing, and installation ensures that clients receive reliable and efficient solutions tailored to their specific needs. By understanding the classification and components of these systems, industrial operators can make informed decisions to enhance their material handling processes and improve overall operational efficiency.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top