Calcite, a widely used mineral in industrial applications, often requires efficient and reliable material handling methods for its transportation. Pneumatic conveying systems offer a viable solution to move calcite powder or granules from one location to another without the need for mechanical components like conveyors or elevators. For industries dealing with calcite, selecting the right pneumatic conveying system is crucial to ensure operational efficiency, product integrity, and cost-effectiveness. This article explores several effective approaches to calcite pneumatic conveying, highlighting the key considerations and solutions provided by Shandong HeadPowder Engineering Co., Ltd. (hereinafter referred to as HeadPowder).
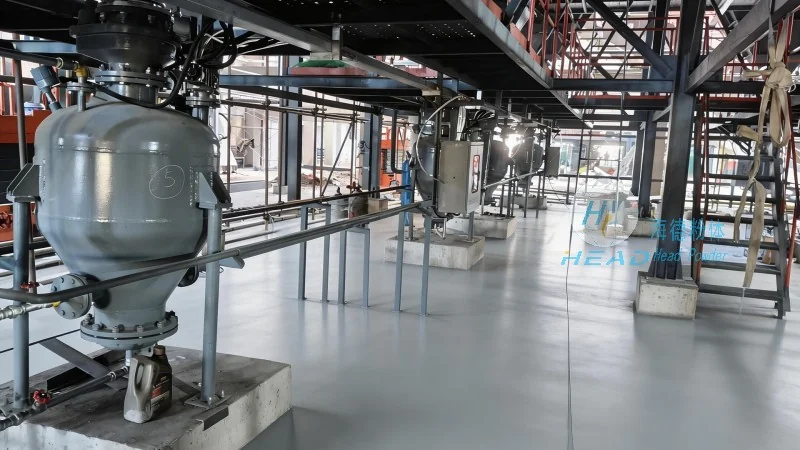
Pneumatic conveying uses compressed air or vacuum to transport bulk materials like calcite through a pipeline. The process involves creating a flow of air that carries the material particles, allowing for seamless movement between storage, processing, and packaging areas. For calcite, which is often used in applications such as cement production, glass manufacturing, and chemical processing, the choice of conveying system depends on factors like material characteristics, distance, and environmental requirements. HeadPowder specializes in designing and implementing customized pneumatic conveying solutions tailored to the specific needs of calcite handling operations.
Positive pressure pneumatic conveying systems operate by blowing air into the conveying line, creating a positive pressure that pushes the calcite material forward. This method is suitable for short to medium distances and is effective for transporting calcite from silos or storage bins to processing equipment. The system typically includes a blower, a hopper with a feeder, and a pipeline network. HeadPowder’s positive pressure solutions are designed to handle calcite with high efficiency, ensuring minimal product degradation and consistent flow rates. The company’s expertise in material flow dynamics allows for the optimization of blower capacity and pipeline design to maximize conveying performance.
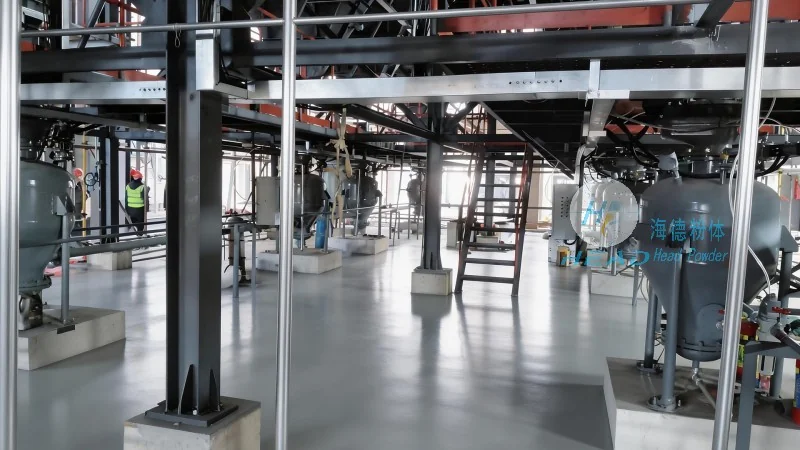
Negative pressure systems, also known as vacuum conveying, draw air and calcite material into the conveying line using a vacuum pump. This approach is ideal for long-distance transport or when the calcite needs to be collected from multiple sources. The vacuum system can handle calcite from various locations, such as raw material storage areas or production lines, and transport it to a central processing unit. HeadPowder’s vacuum conveying solutions are engineered to maintain a consistent vacuum level, ensuring that calcite particles are efficiently drawn into the pipeline without clogging or degradation. The system is particularly useful for handling calcite that may be sensitive to pressure changes or for applications requiring gentle handling.
Mixed-pressure or hybrid systems combine elements of both positive and negative pressure methods. These systems use a combination of blowers and vacuum pumps to create a balanced pressure environment, allowing for flexible conveying of calcite over varying distances and conditions. HeadPowder offers hybrid solutions that can adapt to different operational scenarios, such as transporting calcite from a storage silo to a processing plant over a long distance while maintaining efficiency. The mixed-pressure approach is beneficial when the calcite handling process involves multiple stages, requiring both pressure and vacuum phases to optimize material flow.
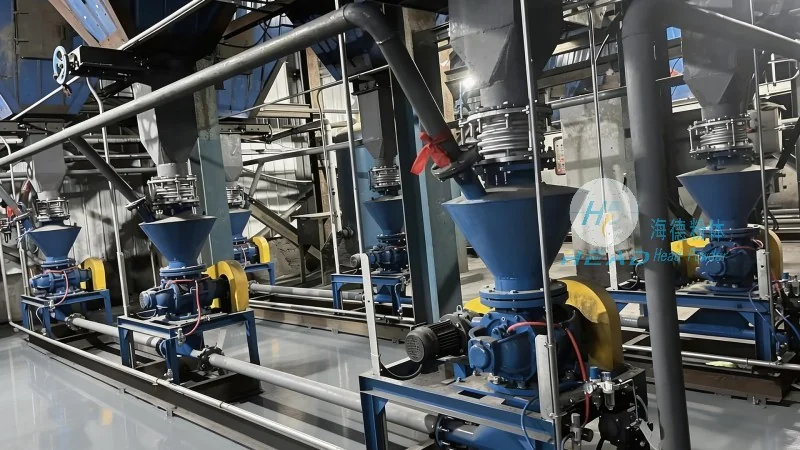
When selecting a pneumatic conveying system for calcite, several factors must be considered to ensure optimal performance. First, the physical properties of calcite, such as particle size, density, and moisture content, influence the choice of system. Larger or denser particles may require higher air velocities or different pipeline diameters. Second, the distance and layout of the conveying route affect the system design. Longer distances may necessitate multiple stages or booster units to maintain pressure. Third, environmental factors, including dust control and air quality, are critical, especially in applications where calcite is used in food or pharmaceutical industries. HeadPowder addresses these considerations by conducting thorough material analysis and site assessments before designing a custom solution. The company’s engineers work closely with clients to understand their specific calcite handling challenges and provide tailored recommendations.
HeadPowder Engineering Co., Ltd., based in Shandong, China, is a leading provider of pneumatic conveying solutions for calcite and other bulk materials. With years of experience in the industry, HeadPowder offers comprehensive services, including system design, installation, and maintenance. The company’s expertise in material handling technology ensures that calcite is transported safely and efficiently, minimizing downtime and operational costs. HeadPowder’s solutions are designed to meet international standards for safety and environmental compliance, making them suitable for a wide range of industrial applications. By leveraging advanced engineering and customer-focused approaches, HeadPowder helps industries optimize their calcite handling processes, enhancing productivity and reducing waste.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top