HeadPowder, a leading engineering company based in Shandong, China, specializes in the design and implementation of coke pneumatic conveying systems. These systems are crucial for efficient material handling in various industrial applications, particularly in the steel and metallurgical sectors. Understanding the classification and composition of such systems is essential for optimizing operational efficiency and ensuring reliable performance.
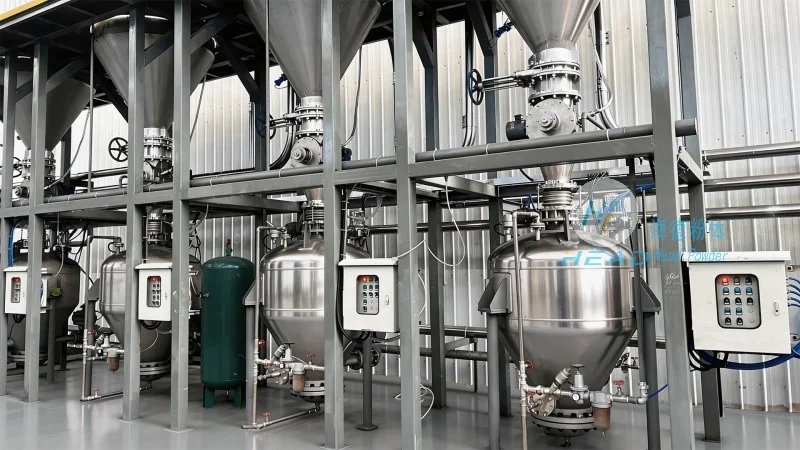
Coke pneumatic conveying systems can be broadly classified based on the principles of air flow and material transport mechanisms. The primary categories include dilute-phase and dense-phase systems, each tailored to specific operational requirements and material characteristics. Dilute-phase systems utilize low-pressure air to suspend and transport materials, making them suitable for long-distance and high-volume applications. In contrast, dense-phase systems employ higher pressure and lower air-to-material ratios to move materials more slowly and with greater control, which is beneficial for handling delicate or abrasive materials like coke.
A coke pneumatic conveying system consists of several critical components that work in tandem to ensure effective material transport. The main components include a material feed hopper, a rotary valve or feeder for controlled material discharge, a conveying pipeline, a dust collector or filter system to manage air and particulate emissions, and a receiver or discharge hopper at the destination. The material feed hopper is designed to store and regulate the flow of coke, preventing blockages and ensuring a consistent feed rate. The rotary valve or feeder acts as a gate to control the amount of material entering the pipeline, preventing overloading and maintaining system stability. The conveying pipeline is typically made of corrosion-resistant materials like stainless steel or special alloys to withstand the abrasive nature of coke and the effects of air pressure. The dust collector or filter system is essential for maintaining air quality and complying with environmental regulations, as coke dust can be a health hazard if not properly managed. Finally, the receiver or discharge hopper collects the material at the end of the pipeline, allowing for smooth unloading and integration with downstream processes.
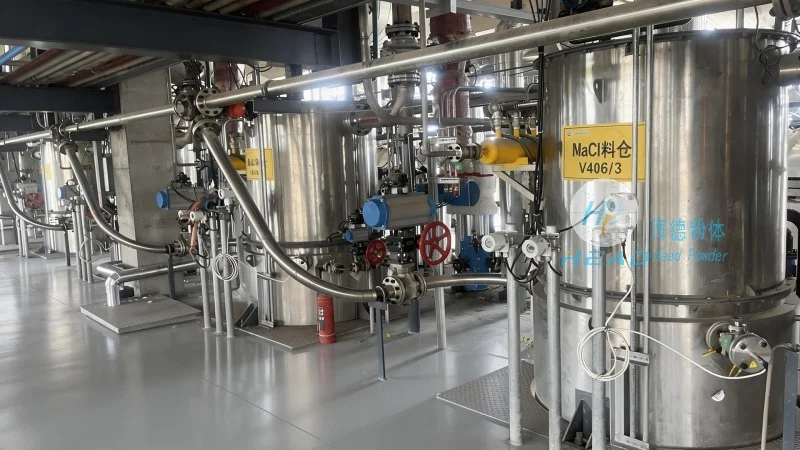
Designing an effective coke pneumatic conveying system requires careful consideration of several factors to ensure optimal performance and longevity. One of the most critical considerations is the selection of the appropriate conveying method based on the specific application and material properties. For example, dilute-phase systems are often preferred for long-distance transport of large quantities of coke, while dense-phase systems may be more suitable for short-distance transport of finer coke particles. Another key factor is the sizing of the system components, including the pipeline diameter, air velocity, and pressure levels. Proper sizing ensures that the system operates within its design parameters, minimizing energy consumption and wear on components. Additionally, the integration of a dust control system is vital to maintain air quality and prevent environmental contamination. This may involve the use of bag filters, cartridge filters, or other filtration technologies to capture coke particulates before releasing air back into the environment. Finally, regular maintenance and monitoring of the system are essential to detect and address issues such as blockages, wear, or leaks promptly, ensuring continuous and reliable operation.
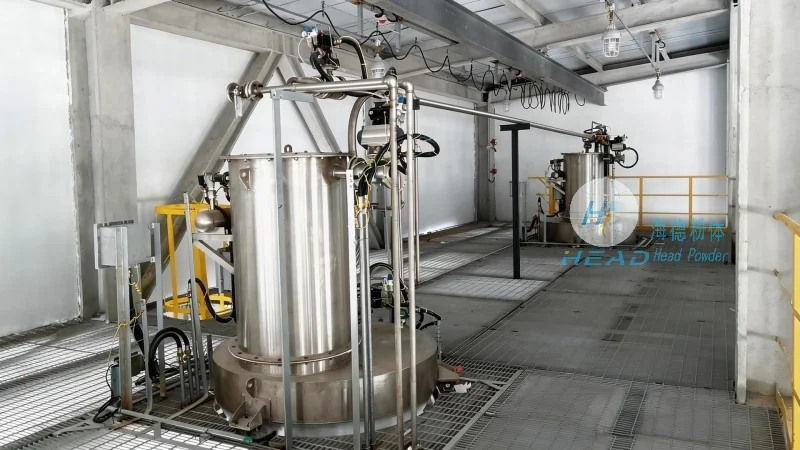
Coke pneumatic conveying systems are widely used in various industrial applications, particularly in the steel industry where coke is a key raw material for blast furnaces. These systems are also utilized in other metallurgical processes, such as the transport of coke from storage facilities to processing plants or from production lines to storage areas. The primary benefits of using coke pneumatic conveying systems include improved operational efficiency, reduced labor costs, and enhanced safety compared to traditional manual or mechanical handling methods. By automating the material transport process, these systems minimize the risk of accidents and injuries associated with manual handling of heavy or abrasive materials. Additionally, the use of pneumatic conveying systems can reduce material loss and improve product quality by minimizing exposure to external contaminants. Furthermore, the systems can be easily integrated with other industrial equipment, such as conveyor belts or storage silos, to create a seamless material handling workflow. Overall, coke pneumatic conveying systems offer a reliable and efficient solution for the transport of coke in industrial settings.
In conclusion, coke pneumatic conveying systems are a vital component of modern industrial material handling, offering efficient and reliable transport of coke in various applications. The classification of these systems into dilute-phase and dense-phase categories allows for tailored solutions based on specific operational needs. The key components, including feed hoppers, rotary valves, conveying pipelines, dust collectors, and receivers, work together to ensure smooth and controlled material transport. Proper system design, considering factors such as material properties, distance, and environmental regulations, is essential for optimal performance. The benefits of using coke pneumatic conveying systems, including improved efficiency, safety, and product quality, make them a preferred choice in the steel and metallurgical industries. As a leading engineering company, HeadPowder provides expert design and implementation services to ensure that coke pneumatic conveying systems meet the specific requirements of its clients, contributing to their operational success and sustainability.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top