Activated carbon pneumatic conveying systems are specialized equipment used for the efficient transport of activated carbon, a critical material in various industrial applications such as air purification, water treatment, and chemical processing. These systems leverage pneumatic technology to move activated carbon from storage to processing units, ensuring minimal dust generation and optimal material handling. Understanding the classification and composition of these systems is essential for selecting the right equipment for specific industrial needs.
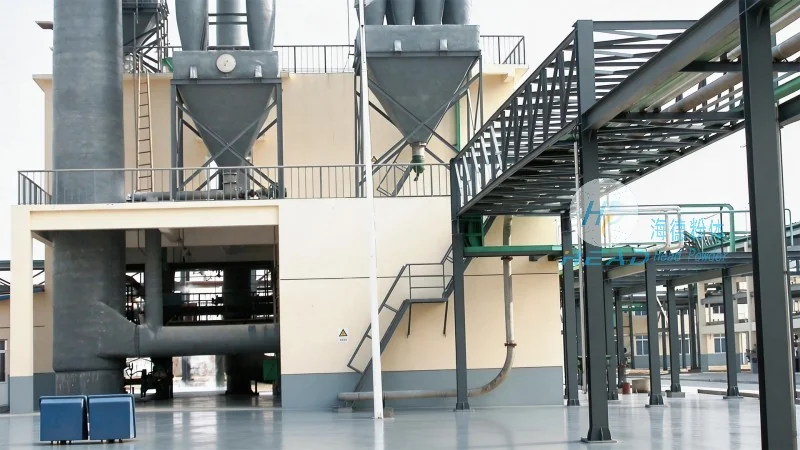
Activated carbon pneumatic conveying systems can be classified based on several key factors, including the type of conveying medium, the system pressure, and the application requirements. The primary classifications include pressure systems, vacuum systems, and pressure-vacuum hybrid systems. Pressure systems use compressed air or gas to push the material through the pipeline, while vacuum systems use suction to draw the material. Hybrid systems combine both approaches to offer flexibility in different operational scenarios. Each classification has distinct advantages and is suited to different operational environments and material characteristics.
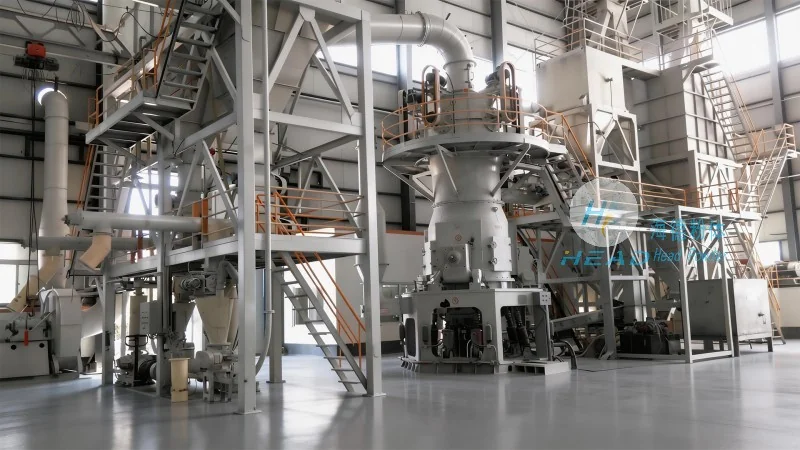
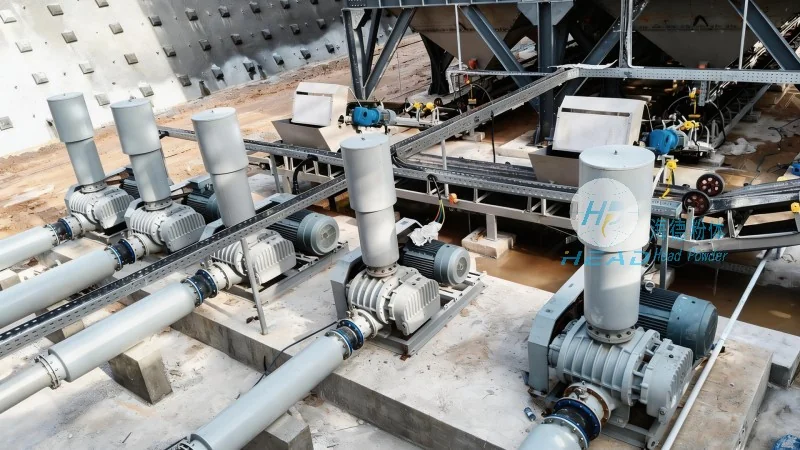
The composition of an activated carbon pneumatic conveying system involves several critical components that work in tandem to ensure efficient material transport. The main components include the hopper or storage bin, the feeder, the conveying pipeline, the air compressor or vacuum pump, the control system, and the dust collection or filtration unit. The hopper is responsible for storing the activated carbon, providing a consistent feed to the feeder. The feeder, often a rotary valve or screw feeder, controls the flow rate of the material into the pipeline. The conveying pipeline, typically made of stainless steel or other corrosion-resistant materials, transports the material and air mixture. The air compressor or vacuum pump generates the necessary pressure or vacuum to move the material. The control system monitors and regulates the operation of the feeder, compressor, and other components to maintain optimal performance. Finally, the dust collection or filtration unit ensures that any airborne particles are captured, preventing contamination and maintaining air quality.
Shandong HeadPowder Engineering Co., Ltd. specializes in the design, manufacturing, and installation of high-quality activated carbon pneumatic conveying systems. With years of experience in the industry, HeadPowder has developed a comprehensive range of solutions tailored to meet the diverse needs of clients across various sectors. The company's team of engineers and technicians leverages advanced technology and rigorous quality control processes to ensure that each system meets the highest standards of performance and reliability. HeadPowder's commitment to innovation and customer satisfaction has made it a trusted partner for businesses seeking efficient and effective activated carbon handling solutions. The company's headquarters is located in Shandong, China, where it operates a state-of-the-art manufacturing facility and research center.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top