Compound fertilizer pneumatic conveying systems are critical in modern agricultural and industrial settings, designed to efficiently transport bulk materials while maintaining product integrity and operational safety. These systems are engineered to handle the unique characteristics of compound fertilizers, ensuring reliable material transfer across various applications. Understanding the classification and composition of such systems is essential for selecting the appropriate equipment and optimizing operational performance.
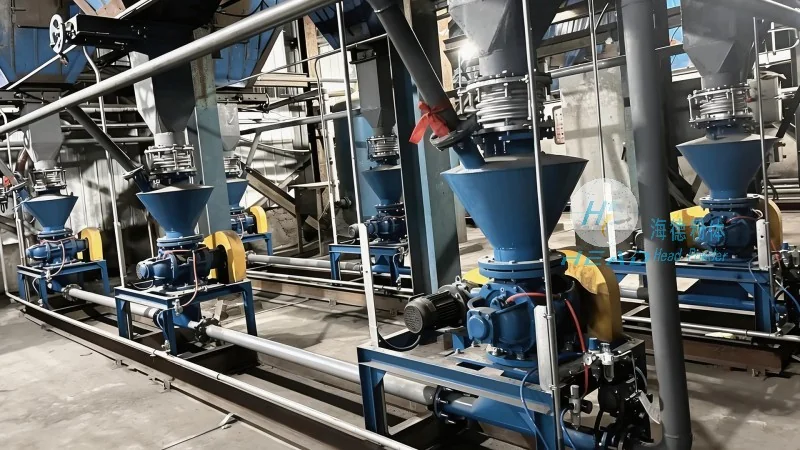
Compound fertilizer pneumatic conveying systems are primarily classified based on the pressure differential within the system, with two main categories: positive pressure systems and negative pressure systems. Each classification has distinct operational principles and is suited to different material handling scenarios.
Positive pressure systems operate by blowing air or gas into the conveying line, creating a pressure higher than ambient air pressure. This method is ideal for transporting dry, free-flowing materials like compound fertilizers, as it provides consistent and reliable material movement. The system typically includes a blower or compressor at the discharge end, which generates the necessary pressure to move the material. A key advantage is the ability to handle long conveying distances and multiple transfer points without significant pressure loss. The components generally consist of a feed hopper to store and feed material, a rotary valve to control flow rate, a rigid or flexible pipe network for transport, and a separator at the receiving end to clean the product. The blower ensures the material is propelled through the system, while the separator uses centrifugal force or filtration to separate the fertilizer from the air stream, delivering a clean product to the storage or processing area.
Negative pressure systems, also known as suction systems, create a vacuum in the conveying line to draw material from the source. This approach is particularly effective for applications requiring material collection from multiple points or for handling dusty or fine materials. The system includes a vacuum pump or fan at the inlet, which generates the suction force. The feed hopper and rotary valve regulate material flow into the suction line, while the pipe network transports the material to the collection point. At the receiving end, a cyclone or filter separates the material from the air, preventing dust dispersion and ensuring product purity. Negative pressure systems are often preferred for their ability to handle sensitive materials without exposing them to high pressure, making them suitable for environments where dust control is critical.
Regardless of classification, a compound fertilizer pneumatic conveying system comprises several essential components that work in tandem to ensure efficient operation. These include the feed hopper, material feeder, conveying line, air source equipment, and separation equipment. Each component plays a vital role in maintaining system performance and reliability.
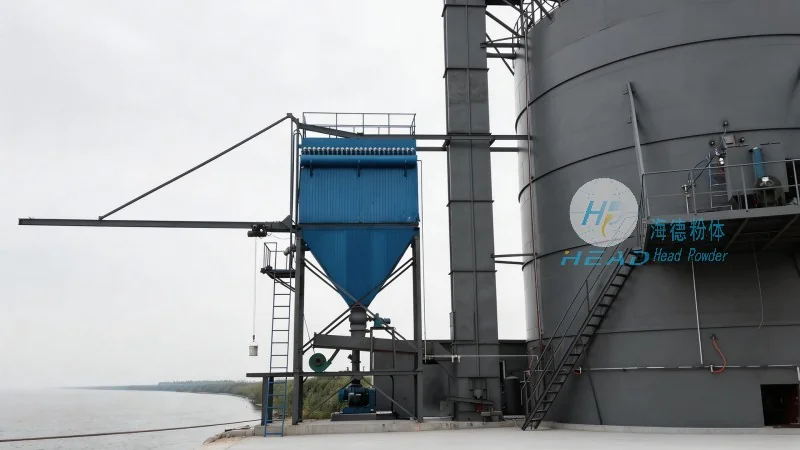
The feed hopper serves as a storage container for the compound fertilizer, providing a consistent material supply to the system. It is designed to prevent material bridging and ensure smooth flow into the feeder. The material feeder, commonly a rotary valve or screw conveyor, regulates the flow rate of fertilizer into the conveying line. This component is critical to avoid overloading the system and to maintain a steady material velocity, which minimizes pressure drop and prevents blockages. The feeder ensures the material is introduced into the air stream at a controlled rate, optimizing system efficiency and preventing material degradation.
The conveying line is the primary component responsible for transporting the material from the source to the destination. It can be constructed from rigid metal pipes (e.g., stainless steel, PVC) or flexible hoses, depending on the system design and operational requirements. The choice of pipe material depends on the chemical properties of the fertilizer and the need for corrosion resistance. The line is equipped with elbows, tees, and other fittings to direct the material flow and accommodate changes in direction or elevation. The diameter of the pipe is carefully selected to ensure the material can be conveyed at the desired velocity without causing excessive pressure loss or material degradation. Proper pipe sizing and material selection are crucial for maintaining system efficiency and longevity.
The air source equipment provides the necessary air or gas to drive the conveying system. In positive pressure systems, a high-pressure blower or compressor is used, while negative pressure systems employ a vacuum pump or fan. The air source must deliver the required volume and pressure to move the material efficiently. The selection depends on system classification, conveying distance, and material characteristics. For example, a high-capacity blower is suitable for long-distance positive pressure conveying, whereas a low-pressure vacuum pump is ideal for short-distance negative pressure applications. The air source is typically equipped with filters to remove contaminants, ensuring the material remains clean and free of dust or debris that could affect product quality or system performance.
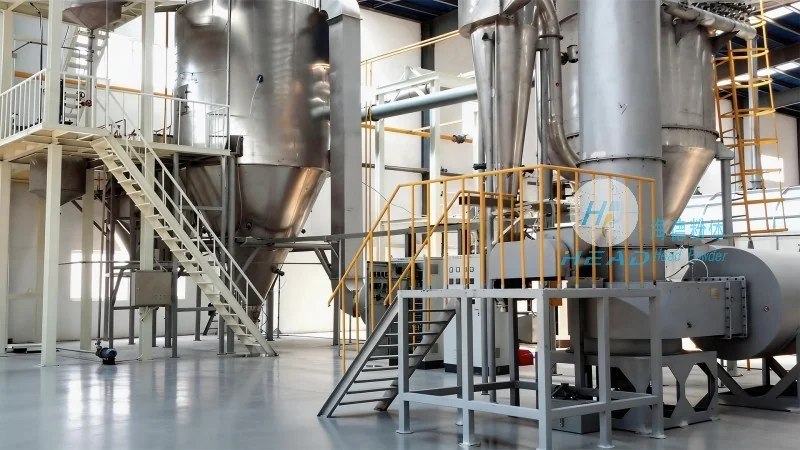
The separation and collection equipment is used at the receiving end to separate the material from the air stream. This component is essential to prevent dust dispersion and to ensure the product is free of contaminants. Common separation devices include cyclones, filters, or baghouses. A cyclone separator uses centrifugal force to separate material from air, while a filter or baghouse traps particles in a mesh or fabric. The separated material is collected in a receiving hopper or bin, ready for further processing or storage. The clean air, now free of dust, is either vented to the atmosphere or recirculated back into the system, depending on environmental regulations and operational needs. This equipment ensures that the final product meets quality standards and that the system operates within safe and regulatory parameters.
Modern compound fertilizer pneumatic conveying systems often integrate advanced control systems to monitor and regulate operation. These systems use sensors and controllers to maintain flow rate, pressure, and temperature within optimal ranges. The control panel provides real-time data and alerts operators to any abnormalities, such as blockages or pressure drops, allowing for immediate adjustments to prevent system damage or inefficiency. The integration of automation enhances reliability, reduces downtime, and lowers maintenance costs. Control systems can also optimize energy usage by adjusting air volume or pressure based on material load, contributing to overall operational efficiency. This level of control is particularly valuable in large-scale fertilizer plants where consistent performance is critical.
Compound fertilizer pneumatic conveying systems are widely used in industries such as agriculture, manufacturing, and logistics. They are essential in fertilizer production plants, storage facilities, and distribution centers where bulk material handling is required. The benefits of using pneumatic conveying systems include increased operational efficiency, reduced labor costs, and improved safety. By automating material transfer, these systems minimize manual handling, reducing the risk of accidents and exposure to dust or chemicals. Additionally, they can handle a wide range of material types and sizes, making them versatile for various operational needs. The systems also contribute to environmental sustainability by reducing material waste and controlling dust emissions, aligning with modern industrial and environmental standards.
Compound fertilizer pneumatic conveying systems represent sophisticated and efficient solutions for bulk material transport. The classification and composition of these systems are tailored to meet specific operational requirements, ensuring reliable and safe material transfer. By understanding the components and operational principles, users can select the appropriate equipment to optimize performance and meet industry standards. The integration of advanced control technology and materials handling expertise continues to enhance system efficiency and reliability, making them indispensable in modern industrial operations. As the demand for efficient and sustainable material handling grows, the importance of well-designed pneumatic conveying systems will only increase, ensuring compound fertilizers are transported safely and effectively to support agricultural and industrial sectors worldwide.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top