Sintered dust removal material conveying systems are critical in industrial processes, especially within the iron and steel industry where sintering operations produce substantial dust and fine particulate matter. These systems are engineered to efficiently collect, transport, and manage sintered dust, ensuring environmental compliance and optimizing material recovery. The following sections will detail the working principle and key features of such systems, offering a comprehensive overview of their functionality and benefits.
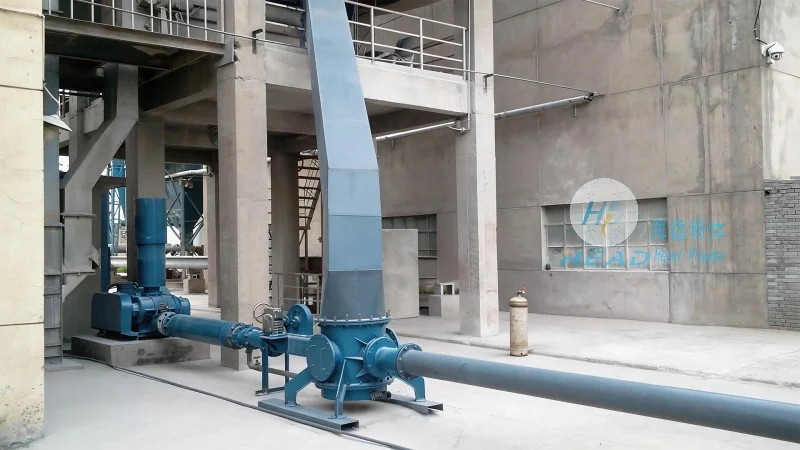
The operation of a sintered dust removal material conveying system involves several integrated steps to ensure effective material handling. Initially, sintered dust is collected from sources like the sintering machine, cooling bed, or dust hoppers. This collected dust is then transferred to a storage or processing area via conveying equipment. Common systems include belt conveyors, screw conveyors, and pneumatic (air-assisted) conveyors, selected based on material properties and plant layout.
Belt conveyors are widely used for horizontal or slight incline transport due to high load capacity and bulk material handling. They consist of a continuous loop of flat or troughed belts moving over rollers, transporting dust from collection to processing/storage. Screw conveyors utilize a rotating screw within a tube, suitable for vertical or inclined transport in confined spaces. Pneumatic conveyors employ compressed air to create an air-dust flow, enabling long-distance and vertical lift transport with minimal friction.
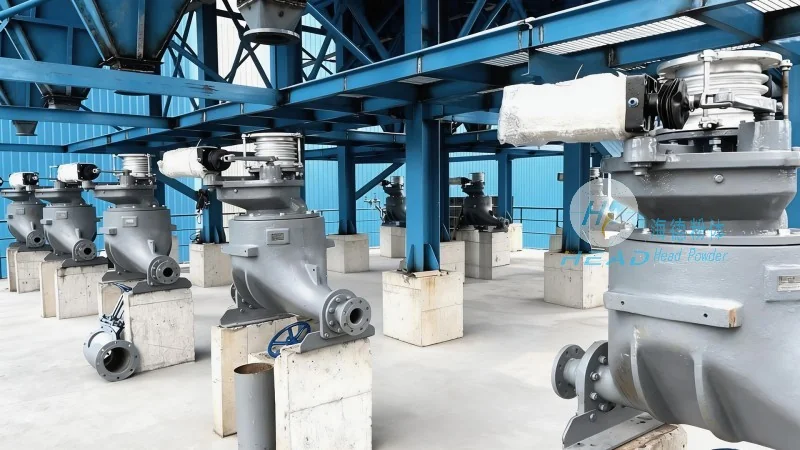
After conveyance, material may undergo additional processing (drying, screening, magnetic separation) to improve quality. Integrated dust collection and filtration components (cyclone separators, bag filters, electrostatic precipitators) capture fine particles, minimizing air emissions and protecting the environment.
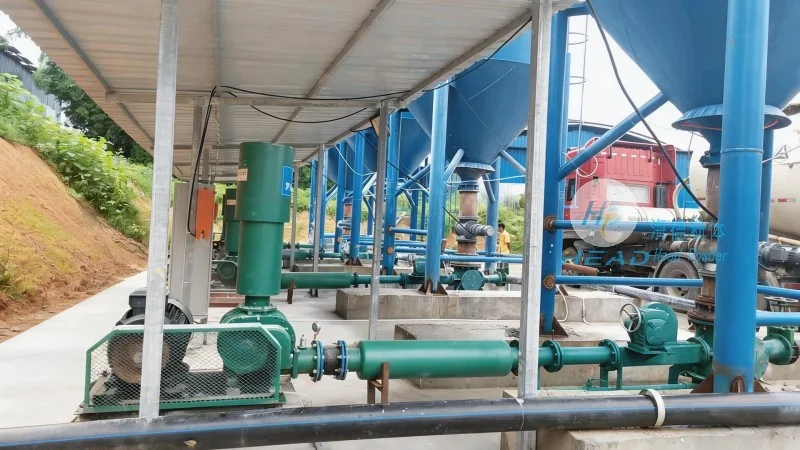
The system offers high material transport efficiency, reducing manual handling time and boosting plant productivity. Energy efficiency is another key advantage; technologies like belt or screw conveyors minimize energy use compared to traditional methods, lowering operational costs and carbon footprint. Environmental compliance is critical, with integrated filtration ensuring emissions stay within regulatory limits, helping avoid fines and maintain operational licenses.
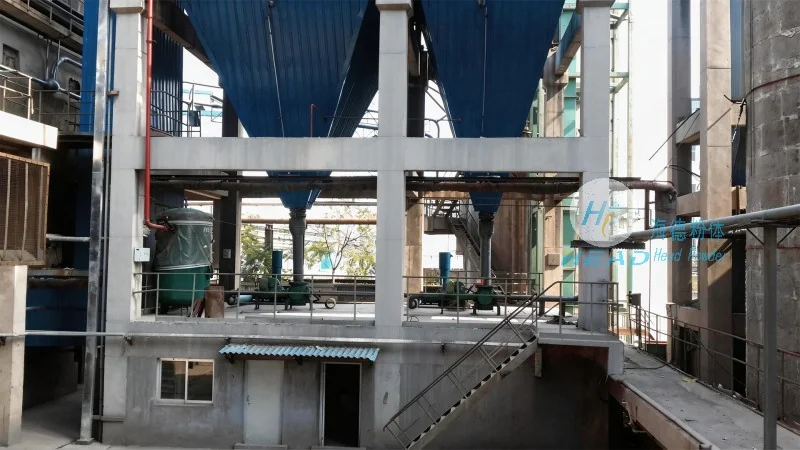
Maintenance simplicity is a notable benefit. Components are designed for easy access and routine maintenance, reducing specialized expertise needs and downtime. The modular design allows seamless integration with existing plant infrastructure, adapting to changing production needs.
Shandong HeadPowder Engineering Co., Ltd. is a leading provider of industrial material handling solutions, specializing in designing, manufacturing, and installing sintered dust removal material conveying systems. With strong presence in China, particularly in Shandong province, the company has extensive experience serving the iron and steel industry and other sectors requiring efficient dust management. The company’s commitment to quality, innovation, and customer satisfaction has established it as a trusted partner for businesses seeking reliable and effective material conveying solutions.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top