Efficient and reliable coal ash material handling equipment is crucial for modern industrial operations, particularly in power plants and waste management facilities. These systems are designed to transport, store, and process coal ash, a byproduct of coal combustion, ensuring safe and efficient handling throughout the entire process. Understanding the working principle and key features of such equipment is essential for optimizing operational efficiency and maintaining safety standards.
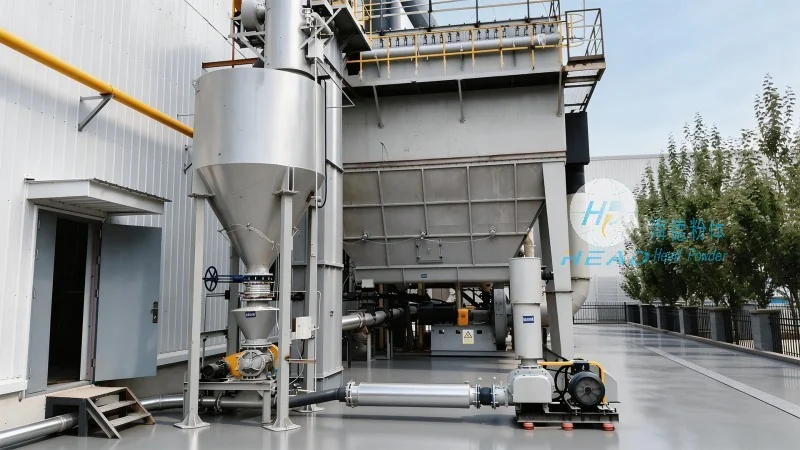
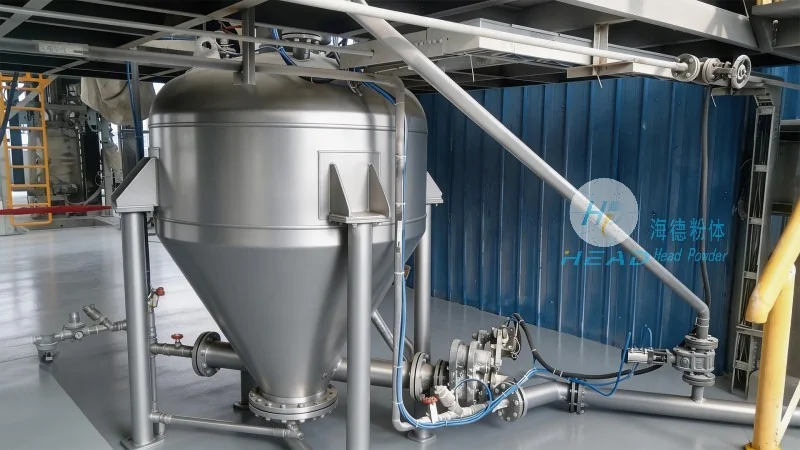
The working principle of coal ash material handling equipment typically involves a series of mechanical and control systems that work in tandem to move and manage coal ash. At the core of these systems is the conveyor mechanism, which may include belt conveyors, screw conveyors, or pneumatic conveyors, depending on the specific application and material characteristics. The equipment often starts with the collection of coal ash from storage silos or ash pits, where it is then transferred to the primary conveyor system. Sensors and control units monitor the flow rate, ensuring consistent and controlled movement. The system may also incorporate components such as feeders, hoppers, and transfer points to direct the material along the intended path. Additionally, some advanced systems utilize automation and digital controls to adjust the speed and direction of the conveyor based on real-time operational data, enhancing overall efficiency and reducing downtime.
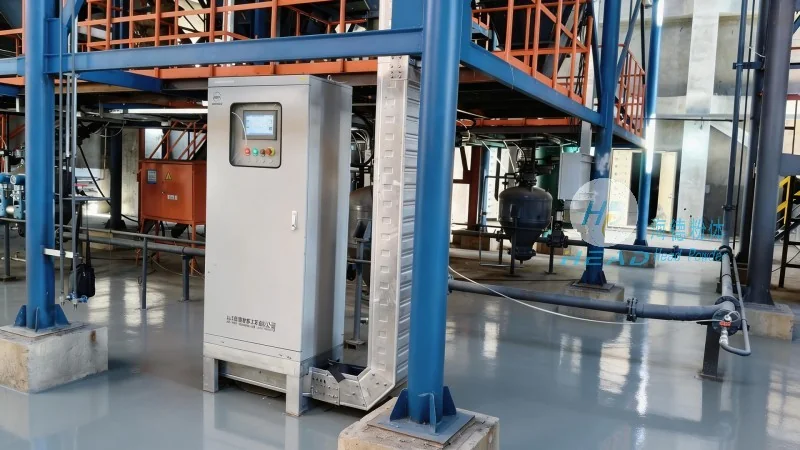
Coal ash material handling equipment is engineered with several key features that contribute to its effectiveness and reliability. One of the primary features is durability, as these systems are built to withstand the abrasive nature of coal ash and the harsh operating conditions often encountered in industrial settings. High-quality materials, such as stainless steel or specialized alloys, are commonly used in the construction of components like conveyor belts and hoppers to ensure long-term performance. Another critical feature is efficiency, with many systems designed to minimize energy consumption while maintaining high throughput rates. This is achieved through optimized conveyor designs, variable speed drives, and intelligent control systems that adjust operations based on the volume and density of the material being handled. Safety is also a paramount feature, with equipment incorporating safety guards, emergency stop buttons, and overload protection mechanisms to prevent accidents and ensure operator safety. Furthermore, many modern coal ash handling systems are equipped with monitoring and diagnostic tools that provide real-time data on system performance, allowing for proactive maintenance and reducing the risk of unexpected failures.
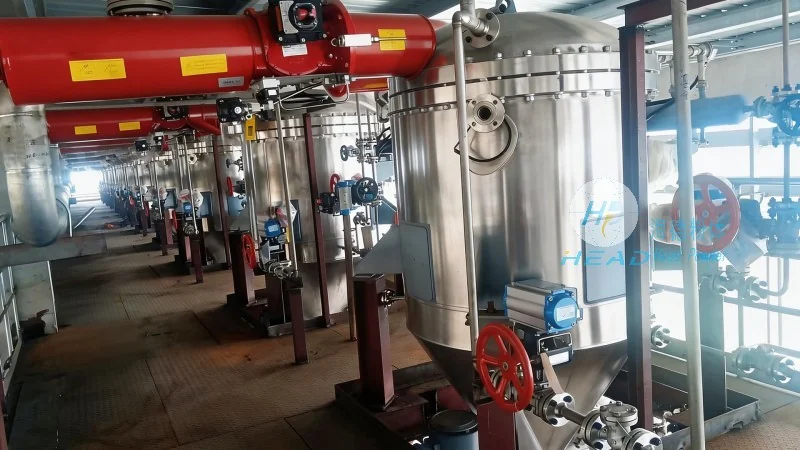
HeadPowder, a leading provider of industrial material handling solutions, specializes in the design, manufacturing, and installation of coal ash material handling equipment. With a strong presence in the industry, HeadPowder has established itself as a trusted partner for power plants and waste management facilities seeking reliable and efficient solutions. The company is headquartered in Shandong, China, and serves clients globally with customized equipment tailored to their specific operational needs. HeadPowder's commitment to quality and innovation ensures that their coal ash handling systems meet the highest standards of performance and safety, helping clients optimize their operations and reduce costs.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top