For industrial applications that require the efficient and reliable transport of bulk powder materials, specialized equipment plays a crucial role. The working principles and features of powder material handling equipment are designed to address the unique challenges associated with handling such materials, ensuring smooth operations and optimal performance in various production environments. This article explores the fundamental mechanisms behind these systems and highlights the key characteristics that make them indispensable in modern industrial settings.
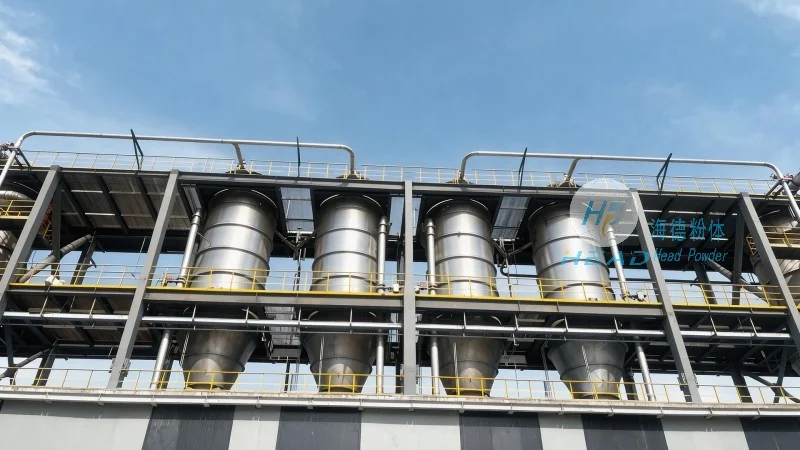
Powder material handling equipment operates on several core principles to move, store, and process bulk powders. The primary goal is to achieve consistent and controlled movement of materials while minimizing issues such as caking, segregation, and degradation. The most common working principles include gravitational, pneumatic, mechanical, and hydraulic systems. Each method is tailored to specific material properties and operational requirements, allowing for flexibility in application.
Gravitational systems rely on the natural force of gravity to move powders from higher to lower elevations. These systems are often used in simple conveying setups where the material can flow freely under the influence of gravity. However, they are limited by the need for a sufficient slope and the characteristics of the powder, such as its angle of repose and flowability. Mechanical systems, on the other hand, utilize components like screws, belts, and buckets to actively transport powders. Screw conveyors, for instance, use rotating screws to push material forward, making them suitable for horizontal or slight incline applications. Belt conveyors employ continuous belts to carry powders, offering high capacity and efficiency for long-distance transport.
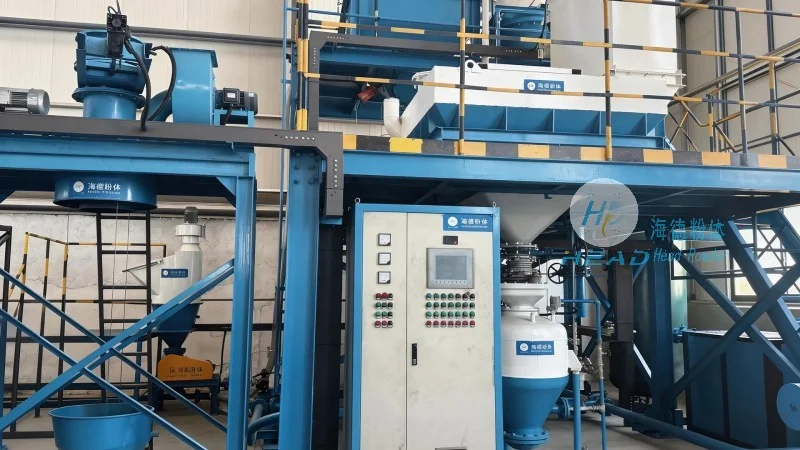
Pneumatic systems, or air conveying, operate by using compressed air to move powders through a pipeline. This method is particularly effective for handling fine powders and can achieve high speeds and distances. The principle involves creating a pressure differential that propels the material along the pipeline. Hydraulic systems, while less common in powder handling, use fluid power to drive mechanisms that move powders, often in applications requiring heavy-duty or high-pressure conditions.
The features of powder material handling equipment are critical in determining their suitability for specific industrial tasks. Key attributes include material handling capacity, flow control, system flexibility, and maintenance requirements. These features are designed to enhance operational efficiency and ensure the longevity of the equipment.
Material handling capacity refers to the volume of powder that the equipment can transport per unit of time. This is a critical factor for production planning and process optimization. Equipment with higher capacity can handle larger batches of material, reducing cycle times and increasing overall productivity. Flow control mechanisms are essential for maintaining consistent material flow rates, preventing overloading or underloading of downstream processes. Features such as variable speed drives, adjustable screw speeds, and air pressure regulation allow operators to fine-tune the flow according to production needs.
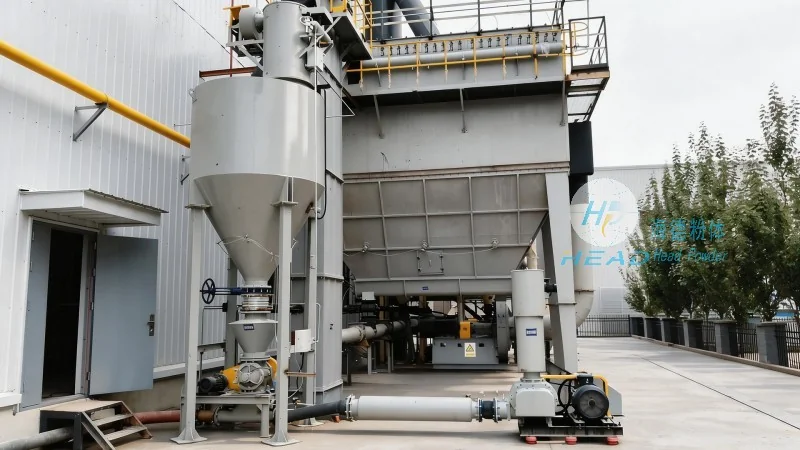
System flexibility is another important feature, as it allows equipment to adapt to different powder types and operational scenarios. Modular designs, interchangeable components, and adjustable configurations enable users to customize the system for specific applications. This flexibility reduces downtime and allows for easy integration into existing production lines. Maintenance requirements are also a key consideration, as equipment that is easy to maintain and service can minimize operational disruptions and lower long-term costs.
Powder material handling equipment is widely used across various industries, including pharmaceuticals, food processing, chemicals, and mining. The benefits of these systems extend beyond efficient material transport, encompassing improved safety, reduced material loss, and enhanced process control. By automating the handling of powders, these systems minimize human exposure to hazardous materials and reduce the risk of accidents. Additionally, they help in maintaining consistent product quality by ensuring uniform material flow and preventing segregation.
In the pharmaceutical industry, for example, the use of clean and sanitary powder handling equipment is crucial to meet regulatory standards and ensure product purity. The equipment must be designed to prevent contamination and allow for easy cleaning and sterilization. In the food industry, features such as stainless steel construction and hygienic design are essential to maintain food safety standards. The chemical industry benefits from equipment that can handle corrosive or abrasive powders, with materials like stainless steel and special coatings protecting against wear and degradation.
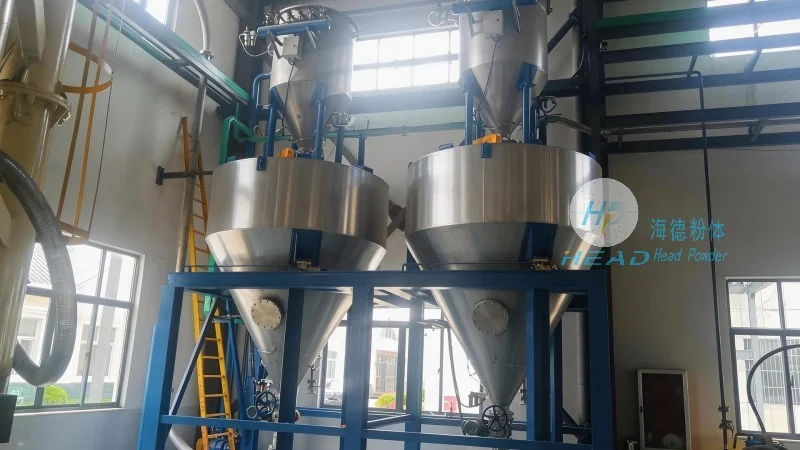
The mining industry utilizes powder handling equipment for transporting ore and other bulk materials from extraction sites to processing facilities. The robust and high-capacity systems used in mining applications are designed to withstand harsh conditions and heavy loads. Overall, the features and working principles of powder material handling equipment contribute significantly to the efficiency and reliability of industrial operations, making them a vital component in modern manufacturing and processing.
In conclusion, the working principles and features of powder material handling equipment are integral to the smooth operation of industrial processes involving bulk powders. By understanding these mechanisms and characteristics, industries can select the most appropriate equipment for their specific needs, leading to improved productivity, reduced costs, and enhanced product quality. The continued development of advanced powder handling technologies ensures that these systems will remain essential in the evolving landscape of industrial manufacturing.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top