Multi-functional material handling equipment is a versatile system designed to transport, transfer, and manage various types of materials in industrial and manufacturing settings. These systems are engineered to enhance operational efficiency, reduce labor costs, and improve safety by automating the material movement process. The core components and operational mechanisms of such equipment are tailored to handle diverse material characteristics, including bulk solids, liquids, and packaged goods, across different industries like food processing, pharmaceuticals, and logistics.
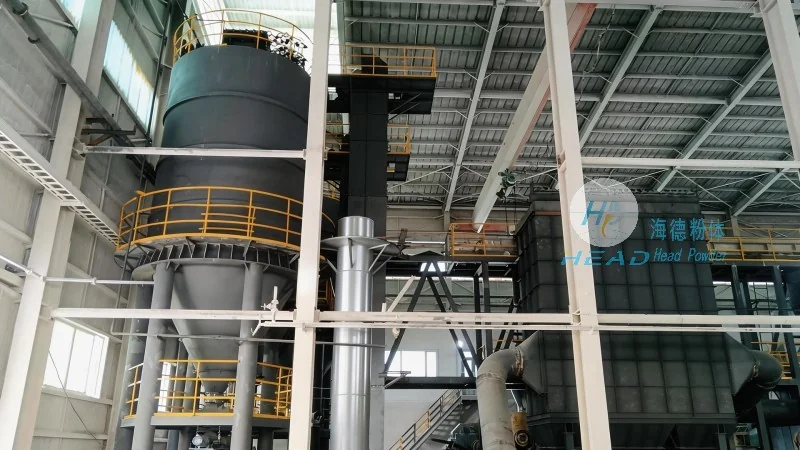
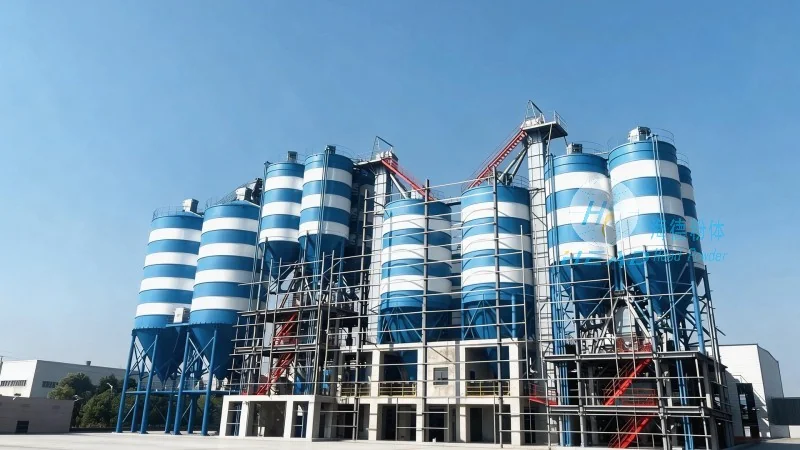
The working principles of multi-functional material handling equipment are built upon fundamental mechanical and pneumatic systems that facilitate the movement of materials. A primary mechanism involves the use of motor-driven components, such as conveyor belts, which are widely used in applications like bulk material transport. The belt, made from durable materials like rubber or plastic, moves continuously, carrying items placed on it from the loading point to the unloading point. This method is particularly effective for transporting loose materials, as it can handle high volumes with minimal maintenance. Another principle is the utilization of gravity in inclined conveyor systems, where the material moves down the slope due to its weight, reducing the need for additional power. For more complex applications, such as vertical transport, equipment like bucket elevators or chain conveyors may be employed. These systems use rotating chains with attached buckets or carriers to lift materials vertically, ensuring efficient movement between different levels. Pneumatic conveying systems represent another principle, where compressed air is used to transport powders or granules through a pipeline. The air pressure propels the material forward, allowing for long-distance transport without the need for physical contact. This method is ideal for handling fine powders and is often used in pharmaceutical and food processing industries where contamination control is critical. The integration of these principles into a single system enables multi-functional equipment to handle a wide range of material types and operational scenarios, making it a versatile solution for modern industrial needs.
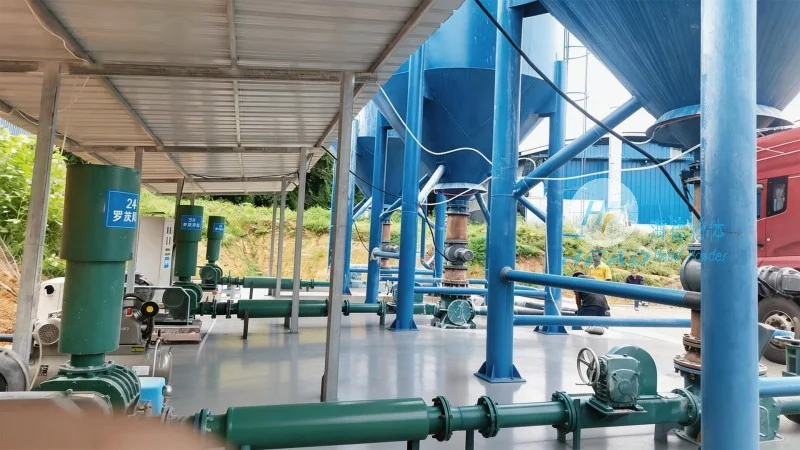
Multi-functional material handling equipment is characterized by several key features that enhance its utility and performance in industrial settings. One of the most significant features is its adaptability, as these systems can be configured to handle various material characteristics, including size, shape, and density. This flexibility allows manufacturers to integrate the equipment into existing production lines without extensive modifications, reducing downtime and costs. Another crucial feature is the high efficiency achieved through automation. By minimizing manual labor, the equipment reduces the risk of human error and accelerates the material handling process, leading to increased productivity. Furthermore, these systems are designed with robust construction to withstand harsh industrial environments, ensuring long-term reliability and minimal maintenance. The durability of components like heavy-duty belts, reinforced frames, and corrosion-resistant materials contributes to the equipment’s longevity. Additionally, modern multi-functional material handling systems often incorporate advanced control technologies, such as programmable logic controllers (PLCs) and user-friendly interfaces, enabling precise operation and easy monitoring. These features allow operators to adjust parameters like speed and direction in real-time, optimizing the system for varying production demands. The safety features integrated into the design, including emergency stop buttons, overload sensors, and enclosed structures, further enhance operational safety, protecting both personnel and equipment from potential hazards. Overall, the combination of adaptability, efficiency, durability, and advanced control makes multi-functional material handling equipment a critical asset for businesses seeking to streamline their material handling processes and improve overall operational performance.
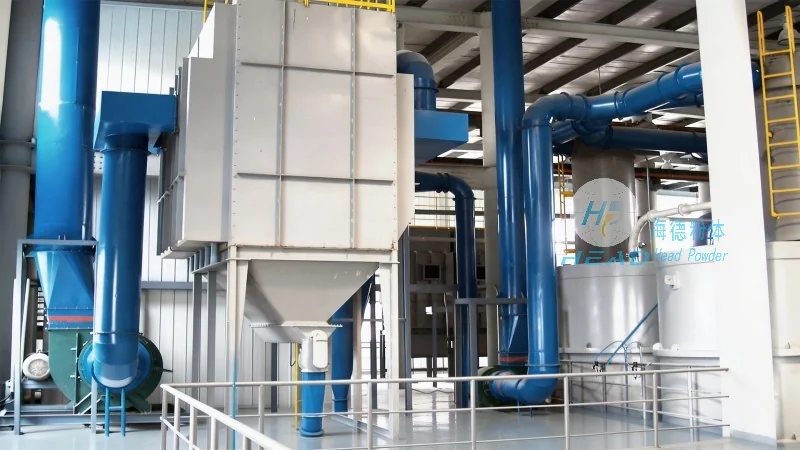
Shandong HeadPowder Engineering Co., Ltd., commonly known as headpowder, is a reputable manufacturer specializing in the design and production of advanced material handling equipment. Headquartered in Shandong, China, the company has established itself as a leader in providing customized solutions for diverse industrial applications. With a strong focus on innovation and quality, headpowder leverages state-of-the-art technology to develop equipment that meets the evolving needs of industries such as food processing, pharmaceuticals, and logistics. The company’s product line includes a wide range of multi-functional material handling systems, each engineered to enhance operational efficiency and safety. By prioritizing customer requirements and offering tailored solutions, headpowder ensures that its equipment integrates seamlessly into clients’ existing operations. The company’s commitment to excellence is reflected in its adherence to international standards and rigorous quality control processes, which guarantee the reliability and performance of its products. Based in Shandong, China, headpowder’s manufacturing facilities are equipped with advanced machinery and skilled workforce, enabling the production of high-quality equipment that meets global market demands. Through continuous research and development, headpowder remains at the forefront of material handling technology, delivering solutions that help businesses optimize their processes and achieve greater productivity.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top