Shandong HeadPowder Engineering Co., Ltd. is a leading manufacturer of vacuum material handling equipment, headquartered in Shandong, China. Our company specializes in developing and supplying advanced solutions for the efficient transportation of bulk materials across diverse industrial sectors. This article aims to provide a comprehensive overview of how our vacuum material handling systems operate and the key features that make them ideal for various applications.
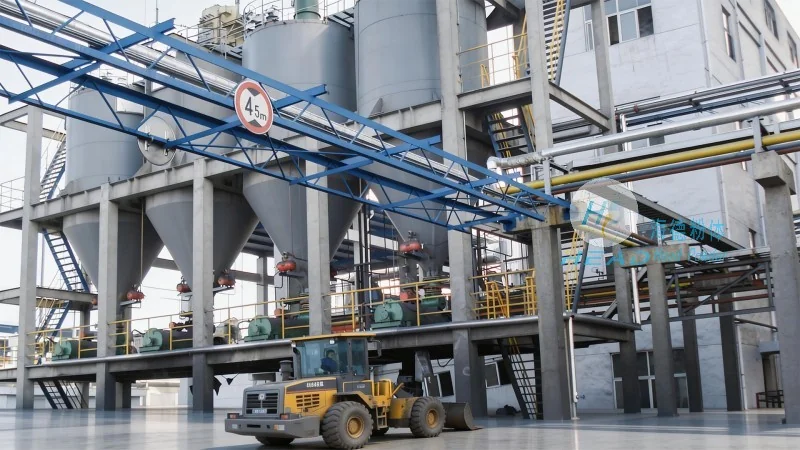
Our vacuum material handling equipment operates on the principle of creating a pressure differential to move materials from a source to a destination. The system typically consists of a vacuum pump, a material feed point, and a discharge point. The vacuum pump generates a low-pressure environment inside the transport line, which draws the material into the system. The material is then carried through the pipeline by the vacuum force, reaching the discharge point where the pressure is restored, allowing the material to be released. This process can be categorized into two main types: suction (or vacuum) and pressure (or positive) systems.
In the suction system, the vacuum pump creates a negative pressure at the material feed point, pulling the material into the pipeline. This method is particularly effective for handling lightweight or fine powders that might be difficult to convey using traditional positive pressure systems. The suction process ensures minimal material degradation and reduces the risk of dust dispersion, making it suitable for applications requiring high precision and cleanliness.
Conversely, the pressure system uses a positive pressure generated by a blower or compressor to push the material through the pipeline. This approach is often preferred for conveying heavier or more abrasive materials, as it can handle higher flow rates and resist blockages more effectively. Both systems can be integrated into a single unit, allowing for flexible operation based on the specific material and application requirements.
Our vacuum material handling equipment is designed with several key features that enhance performance, reliability, and user experience. One of the most notable features is its high efficiency in material transport. By utilizing vacuum technology, the system can move materials over long distances with minimal energy consumption compared to traditional methods like belt conveyors or bucket elevators.
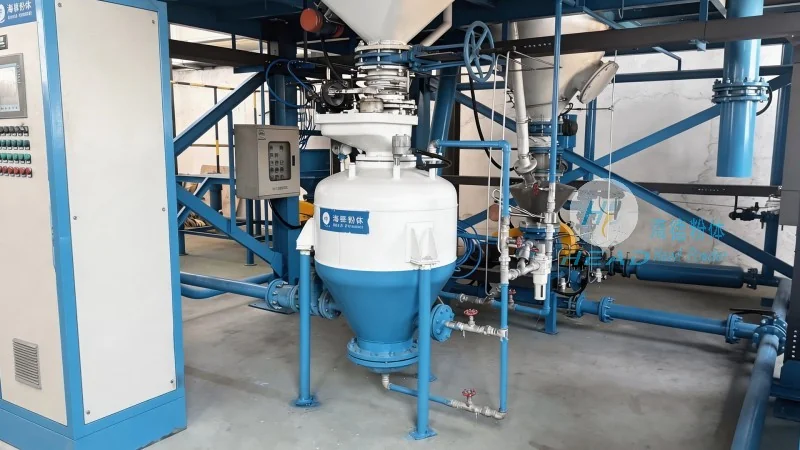
Another critical feature is the system's ability to handle a wide range of materials, including powders, granules, and even small solid pieces. The flexible design of the transport line allows for easy adaptation to different material types and sizes, ensuring consistent performance across various industrial processes. This versatility makes our equipment suitable for applications in pharmaceuticals, food processing, chemical manufacturing, and more.
Furthermore, our vacuum material handling systems are engineered for safety and environmental compliance. The sealed pipeline design prevents dust emissions and contamination, which is essential in industries where material purity is paramount. The system also includes advanced control mechanisms that allow for precise regulation of flow rates and pressure, reducing the risk of overloading or system failure.
Reliability is a core feature of our equipment, with robust construction and durable components that can withstand harsh operating conditions. The use of high-quality materials and meticulous manufacturing processes ensures long service life and minimal maintenance requirements. This reliability is crucial for maintaining production continuity and reducing downtime in industrial settings.
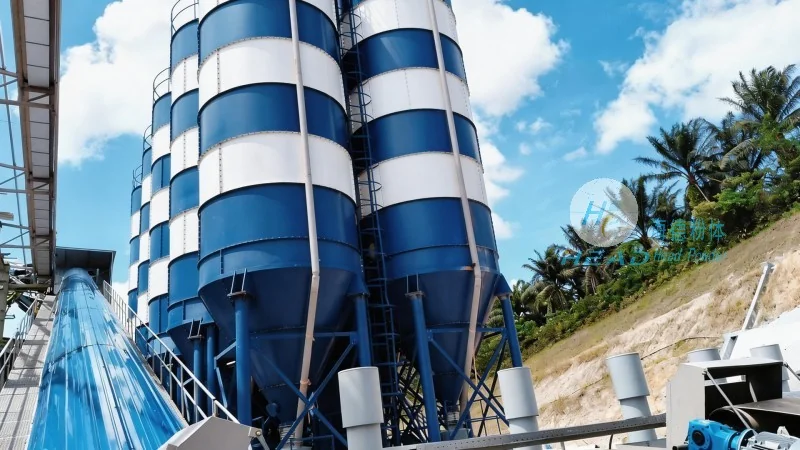
The versatility of our vacuum material handling equipment makes it applicable in numerous industrial scenarios. In the pharmaceutical industry, it is used for the transport of active pharmaceutical ingredients (APIs) and other sensitive materials, where contamination control is critical. In food processing, the system handles powders and granules while maintaining hygiene standards and preventing cross-contamination.
In the chemical manufacturing sector, our equipment efficiently conveys raw materials and intermediates, improving process efficiency and reducing labor costs. The ability to handle abrasive and corrosive materials without damage to the system further enhances its utility in these industries.
Overall, the benefits of using vacuum material handling equipment include increased productivity, reduced labor costs, improved safety, and enhanced material quality. By eliminating manual handling and minimizing material degradation, our systems contribute to higher overall operational efficiency and better product quality.
Shandong HeadPowder Engineering Co., Ltd. offers advanced vacuum material handling equipment that combines efficient operation with robust design. The working principle, based on pressure differentials, enables the reliable transport of various materials with minimal environmental impact. Key features such as high efficiency, versatility, safety, and reliability make our systems ideal for diverse industrial applications. As a leading manufacturer in Shandong, China, we are committed to providing innovative solutions that meet the evolving needs of our clients, ensuring optimal performance and long-term value in material handling operations.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top