Ammonium chloride is a widely used chemical compound in various industrial applications, and efficient handling of this material is crucial for maintaining production efficiency and safety. The pneumatic conveying system equipment designed for ammonium chloride offers a reliable solution for transporting this material from one location to another within industrial facilities. This article will explore the working principle and key features of such systems, providing insights into how they operate and the advantages they bring to industrial processes.
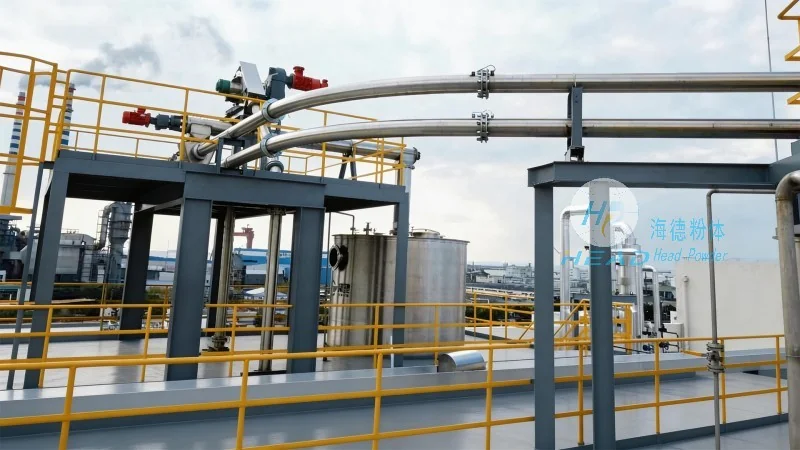
The core of an ammonium chloride pneumatic conveying system lies in its ability to transport bulk materials through the use of air or gas as the conveying medium. The system typically consists of several key components, including a hopper for material storage, a feeder to control the flow rate, a conveying line (often a pipe), and a receiver for the material at the destination. The working principle involves creating a pressure differential between the hopper and the receiver, which is achieved by either suction (negative pressure) or pressure (positive pressure) methods.
In the suction method, a vacuum is created at the receiver end, drawing the ammonium chloride particles along with the air through the conveying line. The feeder regulates the material flow into the system, ensuring a consistent and controlled rate. The air velocity within the pipe is maintained at a level sufficient to keep the particles in suspension, preventing blockages and ensuring smooth transport. At the receiving end, the material is separated from the air, often through a cyclone or filter, and collected in the receiver. This method is particularly useful for long-distance or high-rise applications where the material needs to be lifted or transported over significant vertical distances.
The pressure method, on the other hand, involves blowing air or gas into the conveying line at the hopper end, creating a positive pressure that pushes the ammonium chloride particles through the pipe. This approach is generally more suitable for shorter distances and horizontal or slightly inclined transport. The pressure system ensures that the material is continuously pushed forward, maintaining a steady flow rate. Both methods rely on the principle of fluidization, where the air or gas flow creates a fluid-like environment for the particles, allowing them to move freely without sticking to the pipe walls.
When evaluating pneumatic conveying systems for ammonium chloride, several key features stand out as critical for optimal performance and reliability. These features are designed to address the specific challenges associated with handling this chemical, such as its hygroscopic nature and potential for dust generation.
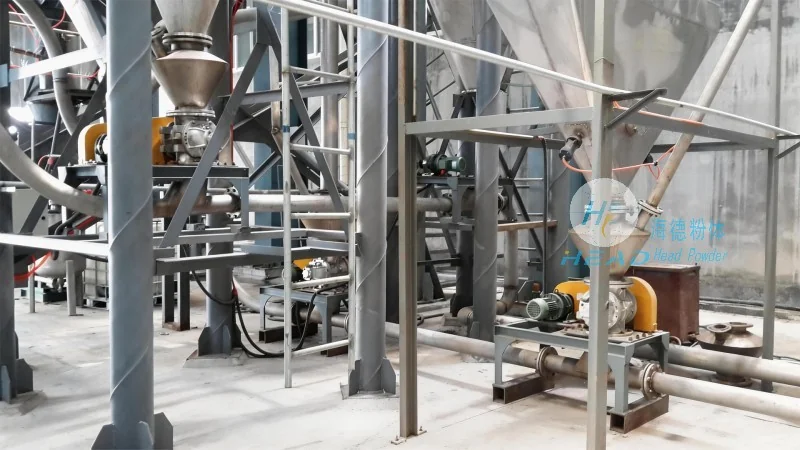
Firstly, the system incorporates dust control measures to minimize the release of fine particles into the environment. This is achieved through the use of sealed hoppers and receivers, as well as filtration systems at the receiving end. The dust control features not only enhance safety by reducing exposure to airborne particles but also help maintain the quality of the ammonium chloride by preventing moisture absorption from the air, which could affect its properties.
Secondly, the equipment is engineered for durability and resistance to corrosion, given the chemical properties of ammonium chloride. The materials used in the construction of the conveying line, hoppers, and other components are selected to withstand the corrosive effects of the material over extended periods. This ensures that the system maintains its structural integrity and operational efficiency, reducing the need for frequent maintenance and replacement.
Thirdly, the system offers flexibility in terms of transport distance and layout. Whether the application requires horizontal, vertical, or a combination of both, the pneumatic conveying system can be configured to meet the specific requirements. The modular design allows for easy expansion or modification as production needs change, providing a long-term solution that adapts to evolving industrial demands.
Additionally, the equipment is designed with safety and operational efficiency in mind. Features such as overload protection, pressure relief valves, and automatic shut-off mechanisms help prevent accidents and ensure smooth operation. The system's ability to handle varying flow rates and material characteristics makes it a versatile choice for different production scenarios, from small-scale operations to large-scale industrial facilities.
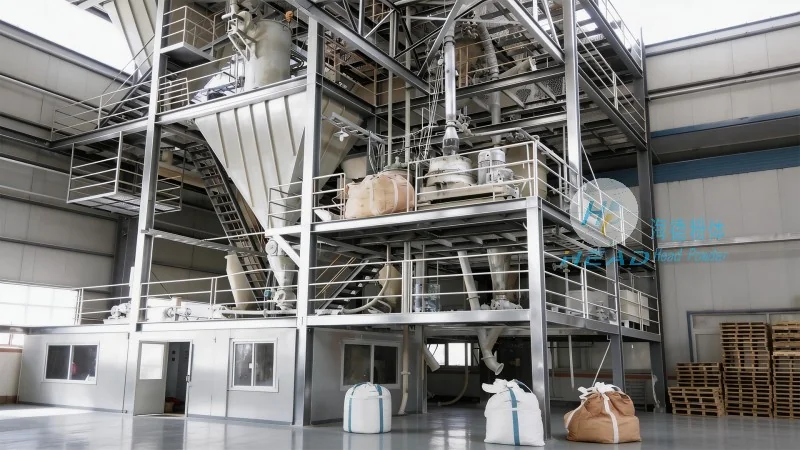
The adoption of pneumatic conveying systems for ammonium chloride offers numerous benefits that contribute to improved operational performance and cost-effectiveness. One of the primary advantages is the reduction in labor costs associated with manual handling of bulk materials. By automating the transport process, the system minimizes the need for manual labor, reducing the risk of human error and increasing overall efficiency.
Another significant benefit is the improvement in material quality and consistency. The enclosed system prevents contamination from external sources, such as moisture or other chemicals, which could affect the purity of the ammonium chloride. This is particularly important in applications where the material is used in sensitive processes, such as pharmaceuticals or food production, where quality control is paramount.
The system also contributes to enhanced safety in the workplace. By eliminating the need for manual handling and reducing the exposure to dust and airborne particles, the risk of respiratory issues and other health hazards is minimized. This not only protects the workforce but also helps in maintaining compliance with occupational health and safety regulations.
Furthermore, the pneumatic conveying system offers energy efficiency compared to traditional methods like belt conveyors or bucket elevators. The use of air as the conveying medium reduces the energy consumption associated with mechanical movement, leading to lower operational costs over time. The system's ability to handle both small and large quantities of material efficiently makes it a cost-effective solution for various production scales.
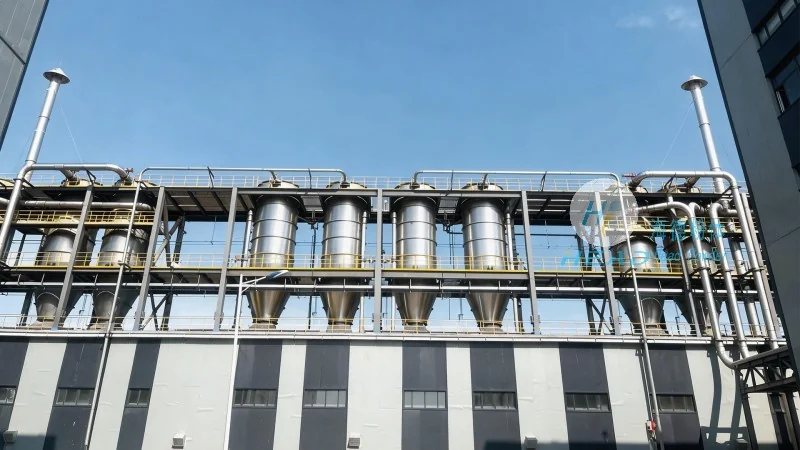
The versatility of ammonium chloride pneumatic conveying systems makes them suitable for a wide range of applications across different industries. In the chemical industry, these systems are commonly used for transporting ammonium chloride between production units, such as from a reactor to a drying or packaging facility. The ability to handle large volumes of material quickly and efficiently supports the continuous production process.
In the agricultural sector, the system is employed in fertilizer production facilities, where ammonium chloride is used as a nitrogen source. The pneumatic conveying system ensures that the material is transported safely and efficiently from storage silos to mixing and packaging areas, maintaining the quality of the fertilizer product.
Additionally, the system finds applications in the pharmaceutical and food processing industries, where the hygienic and dust-free nature of the conveying process is critical. The enclosed design and filtration systems help maintain the purity of the material, ensuring compliance with regulatory standards for these industries.
Overall, the ammonium chloride pneumatic conveying system is a reliable and efficient solution for material handling in various industrial settings. By understanding its working principle and key features, industries can make informed decisions about implementing such systems to enhance their operational performance and safety.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top