Small bag bulk material pneumatic conveying systems represent a sophisticated and efficient method for handling and transporting bulk materials from their original packaging to processing or storage facilities. This technology is particularly valuable in industries where materials are initially packaged in small bags, such as chemicals, food products, and powders, requiring a seamless transition from the bag to the production line. The system integrates bag opening, material extraction, and pneumatic transport into a single, automated process, enhancing operational efficiency and reducing manual handling risks. By eliminating the need for manual bag emptying and material transfer, these systems streamline workflows and improve overall productivity in industrial settings.
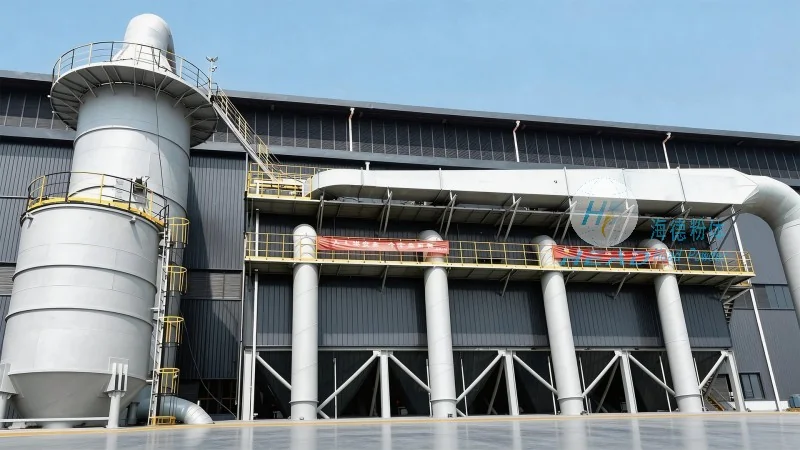
At the core of small bag bulk material pneumatic conveying systems is the use of air pressure to move material particles through a pipeline. The process typically begins with the opening of the small bag, which can be achieved through mechanical means or by using compressed air to rupture the bag. Once the bag is opened, the material is drawn into a hopper or feeder, where it is then conveyed through a series of pipes using a combination of positive and negative pressure. The system utilizes a blower or compressor to generate the necessary air flow, which propels the material along the pipeline. Key components include the bag opener, feeder, airlock, and the conveying pipeline itself. The entire process is designed to be continuous and low-maintenance, ensuring consistent material flow and minimal downtime. The system can operate under positive pressure (pressure conveying) or negative pressure (suction conveying), with each method suited to different material characteristics and pipeline configurations.
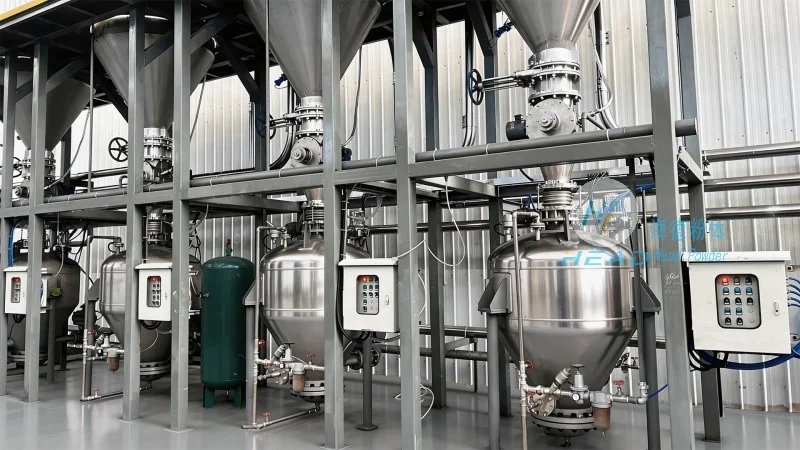
Small bag bulk material pneumatic conveying systems offer several distinct advantages that make them ideal for modern industrial applications. One of the primary benefits is the reduction in manual labor, as the system automates the entire bag-to-pipe transition. This not only improves safety by minimizing human exposure to bulk materials but also enhances productivity by allowing operators to focus on other tasks. Additionally, the system provides a hygienic and dust-free environment, which is crucial for industries like food and pharmaceuticals where contamination control is paramount. The compact design of the system allows for easy integration into existing production lines, and its modular construction enables customization to suit specific material characteristics and processing requirements. Another advantage is the ability to handle a wide range of materials, from fine powders to coarse granules, with consistent performance and minimal material degradation. Furthermore, the system is energy-efficient, with optimized air flow reducing operational costs and environmental impact.
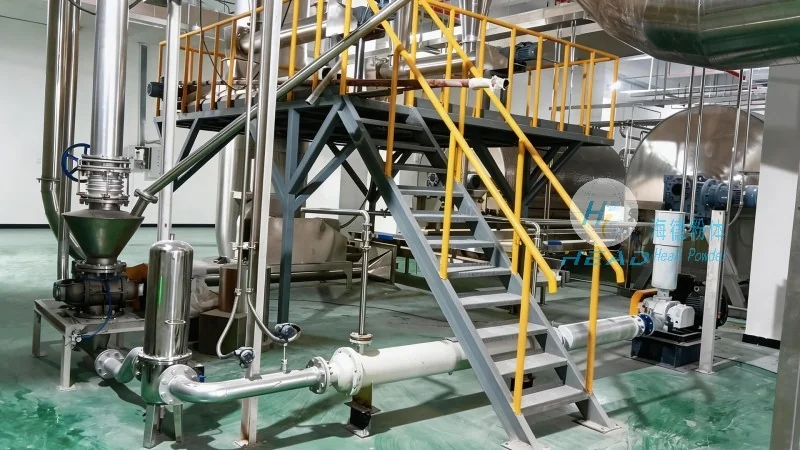
The versatility of small bag bulk material pneumatic conveying systems makes them suitable for a variety of industrial applications. In the chemical industry, these systems are commonly used to transport raw materials such as powders and granules from storage bags to reactors or mixing tanks. For example, in a pharmaceutical manufacturing plant, the system can efficiently transfer active pharmaceutical ingredients (APIs) from sealed bags into high-purity processing equipment, maintaining strict contamination control. In the food and beverage sector, the system is utilized for handling ingredients like flour, sugar, and spices, ensuring that the production process remains clean and efficient. The hygienic design of the system, with smooth surfaces and easy-to-clean components, is particularly important in food processing facilities to meet regulatory standards. In the agricultural sector, the system is widely used for processing and transporting bulk agricultural products, such as grains and seeds, from storage to processing units. Each application benefits from the system's ability to handle materials in a controlled and efficient manner, reducing waste and improving overall operational efficiency.
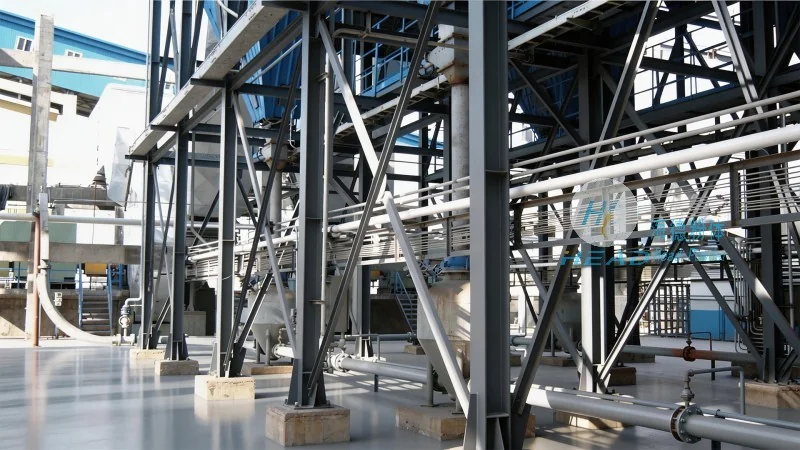
Shandong HeadPowder Engineering Co., Ltd., operating under the brand name headpowder, specializes in the design, manufacturing, and installation of advanced material handling systems, including small bag bulk material pneumatic conveying systems. With headquarters located in Shandong, China, the company leverages over decades of industry experience to deliver customized solutions tailored to the unique needs of each client. The company's team of engineers and technicians works closely with clients to assess their material handling challenges and develop optimal system configurations. Post-installation, headpowder provides comprehensive support, including maintenance services, spare parts supply, and technical training to ensure the system operates at peak efficiency throughout its service life. By combining innovative technology with expert service, headpowder ensures that clients achieve reliable, cost-effective material handling solutions that meet their operational and regulatory requirements. The company adheres to international quality standards and continuously invests in research and development to enhance the performance and reliability of its systems, positioning itself as a leading provider in the material handling industry.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top