For industrial applications that require the efficient handling of diatomite powder, understanding the underlying technology of conveying systems is crucial. This article delves into the working principle and key features of diatomite powder conveying systems, providing insights into how these systems operate and why they are essential in various industrial processes.
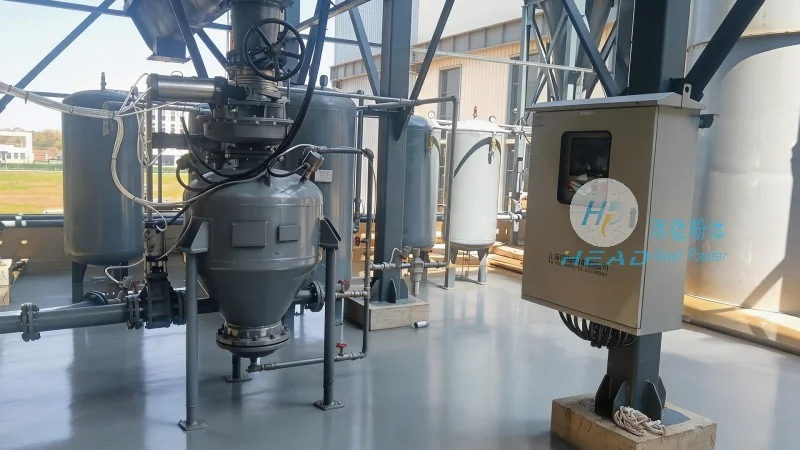
Diatomite, a natural sedimentary rock composed primarily of fossilized diatoms, is widely used in industries such as filtration, cosmetics, and construction due to its high porosity and lightweight properties. The efficient transport of diatomite powder from storage to processing units is a critical step in many production lines. Diatomite powder conveying systems are engineered to handle this material safely and effectively, minimizing dust generation and ensuring consistent flow rates.
At the core of diatomite powder conveying systems is a combination of mechanical and pneumatic components designed to move the fine powder through a pipeline. The primary working principle involves the use of air or pressure to create a flow of material. In pneumatic conveying systems, for example, a fan or blower generates a stream of air that pulls the diatomite powder particles into the conveying line. The system typically includes a hopper for material storage, a feeder to control the flow rate, and a pipeline network that transports the powder to the destination point, such as a mixer or storage silo.
Another common method is the use of mechanical conveyors, such as screw conveyors or belt conveyors, which rely on rotating components to push the powder along a fixed path. These systems are often used for bulk material handling and can be integrated with dust collection systems to maintain a clean working environment. The choice between pneumatic and mechanical conveying depends on factors like the particle size, moisture content, and the distance the powder needs to be transported.
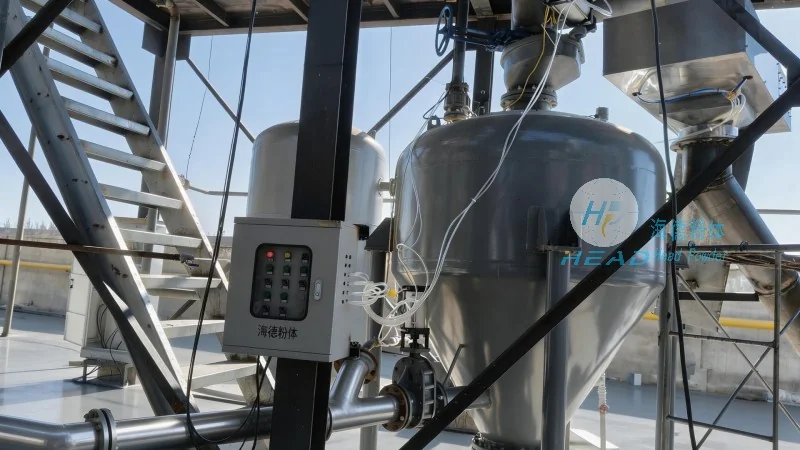
Effective diatomite powder conveying systems are characterized by several key features that enhance performance and safety. One of the most important features is the ability to minimize dust generation. Since diatomite is a fine powder, excessive dust can pose health risks and affect product quality. Advanced systems incorporate sealed hoppers, airtight pipelines, and efficient dust collection mechanisms to keep the environment clean and safe for operators.
Another critical feature is the control of flow rate and pressure. Precise control ensures that the diatomite powder is conveyed at the optimal speed, preventing blockages and maintaining consistent product quality. Modern systems often include variable speed drives and pressure sensors that allow for real-time adjustments, adapting to changes in material properties or system conditions.
Corrosion resistance is also a significant feature, especially when handling diatomite that may contain moisture or acidic components. Materials like stainless steel or specialized coatings are used for components that come into direct contact with the powder to prevent degradation and ensure long-term durability.
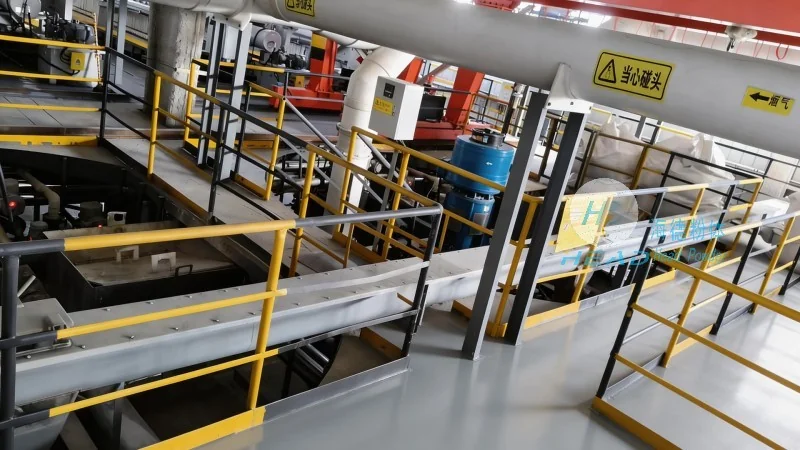
Energy efficiency is another key aspect. By optimizing the air flow and conveyor speed, systems can reduce energy consumption while maintaining performance. This not only lowers operational costs but also aligns with sustainability goals in industrial operations.
Diatomite powder conveying systems are widely used in various industrial applications. In the filtration industry, for example, these systems transport diatomite to filter media production lines, where it is mixed with binders to create high-quality filter papers. In the cosmetics industry, the consistent delivery of diatomite powder is essential for maintaining product uniformity and texture. The construction industry also benefits from these systems when using diatomite as a lightweight aggregate in concrete or insulation materials.
The benefits of using advanced diatomite powder conveying systems extend beyond efficiency. By reducing dust and improving material handling, these systems enhance workplace safety and reduce maintenance costs. The consistent flow of material also leads to higher production throughput and better product quality, which are critical factors for businesses aiming to stay competitive in their respective markets.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top