Desulfurization sodium bicarbonate, also known as sodium bicarbonate used in flue gas desulfurization processes, is a critical chemical in industrial applications. The efficient handling and conveying of this powder are essential for maintaining the performance of desulfurization systems. This article explores the working principle and key characteristics of the powder conveying system for desulfurization sodium bicarbonate, with a focus on the expertise of Shandong HeadPowder Engineering Co., Ltd.
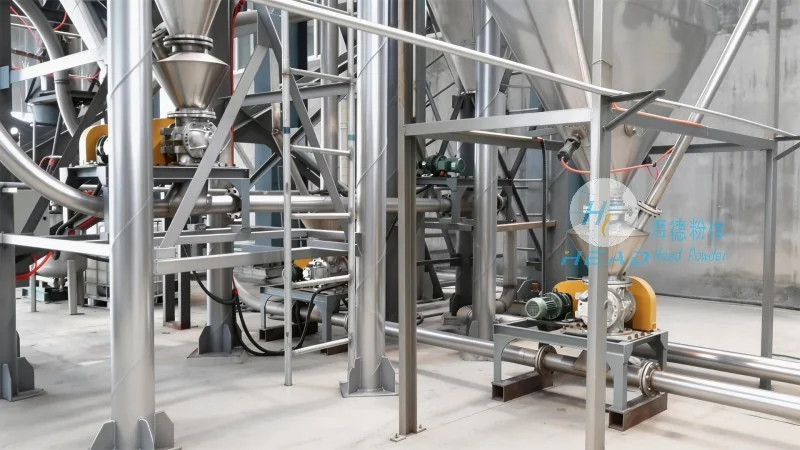
Shandong HeadPowder Engineering Co., Ltd., operating under the brand name headpowder, is a specialized company based in Shandong, China. With a strong background in powder processing and conveying technologies, the company has developed advanced solutions tailored to the unique requirements of desulfurization processes. The company's expertise lies in designing and implementing systems that ensure reliable and efficient transportation of sodium bicarbonate, a key component in flue gas desulfurization (FGD) systems used to reduce sulfur dioxide emissions from industrial sources.
The conveying system for desulfurization sodium bicarbonate typically operates based on principles of pneumatic or mechanical transport, depending on the specific application and scale of the desulfurization plant. In pneumatic conveying systems, the powder is transported using compressed air or other gas streams, which creates a flow that moves the particles through pipelines. This method is particularly effective for handling fine powders like sodium bicarbonate, as it minimizes particle degradation and ensures consistent flow rates. The system generally includes components such as feeders, conveying lines, and control units that work in tandem to maintain the desired flow and pressure conditions. For mechanical conveying, systems like screw conveyors or belt conveyors may be employed, especially in applications where the powder needs to be moved over longer distances or at higher capacities. These mechanical systems rely on rotating parts to move the powder, providing a continuous and reliable transport solution. The choice between pneumatic and mechanical conveying depends on factors such as the particle size, moisture content, and the overall system requirements of the desulfurization plant.
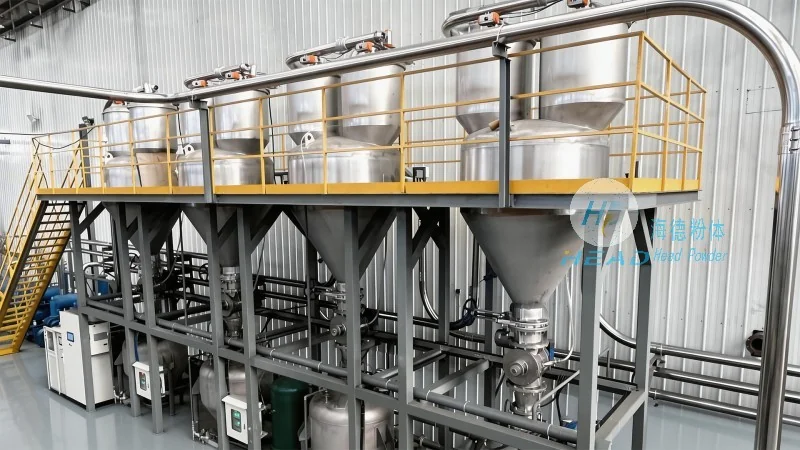
The conveying system for desulfurization sodium bicarbonate exhibits several important characteristics that contribute to its effectiveness and reliability. One of the primary features is its ability to handle fine, dry powders without causing agglomeration or blockages. This is crucial because sodium bicarbonate particles are often small and can easily clump together, which could lead to system inefficiencies or equipment damage. The system is designed with materials that are resistant to corrosion and wear, as the sodium bicarbonate and the gases it interacts with can be abrasive. Additionally, the system incorporates features for precise control of flow rates and pressure, ensuring that the powder is delivered to the desulfurization reactor at the correct concentration and volume. This control is vital for maintaining the optimal operating conditions of the FGD system, which directly impacts the efficiency of sulfur dioxide removal. Another characteristic is the system's adaptability to varying load conditions, allowing it to handle fluctuations in the amount of sodium bicarbonate being processed. This flexibility is essential in industrial settings where production rates may change over time. The system also includes safety features to prevent dust explosions, which is a critical consideration given the nature of the powder and the gases involved in the desulfurization process. These safety measures, such as explosion-proof designs and dust collection systems, ensure that the conveying operation is conducted in a secure environment.
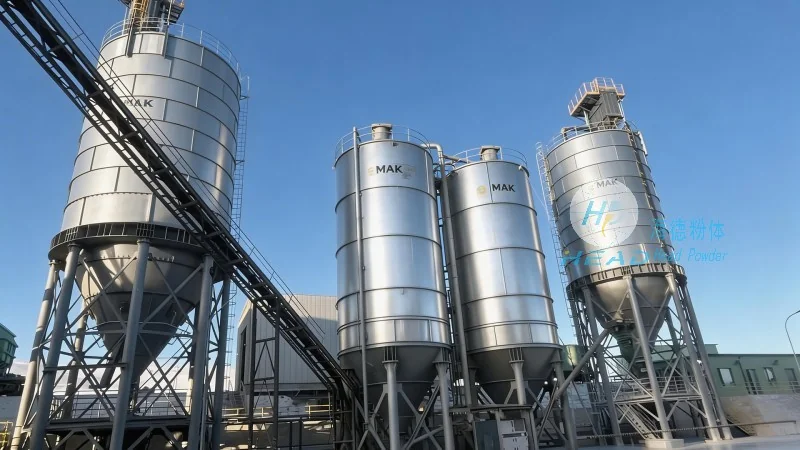
The efficient conveying of desulfurization sodium bicarbonate offers several advantages that enhance the performance of flue gas desulfurization systems. By ensuring a consistent and reliable supply of the chemical, the system helps maintain the optimal pH levels and reaction conditions within the desulfurization reactor. This leads to higher removal efficiencies of sulfur dioxide, which is a major goal in environmental protection efforts. The system also reduces downtime and maintenance costs by minimizing the risk of blockages and equipment failure. In industrial plants, where continuous operation is essential, the reliability of the powder conveying system is paramount. The use of advanced materials and control technologies in the system contributes to its long service life and low maintenance requirements. The applications of this conveying system are widespread in industries such as power generation, petrochemical, and steel production, where flue gas desulfurization is a standard practice to comply with environmental regulations. The system's ability to handle large volumes of sodium bicarbonate at high speeds makes it suitable for both small-scale and large-scale desulfurization plants.
In conclusion, the working principle and characteristics of the desulfurization sodium bicarbonate powder conveying system are critical to the effective operation of flue gas desulfurization processes. The system, developed by companies like Shandong HeadPowder Engineering Co., Ltd., combines advanced engineering with robust materials to ensure reliable and efficient transport of the powder. By understanding the working principles and key characteristics, industrial facilities can optimize their desulfurization systems, leading to improved environmental performance and operational efficiency. The expertise of companies such as headpowder in this field is essential for meeting the growing demands for sustainable and effective sulfur dioxide removal in industrial applications.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top