Desulfurization and dust removal processes in power plants and industrial facilities generate large volumes of fly ash, which requires efficient and reliable powder conveying systems for safe handling and disposal. The HeadPowder Engineering Co., Ltd., a leading provider in Shandong, China, specializes in designing and manufacturing advanced systems tailored to meet these demanding requirements. This article explores the working principle and key features of the desulfurization and dust removal fly ash powder conveying system, highlighting how it enhances operational efficiency and environmental compliance.
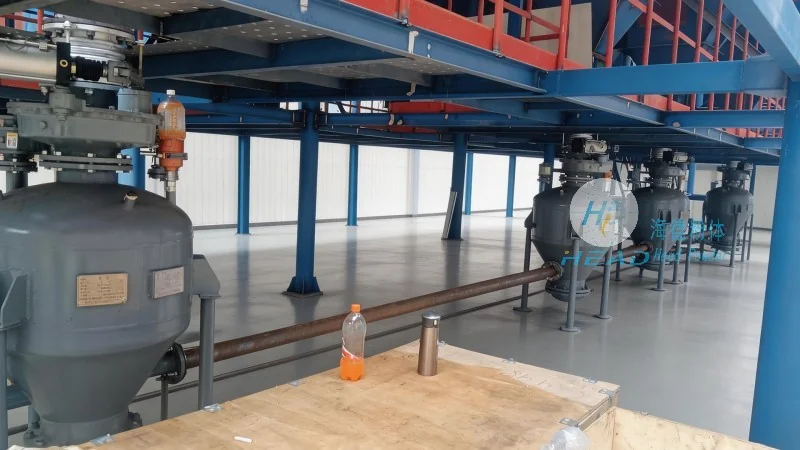
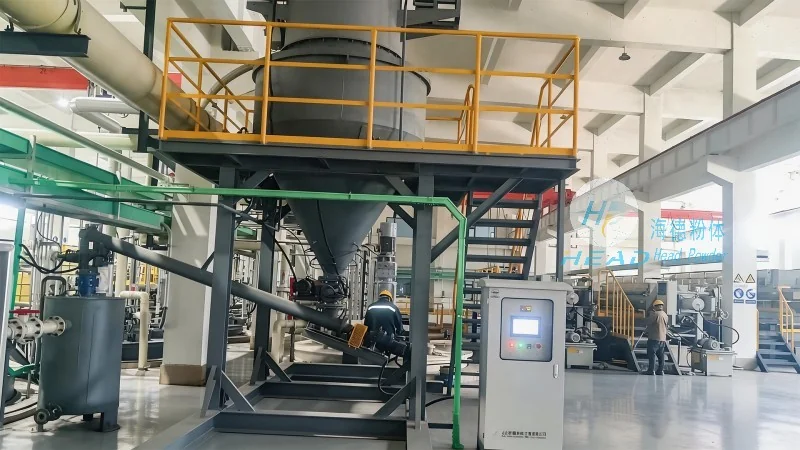
The desulfurization and dust removal fly ash powder conveying system operates on a principle of pneumatic or mechanical transport, depending on the specific application and material characteristics. For most industrial settings, a combination of positive pressure air or vacuum suction is employed to move the fine ash particles from the collection points to storage or disposal locations. The system typically consists of several key components, including ash hoppers, feeders, conveying pipelines, and control units. The process begins with the ash being collected in the hoppers, where it is then fed into the conveying line through a rotary valve or screw feeder. The air or vacuum system then propels the ash through the pipelines, ensuring a consistent and controlled flow. Advanced control systems monitor pressure, flow rate, and material level, providing real-time adjustments to maintain optimal performance. This integrated approach ensures that the fly ash is transported safely and efficiently, minimizing dust emissions and operational risks.
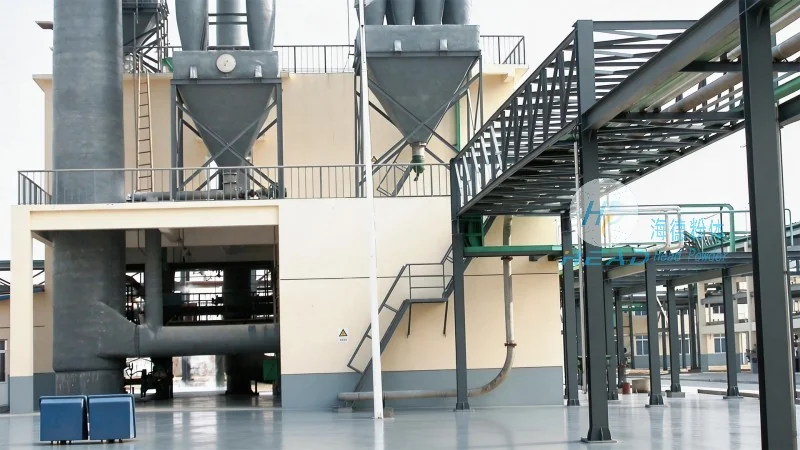
The HeadPowder Engineering Co., Ltd. system is characterized by several distinctive features that set it apart in the industry. Firstly, it incorporates high-efficiency filtration and dust collection mechanisms to prevent particulate matter from escaping into the environment. This not only complies with stringent environmental regulations but also enhances workplace safety by reducing respiratory hazards. Secondly, the system is designed for low maintenance and high reliability, with robust components that can withstand the abrasive nature of fly ash. The use of corrosion-resistant materials and advanced sealing technologies extends the service life of the equipment, reducing downtime and operational costs. Thirdly, the system offers flexible configuration options, allowing customization to suit various plant layouts and processing capacities. This adaptability makes it suitable for both new installations and retrofit applications in existing facilities. Additionally, the system integrates seamlessly with existing plant control networks, enabling centralized monitoring and management. The result is a comprehensive solution that addresses the unique challenges of fly ash handling while optimizing overall plant performance.
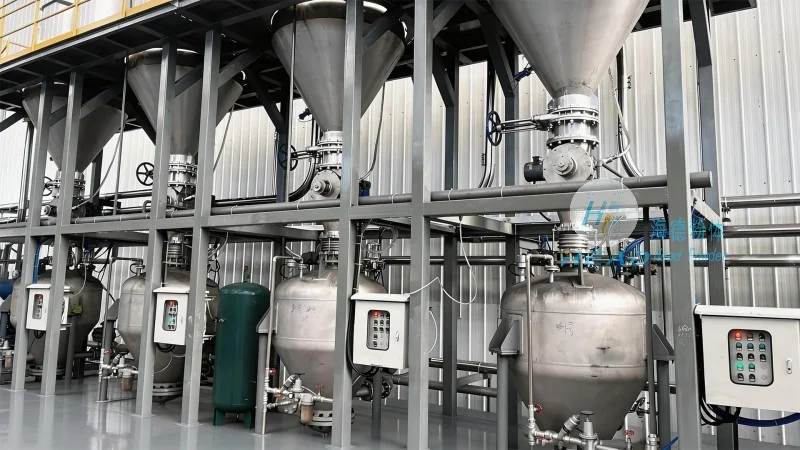
The implementation of the desulfurization and dust removal fly ash powder conveying system brings numerous benefits to industrial operations. By improving the efficiency of ash transport, plants can reduce handling time and labor costs. The system's ability to handle large volumes of fine particles minimizes the risk of blockages and system failures, ensuring continuous operation. Furthermore, the advanced filtration and dust control features contribute to a cleaner working environment, enhancing employee health and safety. The system is particularly valuable in power plants and cement factories, where large quantities of fly ash are generated daily. It also supports sustainable practices by facilitating the reuse of fly ash in construction materials, reducing the need for virgin raw materials. The HeadPowder Engineering Co., Ltd. system has been successfully deployed in numerous projects across China, demonstrating its effectiveness in meeting the demanding requirements of modern industrial facilities. Its combination of performance, reliability, and environmental compliance makes it a preferred choice for companies committed to operational excellence and environmental responsibility.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top