For businesses involved in the rice processing industry, efficient handling and conveying of rice powder is crucial for maintaining production efficiency and product quality. This article explores the working principles and key features of rice powder handling equipment, providing insights into how these systems operate and their advantages in industrial applications.
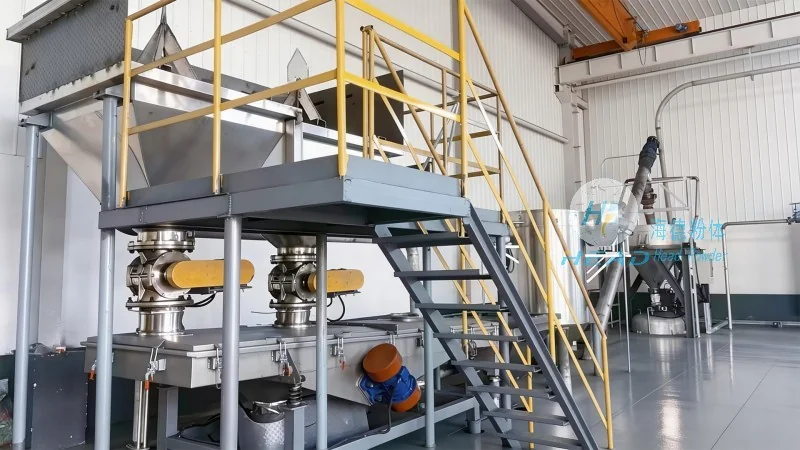
The core function of rice powder conveying equipment is to transport bulk rice powder from one location to another within a processing facility. These systems typically operate based on mechanical forces such as gravity, pressure, or vacuum, depending on the specific design and application requirements. Common mechanisms include screw conveyors, pneumatic conveyors, and bucket elevators, each tailored to handle the unique properties of rice powder, including its fine particle size and potential for dust generation.
For instance, screw conveyors utilize rotating screws to move rice powder along a trough, leveraging the friction between the screw and the material to achieve continuous transport. This method is particularly effective for horizontal or slightly inclined transport, offering a simple and reliable solution for moving bulk rice powder. In contrast, pneumatic conveyors employ air pressure to suspend and transport rice powder particles through a pipeline network. This approach is ideal for long-distance or vertical transport, as it can handle both fine and coarse powders while minimizing material degradation and contamination.
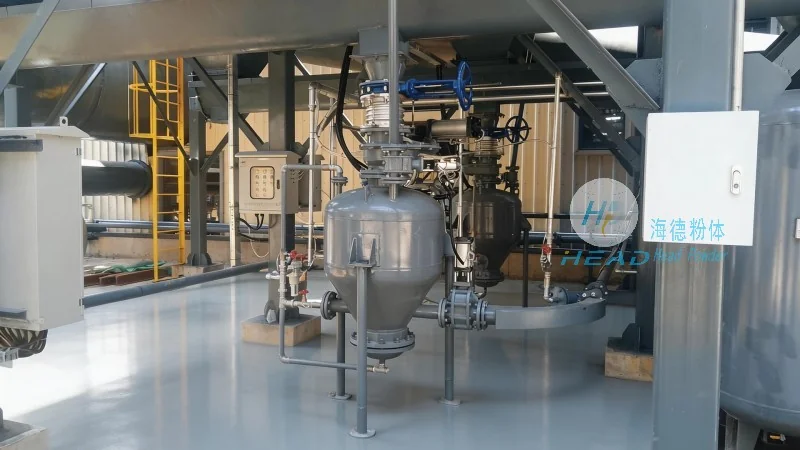
When evaluating rice powder conveying equipment, several key features should be considered to ensure optimal performance and suitability for specific applications. These features include material handling capacity, which determines the volume of rice powder that can be transported per unit time; system efficiency, measured by energy consumption and operational costs; and maintenance requirements, which impact long-term operational costs and downtime.
Another critical feature is the equipment's ability to handle the specific characteristics of rice powder, such as its moisture content, particle size distribution, and flowability. High-quality rice powder handling systems are designed to prevent agglomeration, caking, or segregation of particles, which can compromise product quality and processing efficiency. Additionally, features like dust control and explosion-proof design are essential for ensuring workplace safety, especially in environments where rice powder is prone to dust explosions.
Rice powder handling equipment is widely used in various stages of rice processing, from raw material storage and transport to finished product packaging. In the storage phase, conveyors help move rice powder from storage silos to processing lines, ensuring a steady supply of raw material. During processing, these systems facilitate the transfer of rice powder between different processing units, such as milling, grinding, and blending operations. Finally, in the packaging stage, conveyors can transport finished rice powder products to packaging lines, streamlining the overall production process.
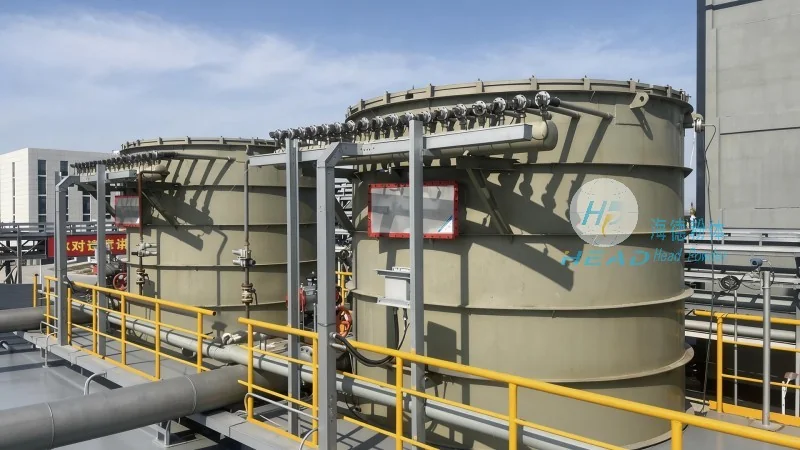
The adoption of advanced rice powder handling equipment offers several industry benefits, including improved production efficiency, reduced labor costs, and enhanced product quality. By automating the transport of rice powder, businesses can minimize manual handling, which reduces the risk of product contamination and human error. Additionally, efficient conveying systems help maintain consistent product quality by preventing segregation and ensuring uniform material flow throughout the processing line.
In summary, rice powder handling equipment plays a vital role in the rice processing industry by providing reliable and efficient methods for transporting bulk rice powder. Understanding the working principles and key features of these systems is essential for selecting the appropriate equipment for specific applications. By leveraging advanced technologies and design features, businesses can enhance their operational efficiency, reduce costs, and maintain high product quality in rice processing operations.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top