When it comes to the efficient handling and transportation of sugar powders in industrial settings, specialized equipment plays a crucial role. A sugar powder conveying machine is a vital component in the food processing and bulk material handling industries, designed to ensure the safe, reliable, and efficient movement of sugar from storage to processing or packaging stages. This article explores the fundamental aspects of such machines, focusing on their design principles and the technology behind their operation.
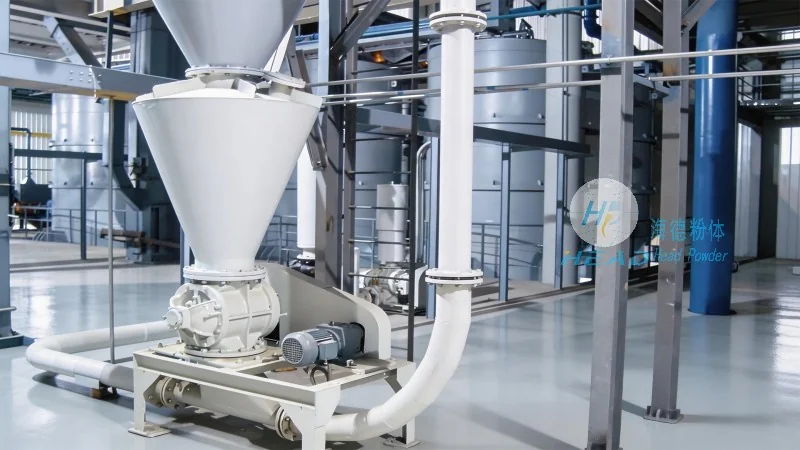
In the sugar industry, the need for efficient and hygienic material handling is paramount. Sugar powder conveying machines are engineered to address the unique challenges associated with transporting granular or powdered sugar, such as preventing caking, maintaining product integrity, and ensuring minimal dust generation. These machines are commonly used in sugar refineries, food processing plants, and other facilities where large volumes of sugar need to be moved between different stages of production. The primary function of a sugar powder conveying machine is to transport sugar from silos, hoppers, or storage containers to processing equipment, packaging lines, or other areas of the facility. By automating this process, these machines enhance operational efficiency, reduce labor costs, and improve overall productivity.
The design of a sugar powder conveying machine is based on several critical principles that ensure optimal performance and reliability. These principles include material handling efficiency, hygienic design, and energy efficiency. The machine's structure is typically designed to minimize the risk of product contamination and to facilitate easy cleaning and maintenance. Key components of a sugar powder conveying machine include the hopper, conveyor system (such as screw conveyors, pneumatic conveyors, or belt conveyors), and control systems. The choice of conveyor type depends on factors like the sugar's characteristics, the required conveying distance, and the desired flow rate. For example, screw conveyors are often used for horizontal or slight incline transport due to their ability to handle dry, free-flowing powders without the need for external air. Pneumatic conveyors, on the other hand, use air pressure to move sugar particles, making them suitable for longer distances or when precise control over the flow is required.
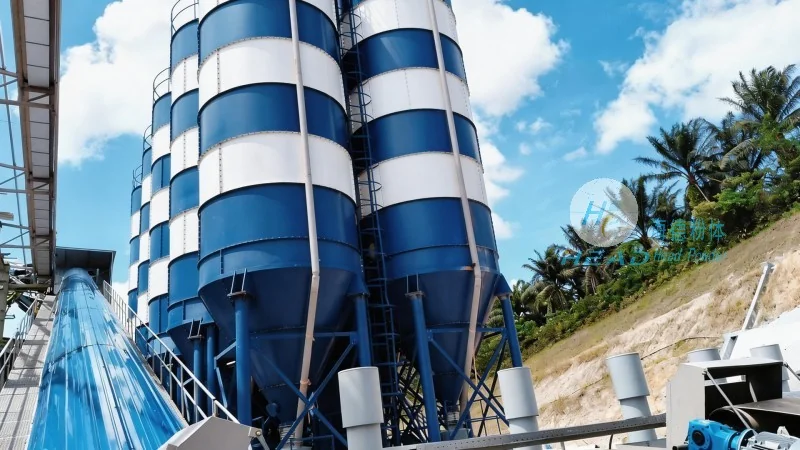
The operation of a sugar powder conveying machine involves a series of steps that ensure the smooth and continuous movement of sugar. The process typically begins with the sugar being fed into the hopper from a storage silo or bulk container. The hopper is designed to hold a sufficient quantity of sugar and to provide a controlled feed rate to the conveyor system. From the hopper, the sugar is transferred to the conveyor mechanism. In a screw conveyor, for instance, a rotating screw (or auger) pushes the sugar forward along the conveyor tube. The screw's pitch and speed are carefully engineered to maintain a consistent flow rate, preventing the sugar from clogging or sticking to the conveyor walls. In pneumatic conveyors, the sugar is suspended in a stream of air and transported through a pipeline. The air pressure and velocity are controlled to ensure the sugar particles move efficiently without damage. The conveying system then delivers the sugar to the next stage of the process, such as a mixer, grinder, or packaging machine. Control systems, often integrated with sensors and variable frequency drives, monitor the flow rate, pressure, and other parameters to maintain optimal performance and prevent system failures.
Implementing a sugar powder conveying machine offers several advantages for industrial operations. Firstly, these machines enhance operational efficiency by automating the material handling process, reducing the need for manual labor and minimizing downtime. By ensuring a consistent and controlled flow of sugar, they help maintain production schedules and improve overall throughput. Secondly, sugar powder conveying machines are designed with hygienic considerations in mind, making them suitable for food processing environments where product purity and safety are critical. The materials used in the construction of these machines, such as stainless steel and food-grade plastics, are resistant to corrosion and easy to clean, reducing the risk of contamination. Thirdly, these machines are energy-efficient, with designs that minimize power consumption while maximizing conveying capacity. The use of variable speed drives allows for adjustments based on the load, further reducing energy costs. Additionally, the compact design of many sugar powder conveying machines makes them suitable for installations with limited space, optimizing facility layout and utilization.
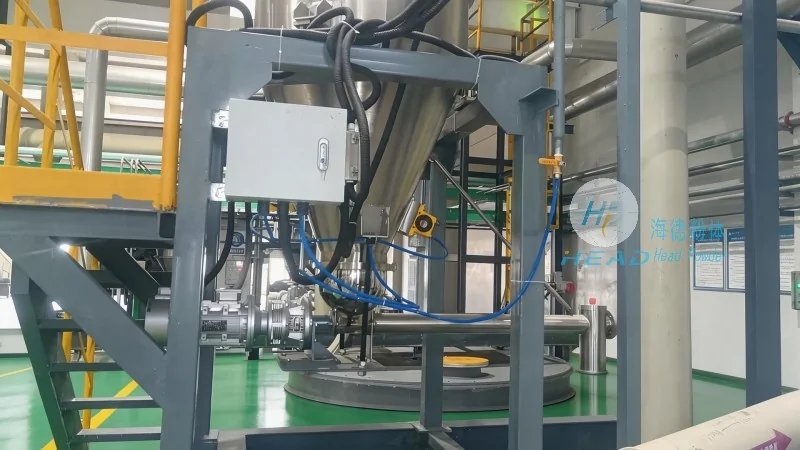
Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer of industrial conveying equipment, offers customized sugar powder conveying machines tailored to the specific needs of various industries. The company, based in Shandong, China, specializes in designing and manufacturing high-quality conveying systems that meet the stringent requirements of the food processing and bulk material handling sectors. Their products are engineered to handle different types of sugar, including granulated, powdered, and crystalline forms, ensuring versatility and adaptability. The company's design team works closely with clients to understand their operational requirements, such as conveying distance, flow rate, and environmental conditions, and develops solutions that optimize performance and reliability. For example, a client in a sugar refinery might require a large-capacity screw conveyor with a high flow rate to handle bulk sugar from storage to processing. Shandong HeadPowder Engineering Co., Ltd. would design a custom machine with appropriate screw dimensions, speed, and material of construction to meet these specifications. Similarly, a food processing plant might need a pneumatic conveyor for transporting sugar to a packaging line, and the company would provide a system with precise air pressure control and dust collection features to ensure compliance with hygiene standards.
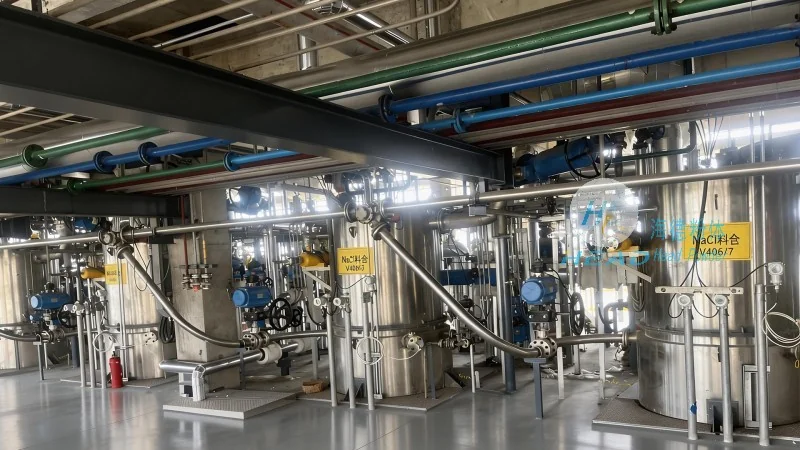
Proper maintenance is essential to ensure the long-term performance and reliability of a sugar powder conveying machine. Regular maintenance tasks include cleaning the hopper and conveyor system to prevent sugar buildup and clogging, inspecting the conveyor components for wear and tear, and checking the control systems for proper operation. The use of high-quality materials, such as stainless steel and food-grade plastics, helps extend the lifespan of the machine and reduces the need for frequent repairs. Shandong HeadPowder Engineering Co., Ltd. provides comprehensive maintenance services and spare parts for their products, ensuring that clients can keep their equipment in optimal condition. The company's technical support team offers guidance on maintenance procedures and can provide advice on best practices for operating and maintaining sugar powder conveying machines. By following recommended maintenance schedules and using genuine spare parts, users can maximize the operational life of their equipment and minimize downtime.
Sugar powder conveying machines are essential equipment in the sugar industry, designed to efficiently and hygienically transport sugar powders between different stages of production. The design principles behind these machines focus on material handling efficiency, hygienic design, and energy efficiency, ensuring optimal performance and reliability. With the right design and maintenance, these machines can significantly enhance operational efficiency and productivity in industrial settings. Shandong HeadPowder Engineering Co., Ltd., with its expertise in industrial conveying equipment, provides high-quality sugar powder conveying machines tailored to the specific needs of various industries, helping clients achieve their production goals while maintaining product quality and safety.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top