Understanding the calcium hydroxide powder conveyor is essential for those working with this critical material in industrial settings. This equipment is specifically designed to handle the transportation of calcium hydroxide powder, a substance widely used in various applications such as construction, chemical processing, and environmental remediation. The efficient and safe handling of this powder is crucial due to its properties, including its fine particle size and potential for dust generation. A well-designed conveyor system not only ensures smooth material flow but also maintains operational safety and environmental compliance.
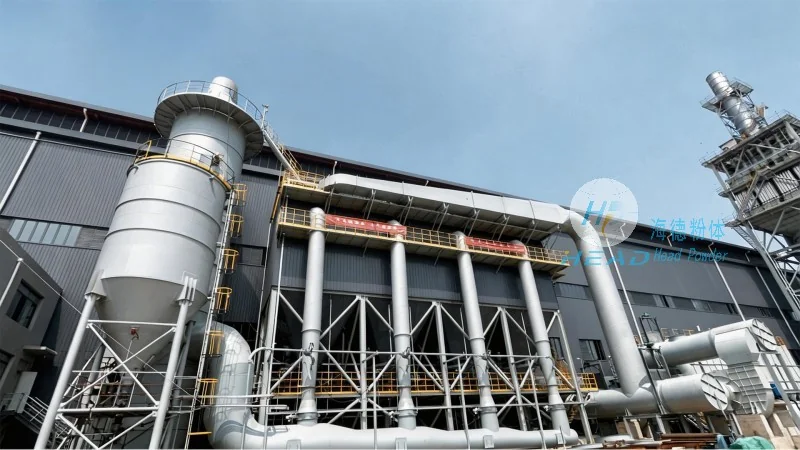
HeadPowder, a leading manufacturer based in Shandong, China, specializes in the engineering and production of advanced powder handling equipment. With a strong commitment to quality and innovation, the company has developed state-of-the-art calcium hydroxide powder conveyors that meet the demanding requirements of modern industrial processes. The company's headquarters and operational base are located in Shandong, China, where they leverage local expertise and resources to deliver high-performance solutions tailored to customer needs. HeadPowder's focus on precision engineering ensures that their conveyor systems are built to handle the unique characteristics of calcium hydroxide powder, providing reliable performance and durability in challenging environments.
The design of a calcium hydroxide powder conveyor is based on several key principles that address the specific challenges associated with this material. First, the system must be capable of handling fine, cohesive powders without clogging or blockages. This is achieved through the use of specialized components such as flexible hoses, rotary valves, and airlock feeders that maintain consistent material flow. The conveyor's structure is typically designed with smooth, non-stick surfaces to prevent powder buildup and ensure easy cleaning. Additionally, the system incorporates dust control measures, including sealed enclosures and filtration systems, to minimize airborne dust and protect both the environment and personnel. The design also emphasizes energy efficiency, with options for variable speed drives and optimized airflow to reduce operational costs while maintaining performance.
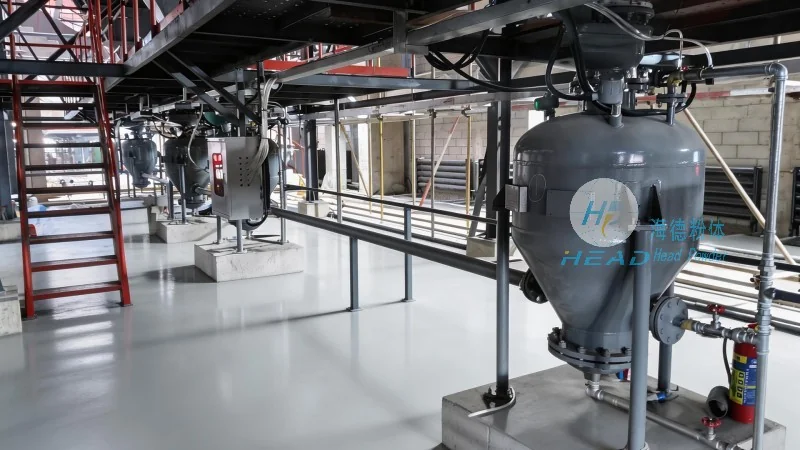
Several critical components work together to ensure the effective operation of a calcium hydroxide powder conveyor. The primary components include the feeding hopper, which collects and stores the powder before it is transferred to the conveyor line. The hopper is designed with a sloped bottom to facilitate material flow and prevent agglomeration. The conveyor itself, often a pneumatic or mechanical system, transports the powder from the hopper to the discharge point. For pneumatic conveyors, the system uses compressed air to create a flow of powder through a pipeline, while mechanical conveyors rely on rotating screws or belts to move the material. The discharge unit, such as a rotary valve or a controlled outlet, regulates the release of the powder to the next stage of the process. Each component is carefully selected and integrated to ensure seamless operation and minimal downtime. The materials used in the construction of these components are chosen for their resistance to corrosion and wear, as calcium hydroxide can be abrasive and reactive with certain metals.
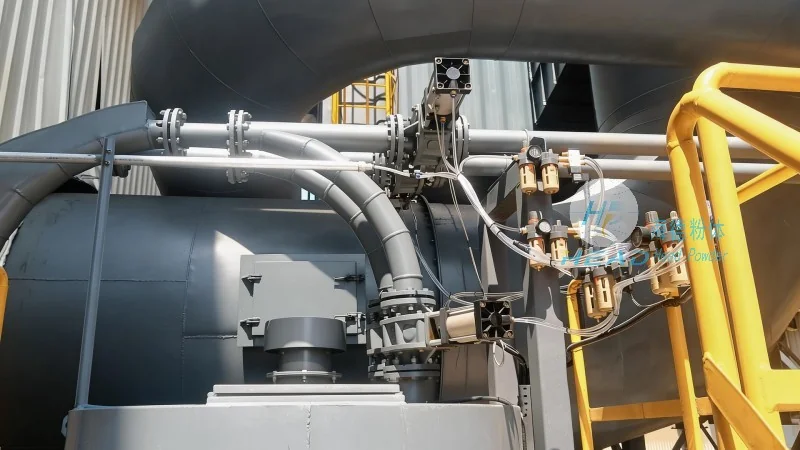
Implementing a calcium hydroxide powder conveyor offers numerous advantages for industrial operations. One of the most significant benefits is the improvement in material handling efficiency. By automating the transportation process, the conveyor reduces manual labor and minimizes the risk of human error, leading to higher productivity and consistent output. The system also enhances safety by containing the powder within a sealed environment, reducing exposure to dust and preventing accidental spills. This not only protects workers but also helps in maintaining compliance with environmental regulations. Additionally, the conveyor's design allows for precise control over the flow rate, enabling better process control and reducing waste. The energy-efficient operation of the conveyor contributes to lower operational costs over time, making it a cost-effective solution for long-term use. Furthermore, the durability and reliability of the equipment ensure minimal maintenance and extended service life, providing a strong return on investment for businesses.
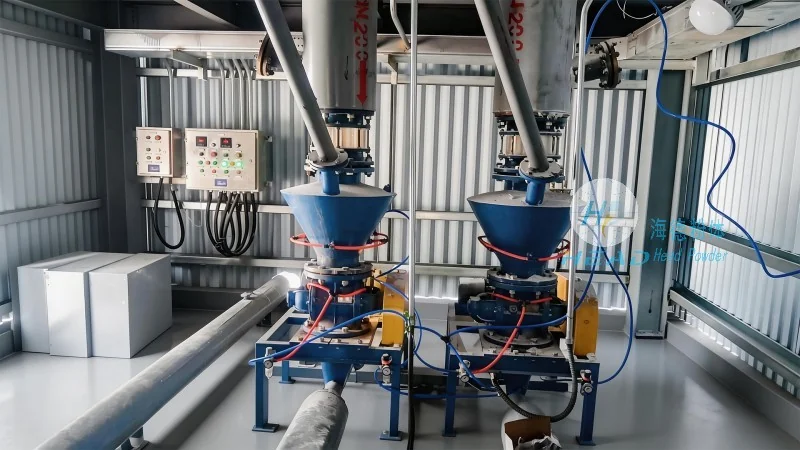
Calcium hydroxide powder conveyors are widely used across various industries due to the versatility of calcium hydroxide. In the construction industry, the material is used as a component in cement and concrete production, and the conveyor ensures that it is delivered to mixing plants efficiently. The chemical industry utilizes calcium hydroxide in the production of other chemicals, and the conveyor facilitates the transfer of the powder between processing stages. Environmental remediation projects also rely on calcium hydroxide to neutralize acidic soils and water, and the conveyor system helps in the distribution of the material to treatment sites. Other applications include the food industry, where calcium hydroxide is used as a food additive, and the pharmaceutical industry, where it is incorporated into various formulations. In each of these applications, the conveyor plays a vital role in ensuring that the material is handled safely and effectively, supporting the overall success of the operations.
Proper maintenance and operational considerations are essential to maximize the performance and lifespan of a calcium hydroxide powder conveyor. Regular inspection of components such as hoses, valves, and bearings is necessary to identify and address any potential issues before they lead to system failure. Cleaning the conveyor system after each use is crucial to remove any residual powder that could cause clogging or contamination. The use of appropriate lubricants and filters helps maintain the efficiency of moving parts and prevents dust accumulation. Operational parameters, such as air pressure and flow rate, should be monitored and adjusted as needed to optimize performance. Training operators on the proper use and maintenance of the conveyor is also important to ensure safe and effective operation. By following these guidelines, businesses can ensure that their calcium hydroxide powder conveyor operates at peak efficiency, reducing downtime and maintenance costs while maintaining high standards of safety and quality.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top