HeadPowder, a leading manufacturer based in Shandong, China, specializes in the design and production of advanced pneumatic conveying systems tailored for the cement and aggregate industries. The cement aggregate pneumatic conveying system is a critical piece of equipment that efficiently transports bulk materials like cement, sand, gravel, and other aggregates from one location to another within industrial facilities. This system operates by utilizing compressed air or vacuum to move materials through a network of pipes, eliminating the need for traditional mechanical conveyors such as belt conveyors or screw conveyors. The technology behind this system is based on the principles of fluidization and particle transport, ensuring a smooth and reliable material handling process.
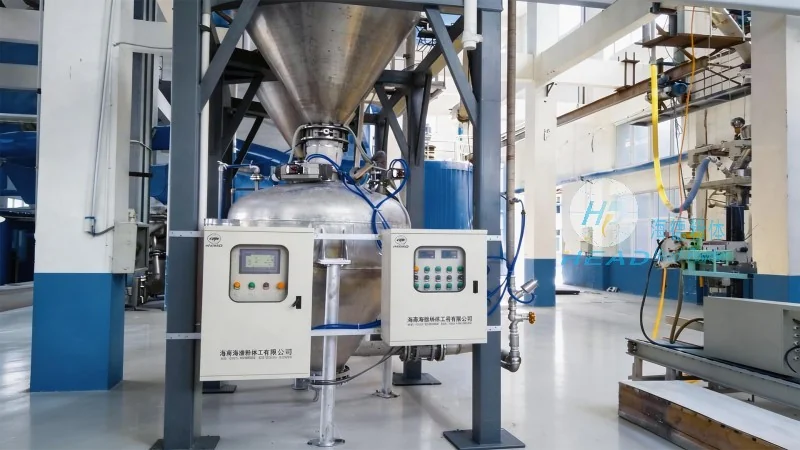
The core principle of the cement aggregate pneumatic conveying system is to create a flow of air that can carry the solid particles through the conveying lines. There are two main types of pneumatic conveying systems: positive pressure and negative pressure. In a positive pressure system, high-pressure air is introduced at the material inlet, pushing the particles forward through the pipeline. The air velocity is maintained above the minimum fluidization velocity to keep the particles suspended and prevent them from settling. On the other hand, a negative pressure system draws the material into the pipeline using a vacuum at the discharge end, pulling the particles along. Both systems rely on the balance between air pressure and particle density to achieve efficient transport. The system typically includes components such as a material hopper, a feeder, a conveying line, a filter, and a receiver. The feeder controls the flow rate of the material into the system, while the filter ensures that the air leaving the system is clean and free from dust. The receiver collects the conveyed material at the destination point.
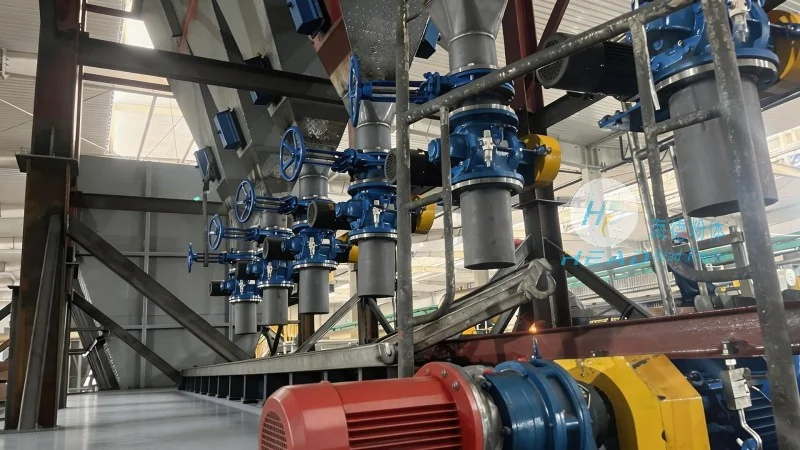
The cement aggregate pneumatic conveying system is widely used in various industrial applications, particularly in the cement production and construction material processing sectors. Its working scene characteristics are tailored to meet the specific demands of different environments and material types. For instance, in a cement plant, the system is used to transport raw materials like limestone, clay, and sand from storage silos to the grinding mills. The system's ability to handle fine powders and bulk aggregates with minimal dust generation makes it ideal for such applications. In aggregate processing plants, the system efficiently transports sand, gravel, and crushed stone from stockpiles to the mixing and batching areas. The system's flexibility allows it to be integrated into existing production lines, reducing downtime and improving overall operational efficiency. Additionally, the system is suitable for applications where long-distance transport is required, as it can cover distances of several hundred meters without significant loss of material or air pressure. The working scene also includes considerations for material compatibility, such as the prevention of material degradation or caking during transport, which is achieved through proper air velocity control and system design. The system's reliability and low maintenance requirements make it a preferred choice for continuous production environments, ensuring consistent material flow and minimizing operational disruptions.
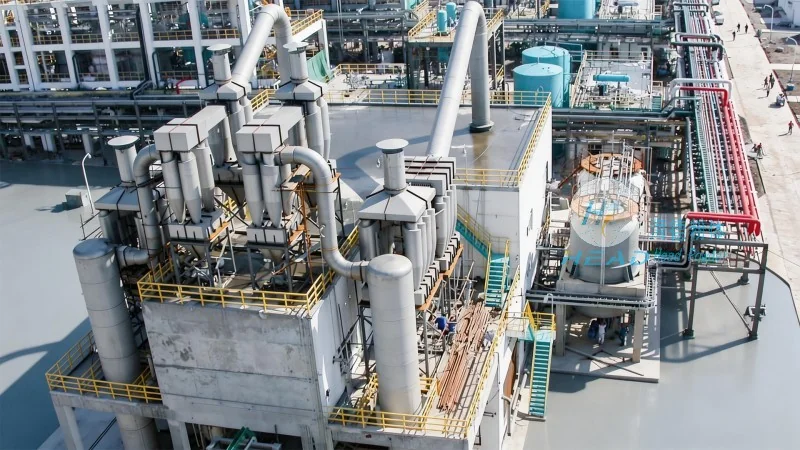
HeadPowder's cement aggregate pneumatic conveying system offers several advantages over traditional material handling methods. The primary benefit is the reduction in labor costs and operational complexity, as the system automates the material transport process. Unlike mechanical conveyors, which require regular maintenance and cleaning, the pneumatic system has fewer moving parts and is less prone to blockages. The system also provides better control over material flow, allowing for precise dosing and batching. This is particularly important in cement production, where accurate material proportions are critical for achieving the desired product quality. The system's ability to handle a wide range of materials, from fine powders to coarse aggregates, makes it versatile for various industrial applications. Furthermore, the system contributes to a cleaner working environment by containing dust and preventing material spillage. In construction material processing plants, the system enhances productivity by enabling faster and more efficient material transfer, which in turn improves the overall production output. The system's scalability allows it to be customized to meet the specific needs of different facilities, whether it's a small-scale operation or a large industrial plant. HeadPowder's expertise in designing and manufacturing these systems ensures that clients receive equipment that is tailored to their unique requirements, providing long-term performance and reliability.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top