Shandong HeadPowder Engineering Co., Ltd., a leading enterprise in the field of powder processing and conveying technology, specializes in the design, manufacturing, and application of advanced pneumatic conveying systems. This article focuses on the fundamental principles and operational characteristics of equipment used for the pneumatic transport of ammonium bicarbonate, a key chemical widely utilized in agriculture and industrial applications.
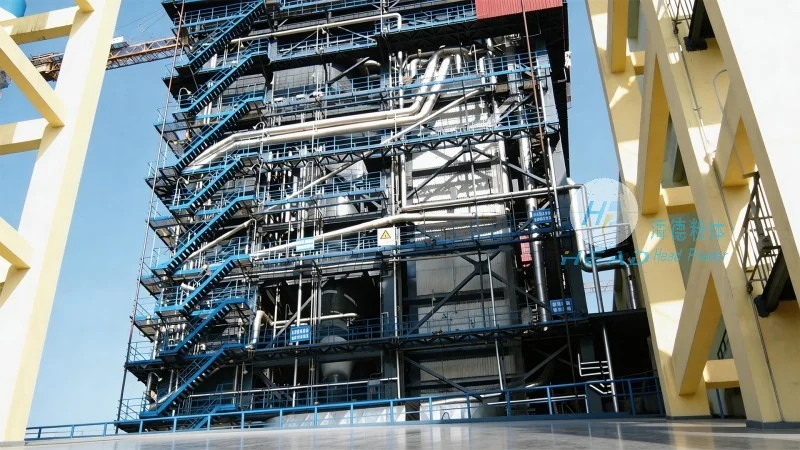
Pneumatic conveying systems utilize air or gas as the medium to transport bulk materials like ammonium bicarbonate. The core mechanism involves creating a pressure differential between the inlet and outlet of the system. In a typical setup, air is drawn into the conveying line, and the ammonium bicarbonate is introduced into the air stream. The air flow then carries the powder particles through the pipeline, ensuring efficient and continuous transport. This method offers several advantages over traditional mechanical conveying, including reduced equipment wear, lower maintenance costs, and the ability to handle materials that are prone to dust or caking.
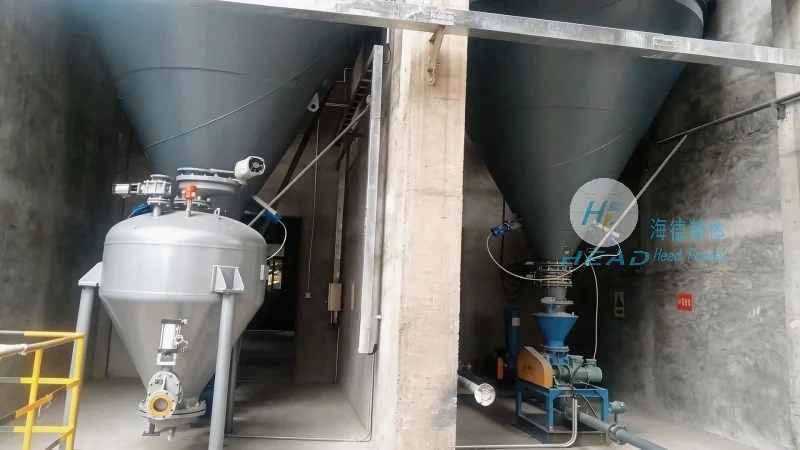
The operational characteristics of these systems are tailored to the specific demands of ammonium bicarbonate handling. Key aspects include the system's ability to maintain consistent flow rates, which is crucial for maintaining product quality and preventing clogging. The design also considers the material's hygroscopic nature, ensuring that the conveying process does not lead to moisture absorption or degradation. Additionally, the systems are engineered to minimize dust emissions, adhering to environmental regulations and ensuring workplace safety. The flexibility of the pneumatic conveying system allows for integration with existing production lines, making it a cost-effective solution for both new installations and retrofit projects.
Ammonium bicarbonate is commonly used as a nitrogen fertilizer in agricultural settings, and the pneumatic conveying systems from Shandong HeadPowder Engineering Co., Ltd. are specifically designed to handle this application. The systems are capable of transporting large volumes of ammonium bicarbonate from storage silos to processing facilities or directly to application sites, ensuring efficient supply chain management. In industrial applications, such as chemical manufacturing, the systems help in the seamless transfer of raw materials, contributing to streamlined production processes. The reliability of the equipment, with its robust construction and advanced control systems, ensures minimal downtime and consistent performance, which are critical for maintaining production efficiency.
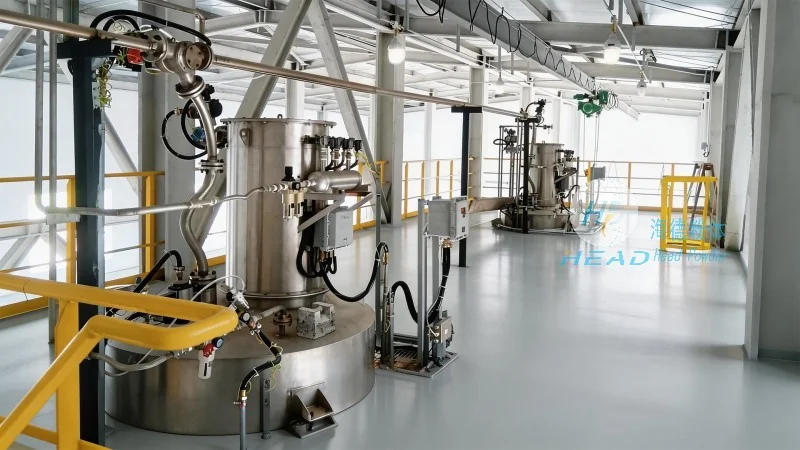
Shandong HeadPowder Engineering Co., Ltd. provides comprehensive solutions for ammonium bicarbonate pneumatic conveying, combining advanced technology with practical application expertise. The company's systems are designed to meet the unique requirements of the material, ensuring efficient, safe, and cost-effective transport. With a focus on quality and customer satisfaction, HeadPowder has established itself as a trusted partner in the powder handling industry, serving clients across China and beyond.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top