Shandong HeadPowder Engineering Co., Ltd., a leading enterprise based in Shandong, China, specializes in the design and manufacturing of advanced powder handling solutions. The fully automatic weighing powder conveying system is a sophisticated piece of equipment engineered to handle bulk powders with precision and efficiency. This system integrates weighing technology with material transport mechanisms, ensuring accurate measurement and controlled delivery of powders in various industrial applications.
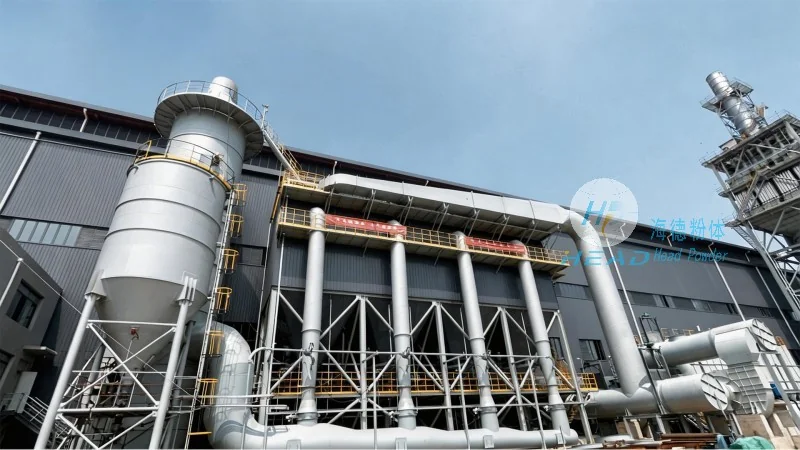
The fundamental principle of the fully automatic weighing powder conveying system revolves around the integration of high-precision load cells and advanced control systems. The system operates by continuously monitoring the weight of the material being conveyed, adjusting the feed rate in real-time to maintain the desired weight. This closed-loop control mechanism minimizes material loss and ensures consistent product quality. The load cells, typically equipped with strain gauges, convert the mechanical force of the powder into an electrical signal, which is then processed by the control unit to regulate the conveyor speed or feeding mechanism. This precise measurement capability is crucial for applications where accuracy in dosage or batch composition is critical, such as in pharmaceutical manufacturing or food processing.
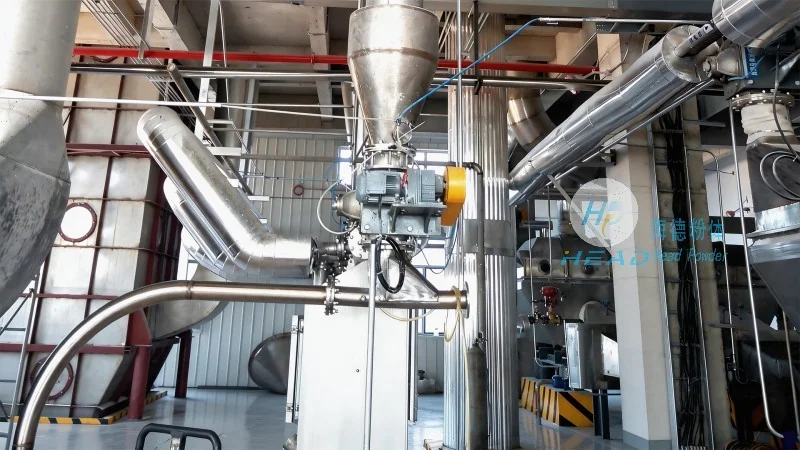
The fully automatic weighing powder conveying system comprises several key components, each playing a vital role in the overall operation. The primary components include the hopper or storage silo, which holds the bulk powder; the conveyor system, which transports the material from the storage to the weighing zone; the load cells or weighing sensors, which provide real-time weight data; the control unit, which processes the data and adjusts the system parameters; and the discharge mechanism, which delivers the material to the next processing stage. The hopper is designed with smooth, non-stick surfaces to prevent powder accumulation and ensure uniform flow. The conveyor system may use screw conveyors, belt conveyors, or pneumatic systems, depending on the material properties and application requirements. The load cells are strategically placed at critical points to capture accurate weight measurements, often with multiple sensors for redundancy and enhanced accuracy. The control unit, typically a programmable logic controller (PLC) or a dedicated weighing controller, uses algorithms to calculate the required feed rate and adjust the conveyor speed or feeding valve opening accordingly. This closed-loop feedback ensures that the actual weight matches the setpoint, minimizing deviations and improving process reliability.
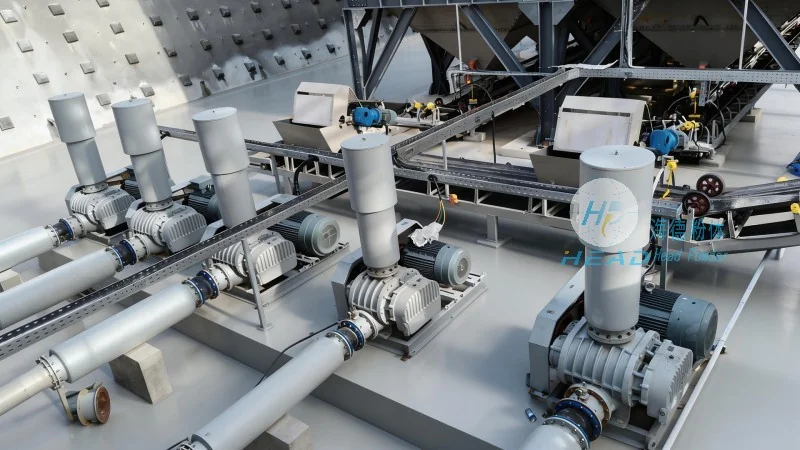
The fully automatic weighing powder conveying system is widely used in diverse industrial sectors, each presenting unique challenges and requirements. In the pharmaceutical industry, for example, the system is employed to handle active pharmaceutical ingredients (APIs) and excipients with high precision, ensuring that each batch meets stringent quality and dosage standards. The system's ability to maintain consistent weight and prevent cross-contamination is particularly valuable in this sector. In the chemical industry, the system is used for transporting raw materials and intermediates, where accurate measurement is essential for chemical reactions and process control. The system's robust design and ability to handle corrosive or abrasive materials make it suitable for these applications. The food and beverage industry also benefits from this technology, as it ensures the accurate dosing of ingredients in food products, such as spices, flavors, and preservatives. The system's hygienic design and easy cleaning features are critical in food processing environments, where compliance with food safety regulations is paramount. Additionally, in the agricultural sector, the system can be used for handling fertilizers and pesticides, where precise application rates are necessary for optimal crop yield and environmental protection.
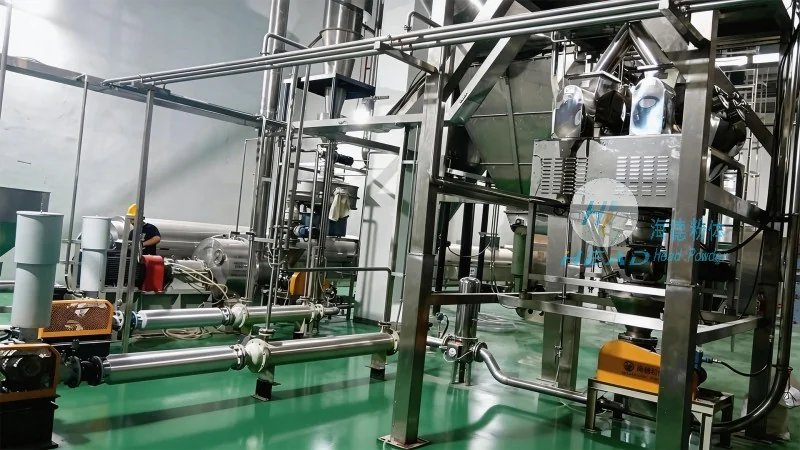
Implementing a fully automatic weighing powder conveying system offers numerous advantages over traditional manual or semi-automated methods. The primary benefit is the significant improvement in measurement accuracy, which reduces material waste and ensures consistent product quality. This accuracy is particularly important in industries where even small deviations can lead to product recalls or financial losses. Another key advantage is the enhanced operational efficiency. The system's automatic control reduces the need for manual intervention, allowing operators to focus on other critical tasks. This leads to increased productivity and reduced labor costs. The system also improves safety by minimizing the risk of overfilling or underfilling, which can cause equipment damage or product contamination. Furthermore, the system's ability to handle a wide range of powder types, from fine powders to bulk materials, makes it versatile and adaptable to various applications. The closed-loop control system provides real-time monitoring and adjustment, enabling quick response to changes in material flow or system performance. This adaptability is crucial in dynamic industrial environments where process conditions may vary. The system's durability and low maintenance requirements also contribute to long-term cost savings, as it reduces downtime and maintenance expenses.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top