Efficient bulk material conveying is a critical component in modern grain storage operations, ensuring the smooth transfer of grains and other powders within silos. The principles and operational characteristics of these systems are designed to optimize performance, reliability, and safety in diverse agricultural and industrial settings.
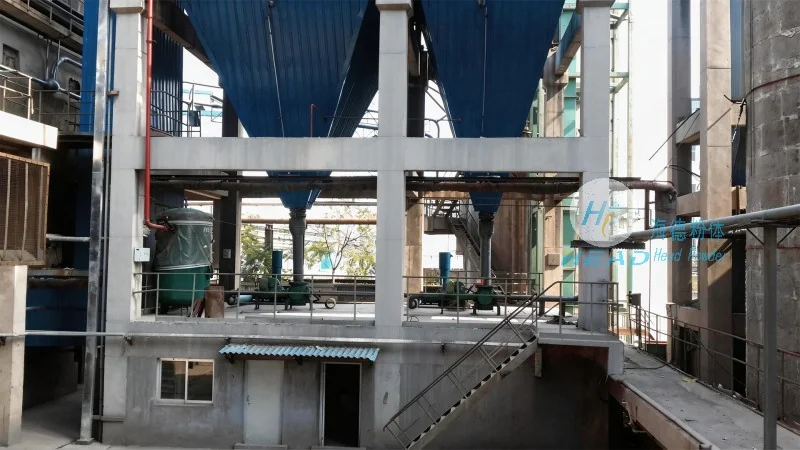
The core of grain silo conveying systems lies in the mechanics of transporting bulk materials through a network of pipes, hoppers, and control mechanisms. Common methods include pneumatic (air-assisted) and mechanical (belt, screw, or bucket) conveyors. Pneumatic systems utilize compressed air to create a flow of material, while mechanical systems rely on rotating components to move the product. Both approaches are engineered to handle varying particle sizes, densities, and moisture levels, ensuring consistent and efficient transfer.
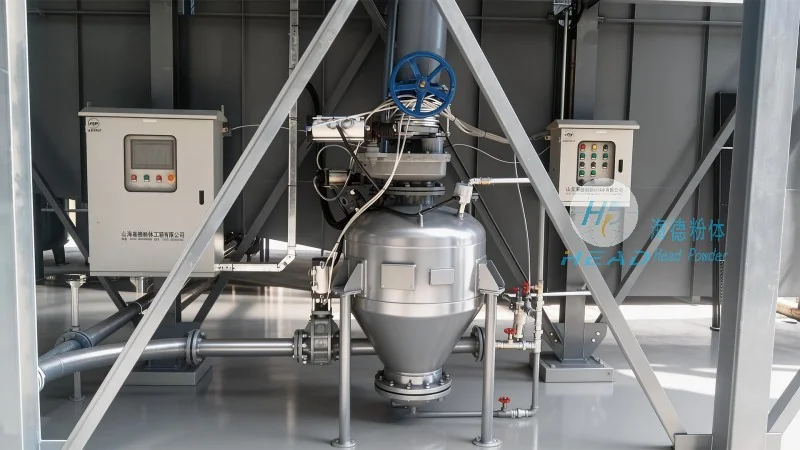
Grain silo conveying applications exhibit distinct characteristics based on the scale of the facility, the type of grain being handled, and the operational requirements. For large-scale storage facilities, continuous conveying systems are preferred to maintain steady throughput, minimizing downtime and maximizing storage capacity utilization. In contrast, smaller operations may employ batch or intermittent conveying for more flexible handling of different grain varieties. Environmental factors such as temperature fluctuations and humidity also influence system design, as materials can become sticky or clumpy under certain conditions, requiring specialized equipment to prevent blockages and ensure smooth operation.
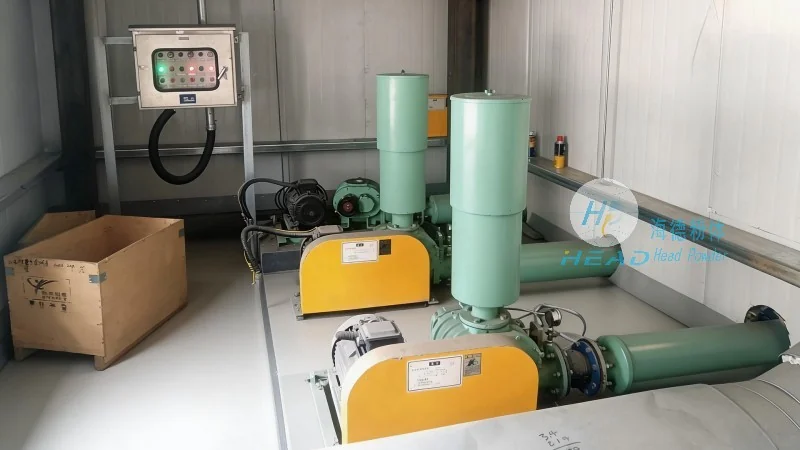
Typical bulk conveying systems in grain silos consist of several key components: a hopper or bin for material storage, a conveyor unit (either pneumatic or mechanical), a control panel for monitoring and adjusting flow rates, and a discharge outlet for delivering the material to processing or storage areas. The control panel plays a vital role in regulating the system, allowing operators to adjust air pressure, motor speed, or conveyor speed to match the specific needs of the operation. This adaptability ensures that the system can handle a wide range of materials, from fine powders like flour to larger grains like corn, without compromising performance.
Shandong HeadPowder Engineering Co., Ltd., a leading provider of bulk material handling solutions, specializes in designing and manufacturing customized conveying systems tailored to the unique demands of grain storage facilities. With a focus on reliability and efficiency, their products are engineered to meet the rigorous standards of agricultural operations, ensuring consistent performance over extended periods. The company’s expertise in material science and mechanical engineering allows them to develop systems that address the specific challenges of different grain types and operational environments, providing clients with durable and cost-effective solutions.
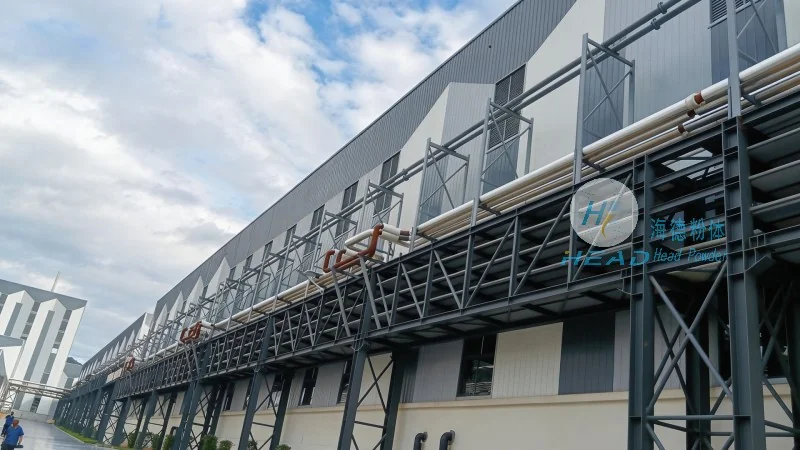
The working scene characteristics of bulk material conveying in grain silos are directly influenced by the operational scale and the type of grain being processed. For instance, in large commercial grain elevators, high-capacity pneumatic conveyors are used to transport thousands of tons of grain per day, while in smaller farm silos, mechanical screw conveyors may be more appropriate for handling smaller volumes of diverse grain varieties. The adaptability of these systems is crucial, as they must be able to handle changes in grain quality, such as variations in moisture content or particle size, without requiring extensive modifications. This flexibility ensures that grain storage operations can maintain efficiency and productivity, even under varying conditions.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top