HeadPowder, or Shandong HeadPowder Engineering Co., Ltd., is a professional manufacturer based in Shandong, China, specializing in the design, development, and production of advanced powder handling solutions. The company focuses on providing efficient and reliable systems for the transportation of various powders using negative pressure vacuum technology.
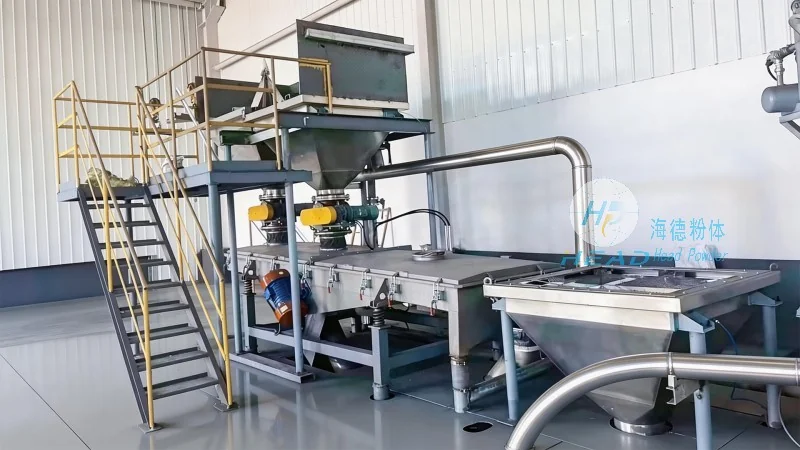
Negative pressure vacuum powder transport operates on the fundamental principle of creating a pressure differential between the powder source and the receiving container. By generating a lower pressure (vacuum) in the transport system, the surrounding atmospheric pressure pushes the powder particles into the vacuum chamber. This process is achieved through a series of components, including a vacuum pump, a transport pipeline, and a dust collection system. The vacuum pump draws air and powder particles from the source, while the pipeline conveys the material to the destination. The system ensures that the powder is moved without the need for mechanical agitation or external force, reducing the risk of material degradation and contamination.
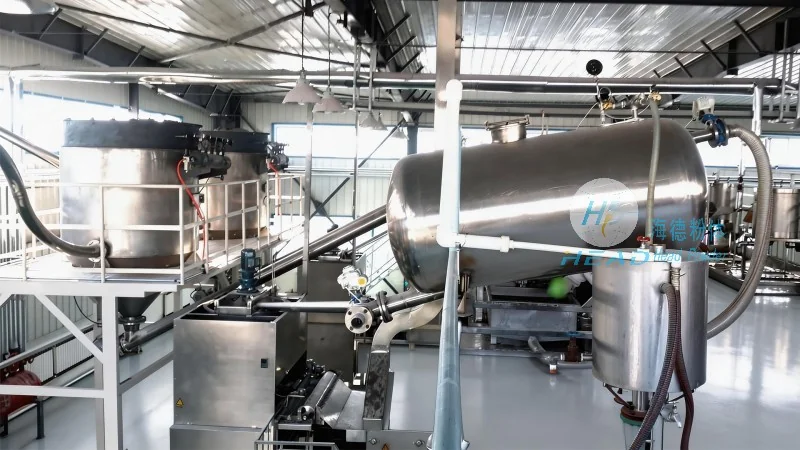
The negative pressure vacuum powder transport system offers several advantages that make it suitable for diverse industrial applications. One of the primary benefits is its ability to handle a wide range of powder types, from fine powders like pharmaceuticals and chemicals to bulk materials such as cement and food products. The system's gentle handling minimizes particle breakage and agglomeration, preserving the quality and integrity of the material. Additionally, the enclosed design prevents dust emissions, ensuring compliance with environmental regulations and maintaining a clean working environment. This feature is particularly important in industries where dust control is critical, such as pharmaceutical manufacturing, food processing, and chemical processing.
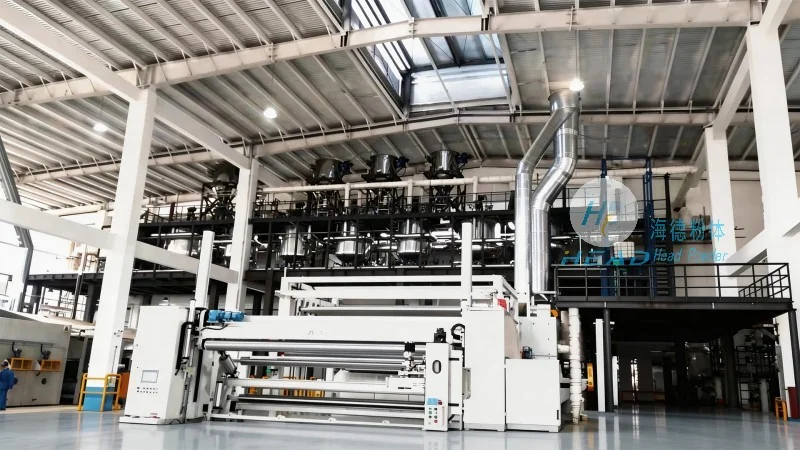
HeadPowder's negative pressure vacuum transport systems are widely used in various sectors. In the pharmaceutical industry, the system is employed to transport active pharmaceutical ingredients (APIs) and excipients with high precision, ensuring that the powders are handled under sterile conditions. The gentle transport process reduces the risk of contamination and maintains the stability of the product. In the chemical industry, the system is used to handle reactive powders and hazardous materials, providing a safe and controlled method of transportation. The ability to operate under negative pressure also helps in preventing the release of harmful fumes or dust into the environment. In the food and beverage industry, the system is utilized for transporting ingredients like flour, sugar, and spices, maintaining the freshness and quality of the products. The enclosed system also prevents cross-contamination, which is essential in food processing facilities.
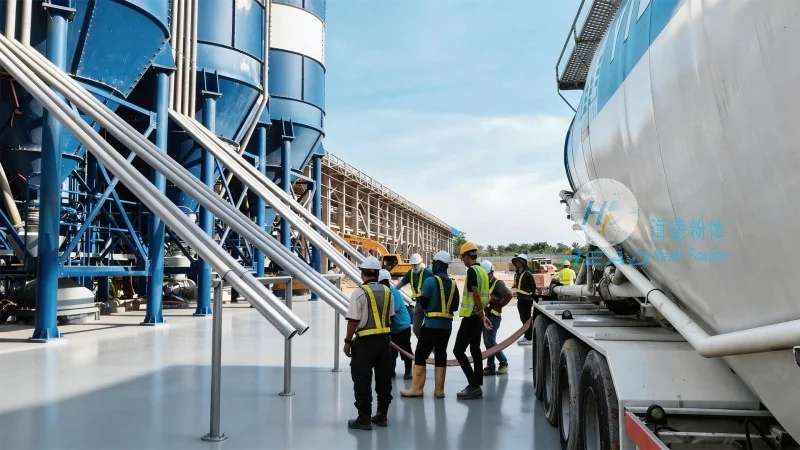
Compared to traditional powder transport methods like pneumatic conveying or mechanical conveying, negative pressure vacuum transport offers several advantages. Traditional methods often require high pressure and can cause particle degradation due to high velocity and turbulence. In contrast, the negative pressure system operates at lower velocities, reducing the risk of particle breakage and maintaining the material's original properties. The system also provides better control over the flow rate, allowing for precise dosing and dosing accuracy. Another advantage is the reduced energy consumption, as the vacuum pump operates at lower power levels compared to high-pressure compressors used in conventional systems. This results in lower operational costs and increased energy efficiency. Additionally, the system's enclosed design minimizes dust accumulation and the need for frequent cleaning, reducing maintenance time and costs.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top