HeadPowder, a leading engineering firm based in Shandong, China, specializes in the design and implementation of advanced pneumatic conveying systems tailored for the efficient bulk handling of cement, fly ash, and various mineral powders. This article explores the critical role of pneumatic conveying technology in modern industrial applications, highlighting the benefits and technical considerations for industries relying on these materials.
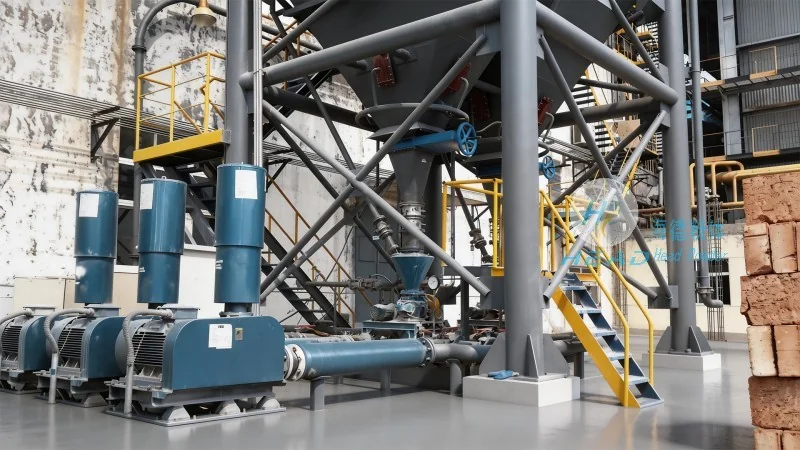
Pneumatic conveying, also known as air conveying, is a method of transporting bulk materials through a pipeline using a stream of air. Unlike traditional mechanical systems like belt conveyors or screw conveyors, pneumatic systems offer unique advantages in terms of flexibility, cleanliness, and the ability to handle a wide range of materials, including fine powders and abrasive substances. The core components of a pneumatic conveying system typically include a material feed hopper, a conveyor line, a control system, and an air supply unit. These components work in tandem to ensure the safe and efficient movement of materials from one location to another.
For industries dealing with cement, fly ash, and other mineral powders, pneumatic conveying systems provide several key benefits. First, they minimize material contamination and dust exposure, which is crucial for maintaining product quality and ensuring worker safety. Unlike mechanical systems that may generate friction and particle degradation, pneumatic systems use air to move materials, reducing the risk of product degradation and preserving the integrity of the powders. Second, these systems offer high throughput and flexibility in material handling. They can transport materials over long distances and adapt to varying production schedules without significant downtime. Additionally, pneumatic conveying systems are more compact and require less floor space compared to traditional bulk handling equipment, making them ideal for facilities with limited space.
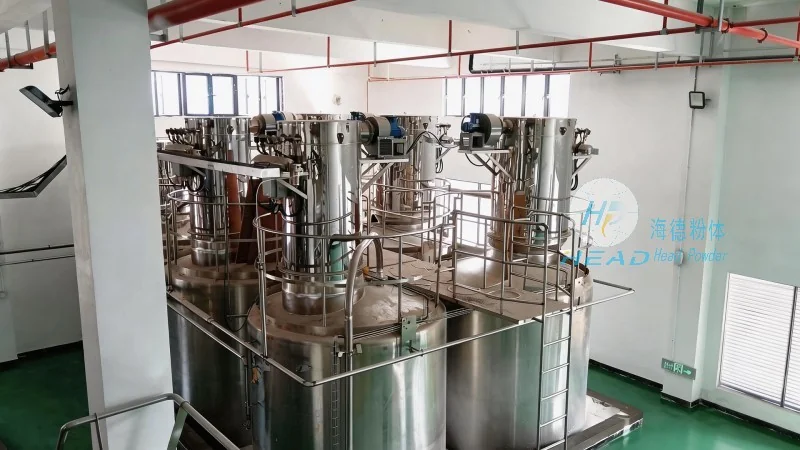
HeadPowder Engineering Co., Ltd. leverages cutting-edge technology and engineering expertise to design customized pneumatic conveying solutions that meet the specific needs of each client. The company’s engineers conduct thorough assessments of material properties, such as particle size, moisture content, and flow characteristics, to select the most appropriate conveying method—whether it be pressure or vacuum systems, or a combination of both. For example, pressure systems are often used for short to medium distances and high-volume applications, while vacuum systems are suitable for longer distances or when materials need to be collected from multiple points. HeadPowder also integrates advanced control systems that monitor pressure, flow rate, and material levels in real-time, ensuring optimal performance and preventing system failures.
Reliability is a top priority for HeadPowder when designing pneumatic conveying systems. The company uses high-quality materials and components, such as corrosion-resistant stainless steel for the conveyor lines and advanced air filtration systems to maintain air quality. Regular maintenance and performance monitoring are integral to the system’s lifecycle, ensuring that the equipment operates at peak efficiency and minimizes downtime. By focusing on durability and performance, HeadPowder’s systems provide long-term value to clients, reducing operational costs and improving overall productivity.
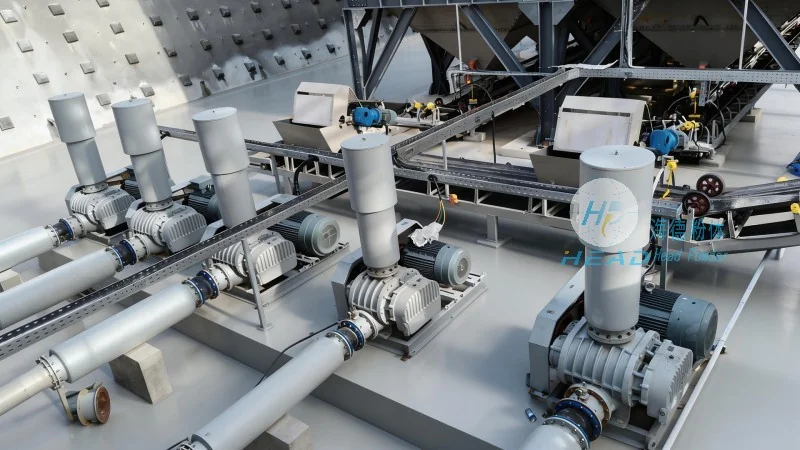
The effectiveness of pneumatic conveying systems is evident in various industrial applications. In cement production, these systems are used to transport raw materials from storage silos to the grinding mills, as well as to move finished cement products to storage or shipping facilities. For fly ash, a byproduct of coal combustion, pneumatic conveying enables its efficient collection and transportation to disposal or utilization sites, reducing environmental impact and optimizing resource recovery. Similarly, in mining and mineral processing industries, pneumatic systems facilitate the movement of fine mineral powders, such as silica or limestone, from processing plants to storage or downstream processing units.
As industries continue to demand more efficient and sustainable bulk material handling solutions, pneumatic conveying technology remains a cornerstone of modern engineering. HeadPowder Engineering Co., Ltd., with its expertise and commitment to innovation, plays a vital role in advancing these technologies for the cement, mineral, and related industries. By providing tailored, reliable, and efficient pneumatic conveying systems, HeadPowder helps clients enhance their operational performance, reduce costs, and meet the evolving demands of the market. The company’s presence in Shandong, China, underscores its position as a trusted partner in the global bulk handling industry.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top