Malting is a critical process in the production of beer and other malt-based beverages, involving the germination of barley to develop enzymes and other beneficial compounds. Efficient material handling is essential to maintain quality and productivity in malting operations. Air conveying systems offer a reliable and flexible method for transporting malting materials, such as raw barley, malt, and by-products, within the facility. This article explores several effective air conveying solutions tailored for malting applications, highlighting the benefits and considerations for each approach.
HeadPowder, or Shandong HeadPowder Engineering Co., Ltd., is a leading provider of specialized engineering solutions for the food and beverage industry. With a focus on innovation and customer-centric design, the company delivers high-quality equipment and systems that meet the unique demands of malting and other processing sectors. HeadPowder's expertise in material handling and process optimization ensures that their solutions are both efficient and durable, supporting long-term operational success for their clients. The company is based in Shandong, China, and serves a global market with tailored engineering services.
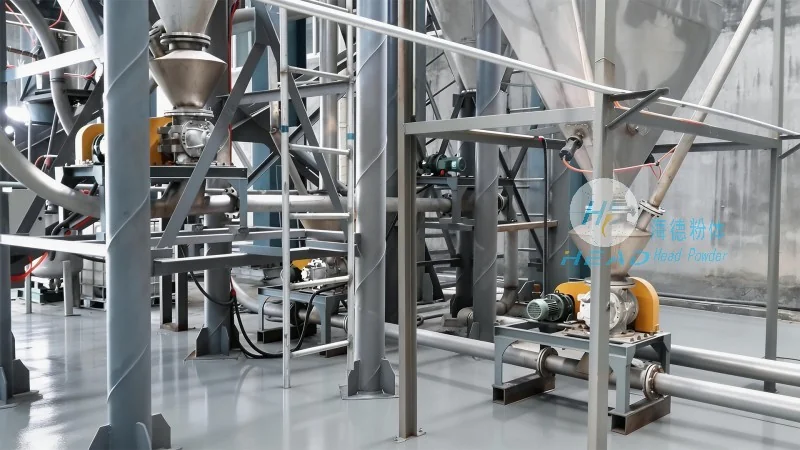
One of the most common air conveying solutions for malting is the positive pressure system. This method uses a blower or fan to generate air pressure within the system, which propels the material through a network of pipes. The positive pressure system is particularly effective for transporting fine powders and granular materials, such as malt flour or ground barley. It offers advantages like consistent material flow, reduced dust generation, and the ability to handle long conveying distances. The system typically includes a hopper for material storage, a rotary valve for controlled discharge, and a filter to capture any airborne particles. HeadPowder's positive pressure air conveying systems are designed with robust components to withstand the abrasive nature of malting materials, ensuring reliable performance over extended periods.
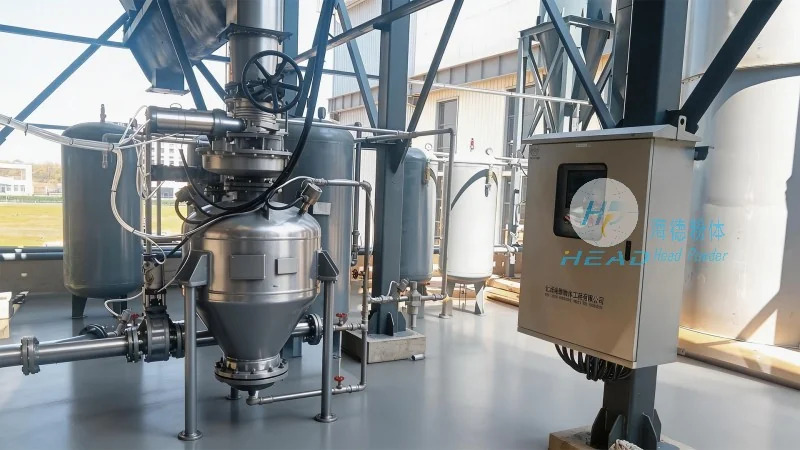
Another viable option is the negative pressure or suction system, which operates by creating a vacuum in the system to draw material from a source. This method is well-suited for applications where material needs to be collected from multiple points or transported over shorter distances. The negative pressure system is often preferred for handling bulk materials like whole barley or partially germinated malt, as it can efficiently capture and transport the material without the need for high air speeds. Key components include a vacuum pump, a collection hopper, and a filter to prevent dust from entering the system. HeadPowder's suction air conveying solutions are engineered to maintain consistent suction levels, minimizing the risk of material blockages and ensuring smooth operation. The system's design also allows for easy integration with existing malting equipment, making it a flexible choice for various processing needs.
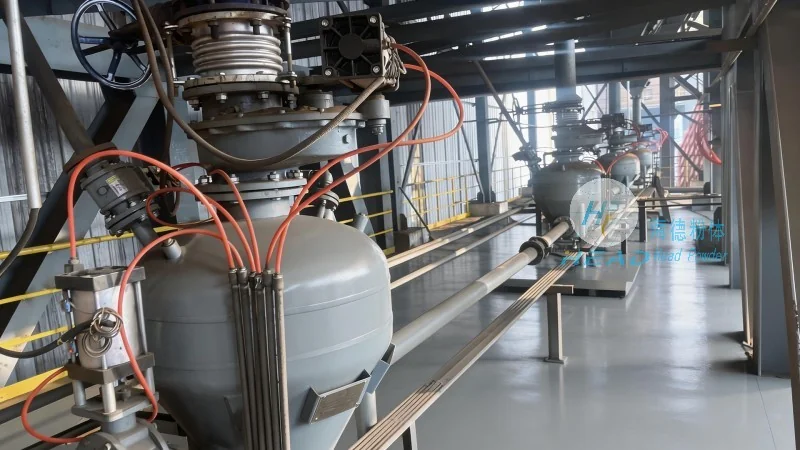
For more complex malting operations that require both material transport and collection from multiple locations, a combined positive and negative pressure system may be the optimal choice. This hybrid approach integrates elements of both positive and negative pressure systems to create a versatile material handling solution. The system can use positive pressure to transport material from a central source to a processing area, while negative pressure is employed to collect material from different points and return it to the main line. This configuration allows for efficient material flow in both directions, reducing the need for separate conveyors and minimizing energy consumption. HeadPowder's combined system is designed with advanced control technology to manage the pressure levels and material flow dynamically, ensuring optimal performance under varying operational conditions. The system's modular design enables easy expansion or modification as the malting facility grows, providing long-term adaptability.
When selecting an air conveying system for malting, several factors must be carefully evaluated to ensure the best fit for the specific application. Material characteristics, such as particle size, moisture content, and abrasiveness, play a crucial role in determining the appropriate system type and components. For example, fine malt powders may require a positive pressure system with a high-efficiency filter to prevent dust accumulation, while larger barley grains might benefit from a suction system with a robust hopper. The conveying distance and elevation changes also impact the system's design, as longer distances may necessitate additional blower capacity or intermediate collection points. Energy efficiency is another important consideration, as air conveying systems can consume significant power. HeadPowder's solutions are engineered with energy-saving features, such as variable speed drives and optimized pipe layouts, to minimize operational costs while maintaining performance. Additionally, the system's compatibility with existing infrastructure and the ease of maintenance are critical factors. HeadPowder provides comprehensive support, including installation, training, and ongoing maintenance services, to ensure that their air conveying systems operate at peak efficiency throughout their service life.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top