Capsule powder conveying systems are advanced mechanical solutions designed to efficiently transport and handle powder materials in various industrial applications. The core principle of these systems revolves around the use of specialized mechanisms to move powder through pipelines or enclosed pathways. Typically, the system operates by utilizing a combination of rotary or oscillating components that create a controlled flow of powder, ensuring minimal degradation and consistent delivery. The design often incorporates features such as air seals, anti-static measures, and precise control valves to maintain the integrity of the powder and prevent contamination. This approach allows for a reliable and efficient method of handling sensitive or high-value powder products, which is critical in industries like pharmaceuticals, food processing, and chemical manufacturing.
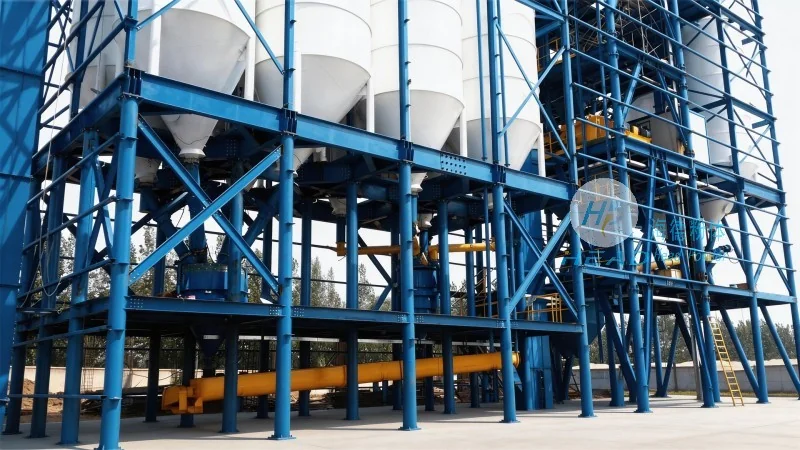
The operational characteristics of capsule powder conveying systems are tailored to meet the demands of diverse industrial environments. These systems are particularly effective in scenarios where precise control over powder flow is essential, such as in the production of capsules, granules, or other dosage forms. The ability to handle fine powders without agglomeration or segregation makes them suitable for applications requiring high purity and uniformity. Additionally, the systems are designed to operate in cleanroom environments, adhering to stringent hygiene standards, which is paramount in pharmaceutical and food industries. Their compact design and low maintenance requirements also make them ideal for space-constrained facilities or applications with limited operational downtime. By integrating advanced engineering principles, these systems provide a robust solution for continuous powder handling, enhancing productivity and reducing operational costs.
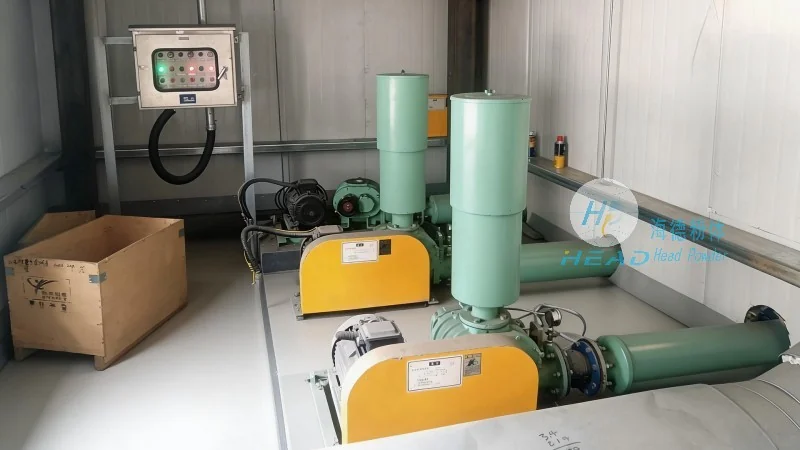
In the pharmaceutical industry, capsule powder conveying systems play a vital role in the production of oral dosage forms. The systems are used to transport raw materials, such as APIs (Active Pharmaceutical Ingredients) and excipients, from storage to processing units. The precise control over powder flow ensures that the correct proportions are maintained, which is crucial for achieving consistent drug potency and quality. For example, in the manufacturing of soft gel capsules or hard gelatin capsules, these systems facilitate the seamless transfer of powder into filling machines, minimizing the risk of product loss or contamination. The systems also support the integration of automated processes, enabling manufacturers to streamline their production lines and improve overall efficiency. Furthermore, the ability to handle sensitive powders, such as those used in biologics or specialty drugs, ensures that the product remains stable and free from degradation during transport.
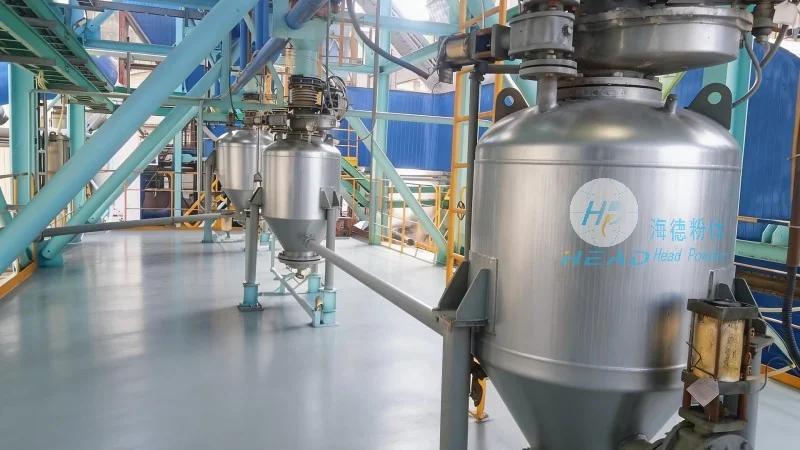
Beyond pharmaceuticals, capsule powder conveying systems are widely utilized in chemical and food processing sectors. In chemical manufacturing, these systems help transport raw chemicals, catalysts, and reagents to reactors or processing equipment. The systems' ability to handle abrasive or corrosive powders, along with their robust construction, makes them suitable for harsh industrial environments. Similarly, in the food industry, they are employed to convey ingredients like spices, vitamins, or flavorings in food production lines. The hygienic design of these systems, with features like easy-to-clean surfaces and sealed components, ensures compliance with food safety regulations. This is particularly important in applications such as the production of nutritional supplements or processed foods, where product purity and safety are non-negotiable. The systems' efficiency in maintaining consistent flow rates also contributes to improved product quality and reduced waste in these industries.
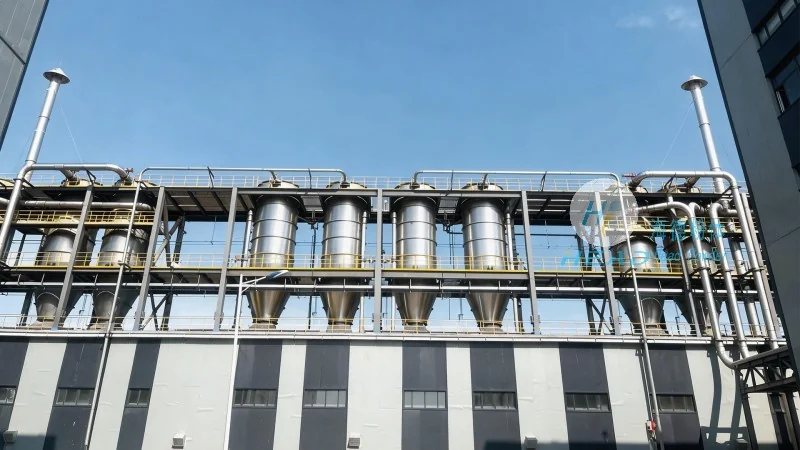
Shandong HeadPowder Engineering Co., Ltd., a leading provider of powder handling solutions, specializes in designing and manufacturing capsule powder conveying systems tailored to specific industrial needs. With headquarters in Shandong, China, the company leverages over two decades of experience in the field to deliver high-quality, reliable equipment. The company's engineering team focuses on understanding the unique challenges of each application, ensuring that the systems are optimized for performance, durability, and cost-effectiveness. By incorporating advanced materials and precision manufacturing techniques, HeadPowder systems are built to withstand the demands of continuous operation in demanding environments. The company also offers comprehensive support services, including installation, maintenance, and technical consultation, to ensure that clients achieve maximum operational efficiency and product quality. With a commitment to innovation and customer satisfaction, Shandong HeadPowder Engineering Co., Ltd. remains a trusted partner for businesses seeking efficient powder handling solutions.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top