HeadPowder, a leading provider of industrial conveying solutions, specializes in the design and manufacturing of slurry and powder conveying equipment. This article delves into the working principles and key features of such equipment, offering insights into how these systems efficiently handle diverse materials in various industrial applications.
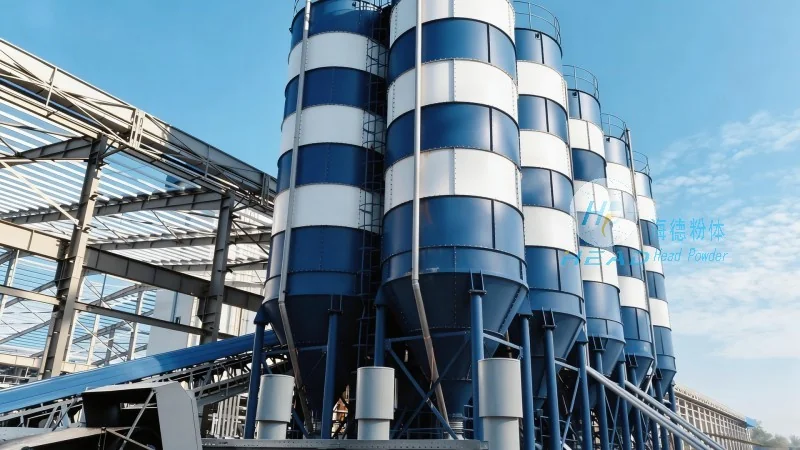
HeadPowder Engineering Co., Ltd. is headquartered in Shandong, China. As a professional manufacturer in the field of material handling, the company focuses on delivering high-quality, reliable conveying equipment tailored to meet the specific needs of clients across different industries.
The core working principle of slurry and powder conveying equipment involves the use of specialized mechanisms to transport bulk materials, such as powders, granules, and slurries, from one location to another. These systems typically operate by creating a flow path through which the material is propelled or drawn, depending on the design. For example, pneumatic conveying systems utilize air pressure to move powders, while hydraulic or mechanical systems may employ screw conveyors, belt conveyors, or pump-driven mechanisms for slurry transport.
In pneumatic conveying, the material is suspended in a stream of air and transported through pipes. This method is particularly effective for handling fine powders and dry materials, as it minimizes material degradation and contamination. Conversely, slurry conveying often relies on pump systems or gravity-fed mechanisms, where the liquid component carries the solid particles, ensuring consistent flow and preventing clogging in the pipeline.
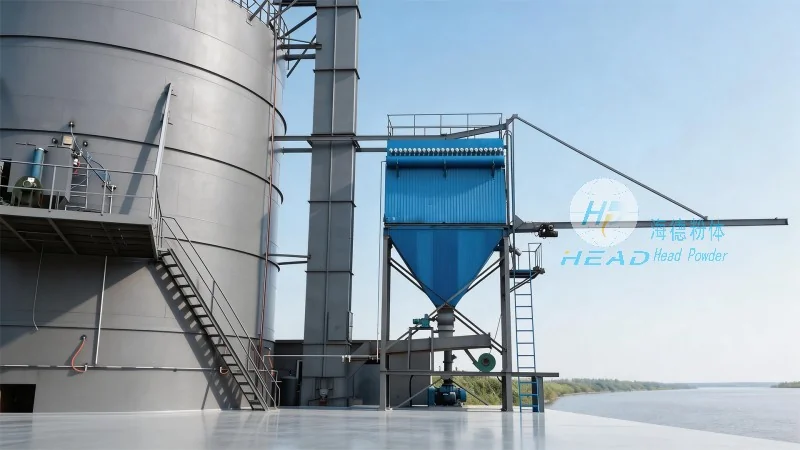
Several key features distinguish high-quality slurry and powder conveying equipment, making them suitable for demanding industrial environments. Firstly, durability and corrosion resistance are critical, as these systems often handle abrasive or corrosive materials. Materials like stainless steel, high-grade alloys, and wear-resistant coatings are commonly used to extend the equipment's lifespan and maintain performance.
Secondly, efficiency and energy savings are important considerations. Modern conveying systems incorporate advanced control technologies, such as variable frequency drives (VFDs), to optimize energy consumption while maintaining consistent material flow. This not only reduces operational costs but also enhances the overall sustainability of the process.
Thirdly, flexibility and adaptability are essential features. Many conveying systems are designed to handle a wide range of materials, from fine powders to heavy slurries, with adjustable parameters like flow rate, pressure, and particle size. This versatility allows manufacturers to customize solutions for specific applications, such as in mining, food processing, or chemical industries.
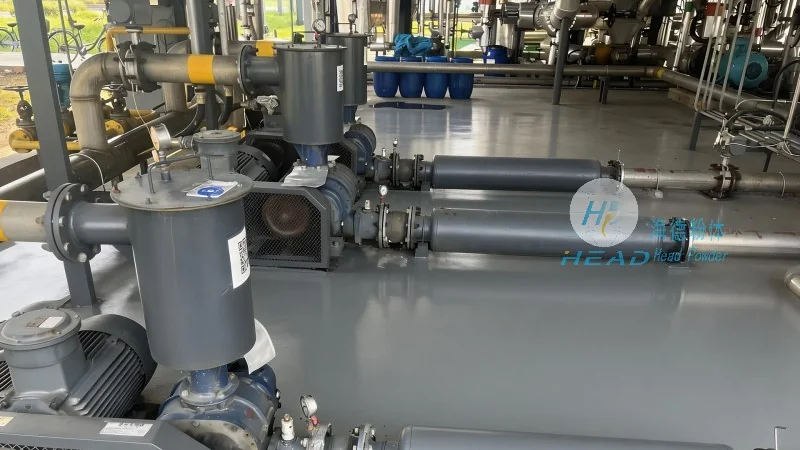
Additionally, safety and operational reliability are paramount. Equipment is equipped with safety features like pressure relief valves, overload protection, and automatic shut-off mechanisms to prevent accidents and ensure smooth operation. Regular maintenance and monitoring systems are also integrated to minimize downtime and ensure long-term reliability.
Slurry and powder conveying equipment finds extensive applications across various industries. In the mining sector, these systems are used to transport ore, tailings, and other minerals from processing plants to storage or disposal sites. The food and beverage industry utilizes them for handling powders like flour, sugar, and spices, ensuring hygienic and efficient production processes. In the chemical industry, they are employed to convey slurries containing chemicals, ensuring precise control over material handling and reducing the risk of contamination.
Slurry and powder conveying equipment, as exemplified by the solutions offered by HeadPowder Engineering Co., Ltd., plays a vital role in modern industrial operations. By understanding the working principles and key features of these systems, industries can select the most appropriate equipment to enhance productivity, reduce costs, and ensure safe, efficient material handling. With a focus on quality, innovation, and customer satisfaction, HeadPowder continues to provide reliable conveying solutions that meet the evolving needs of the global market.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top