For industries dealing with food additives, efficient and reliable powder handling is crucial. The food additive powder conveying system is a specialized equipment designed to transport bulk powders, such as flavorings, colorants, and preservatives, within processing facilities. Understanding its working principle and key features is essential for optimizing production processes and ensuring product quality.
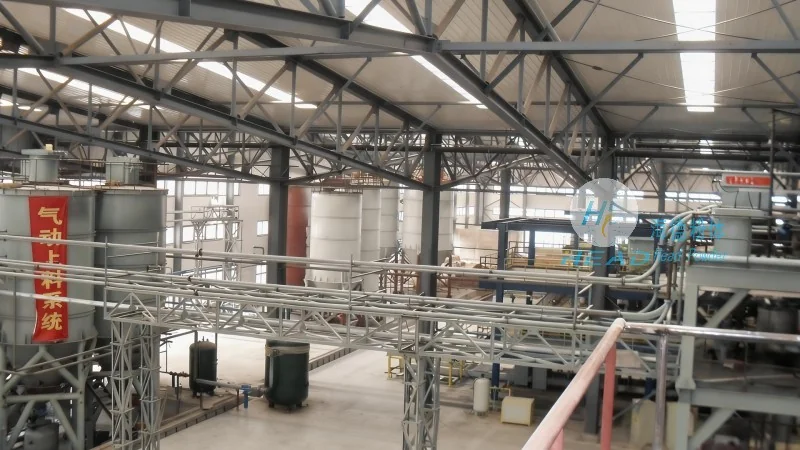
At the core of these systems is a combination of mechanical and pneumatic components that work in tandem to move powders from one location to another. The typical process begins with the feeding of the powder into a hopper or storage silo. From there, the powder is transferred through a network of pipes or conveyor tubes using either positive pressure (air or gas) or negative pressure (suction). The system often incorporates a blower or compressor to generate the necessary airflow, which propels the powder particles through the system. Additionally, features like rotary valves, check valves, and dust collectors are integrated to control flow, prevent backflow, and maintain air quality, ensuring the system operates safely and efficiently.
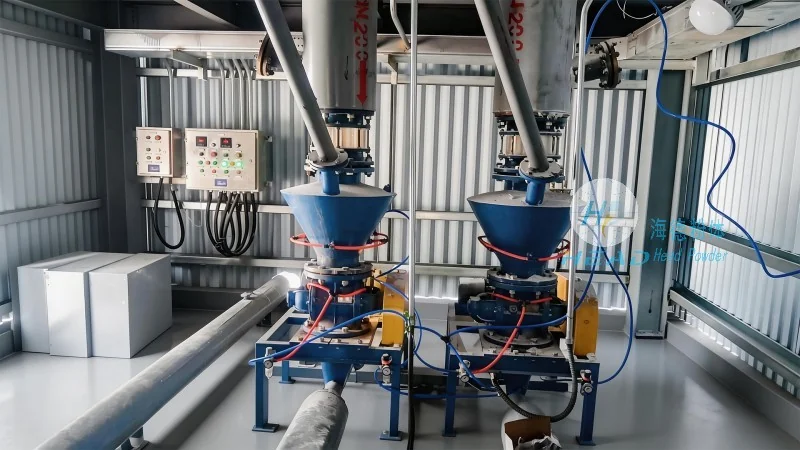
Several critical features distinguish high-quality food additive powder conveying systems. First, hygienic design is paramount, as these systems must comply with strict food safety regulations. Components are often made from stainless steel and are easy to clean, reducing the risk of contamination. Second, flexibility is a key feature, allowing the system to handle various powder types with different flow properties. This adaptability is achieved through adjustable airflow rates and the use of different conveying materials, such as flexible hoses or rigid pipes. Third, energy efficiency is a significant consideration, as the system’s power consumption directly impacts operational costs. Modern systems incorporate energy-saving technologies, such as variable frequency drives (VFDs), which adjust motor speed based on the required airflow, minimizing energy waste. Fourth, control and monitoring capabilities are essential for maintaining consistent performance. Advanced systems include sensors and control panels that allow operators to monitor flow rates, pressure, and system status in real-time, enabling quick adjustments and preventing downtime.
Food additive powder conveying systems are widely used in various stages of food production. In the initial mixing phase, these systems efficiently deliver flavorings and colorants to mixing tanks, ensuring uniform distribution of ingredients. During packaging, they transfer powders to filling machines, maintaining consistent flow rates and preventing product loss. Additionally, in quality control processes, the system can be used to transport samples for testing, ensuring accurate and reliable results. The versatility of these systems makes them indispensable in modern food processing facilities, where efficiency and compliance are top priorities.
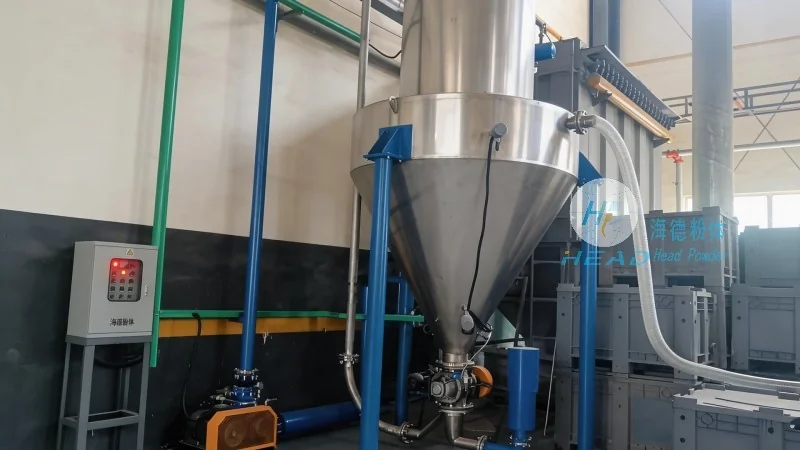
Shandong HeadPowder Engineering Co., Ltd., operating under the brand name headpowder, is a leading manufacturer of specialized powder handling equipment. With a focus on innovation and quality, the company has developed advanced food additive powder conveying systems tailored to the unique needs of the food industry. HeadPowder’s products are designed to meet the highest standards of hygiene and efficiency, ensuring that food processing facilities can operate smoothly while maintaining product safety. The company’s commitment to customer satisfaction and technical excellence has made it a trusted partner for businesses worldwide.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top