For professionals in the construction and material handling industries, understanding the efficient and reliable operation of sand and gravel powder conveying systems is crucial. These systems are essential for transporting bulk materials like sand, gravel, and other fine powders across various industrial applications. The following article provides an in-depth look at the working principles and key features of such systems, presented by Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer based in China.
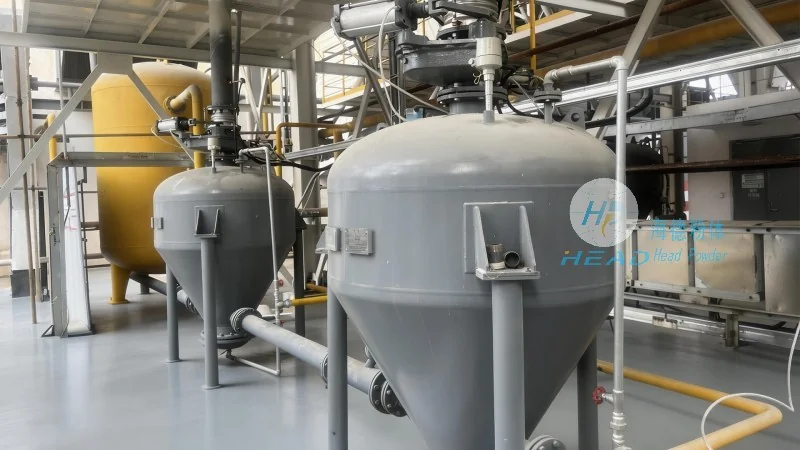
The core function of a sand and gravel powder conveying system is to transport bulk materials from a source to a destination with minimal loss and maximum efficiency. The system typically operates through a combination of mechanical components that work in tandem to achieve this goal. A common mechanism involves a hopper or feeder that feeds the material into a conveyor, which then transports it through a pipeline or open channel. The conveyor may use various technologies such as screw conveyors, pneumatic conveyors, or belt conveyors, depending on the specific requirements of the application. The working principle can be broken down into several key steps:
First, the material is loaded into the hopper or storage silo. The hopper is designed to hold a large volume of material and regulate the flow rate into the conveyor. This initial step ensures a consistent feed rate, preventing overloading or underloading of the system. Next, the material is transferred to the conveyor. In a screw conveyor, for example, a rotating screw (or auger) pushes the material forward through a tube or trough. The rotation of the screw creates a positive displacement, moving the material along the length of the conveyor. In pneumatic conveyors, the material is suspended in a stream of air and transported through a pipeline. The air pressure and velocity are carefully controlled to maintain the material's flow and prevent blockages. Finally, the material is discharged at the destination point, completing the conveying process. The entire system is often equipped with sensors and controls to monitor the flow rate, pressure, and other parameters, ensuring optimal performance and safety.
Modern sand and gravel powder conveying systems are characterized by several advanced features that enhance their performance, durability, and adaptability. These features are designed to meet the diverse needs of industrial applications while maintaining high efficiency and reliability. Some of the most notable features include:
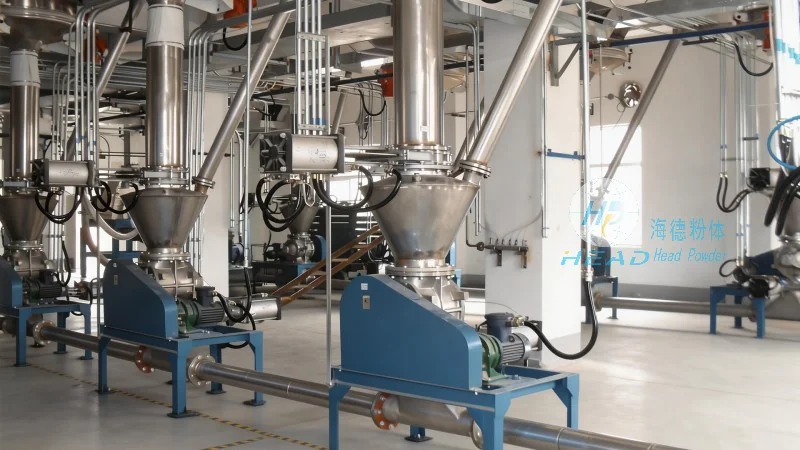
1. Material Handling Flexibility: The systems are capable of handling a wide range of materials, from fine powders to coarse aggregates. This flexibility allows them to be used in various industries, including construction, mining, and manufacturing. The design of the conveyor components, such as the screw diameter and pitch, can be adjusted to accommodate different material types and sizes.
2. Energy Efficiency: Advanced systems incorporate energy-saving technologies, such as variable speed drives and optimized airflow, to reduce power consumption. This not only lowers operational costs but also contributes to environmental sustainability. The use of efficient motors and control systems further enhances energy efficiency.
3. Low Maintenance Requirements: High-quality materials and robust construction reduce the need for frequent maintenance. The components are designed to withstand the abrasive nature of sand and gravel, minimizing wear and tear. Regular inspections and preventive maintenance schedules are recommended to ensure long-term reliability.
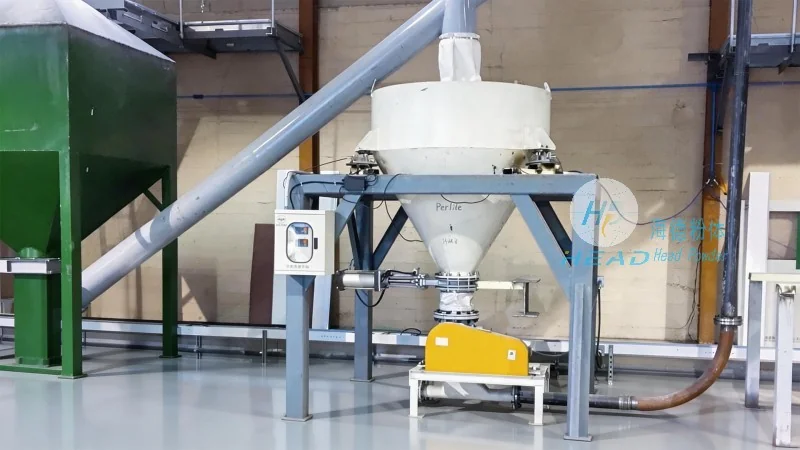
4. Customization Options: Manufacturers like Shandong HeadPowder Engineering Co., Ltd. offer customized solutions tailored to specific customer needs. This includes adjustments to the conveyor length, capacity, and material handling capabilities. Customization ensures that the system meets the exact requirements of the application, maximizing efficiency and minimizing downtime.
5. Safety and Compliance: The systems are designed to comply with industry safety standards and regulations. Features such as overload protection, emergency stop buttons, and safety interlocks are integrated to prevent accidents and ensure safe operation. The use of durable materials and robust construction also enhances safety by reducing the risk of material spillage or equipment failure.
Sand and gravel powder conveying systems are critical components in the material handling industry, enabling the efficient and reliable transport of bulk materials. The working principles and key features discussed above highlight the advanced technology and engineering that go into these systems. By understanding these aspects, industry professionals can make informed decisions when selecting and implementing such systems. Shandong HeadPowder Engineering Co., Ltd. specializes in providing high-quality, customized conveying solutions that meet the diverse needs of their clients, ensuring optimal performance and reliability in various industrial applications.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top