For industrial operations that require efficient and reliable handling of bulk powders, the automatic tonne bag feeding and powder conveying system has emerged as a critical solution. This technology, developed by Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer based in Shandong, China, offers a sophisticated approach to managing the entire process from bag opening to material transfer. Understanding its working principle and key features is essential for industries such as pharmaceuticals, chemicals, food processing, and mining, where precision and safety are paramount.
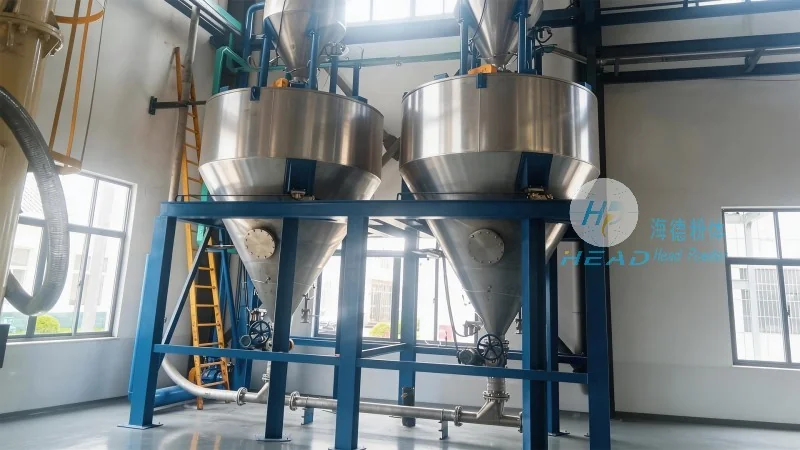
The core of the system lies in its automated sequence of operations, designed to handle large tonne bags (typically 1 tonne or more) with minimal human intervention. The process begins with the placement of the tonne bag onto a specialized feeding platform. Once positioned, the system initiates the bag opening mechanism, which may involve cutting or tearing the bag's top to access the contents. This is followed by the activation of a feeding hopper that draws the powder from the bag and directs it into a conveyor or pneumatic transport system. The system is equipped with sensors to monitor the bag's position, the flow rate of the material, and any potential blockages, ensuring a smooth and continuous operation. The entire sequence is controlled by a programmable logic controller (PLC), which coordinates the actions of various components, including motors, valves, and sensors, to maintain optimal performance.
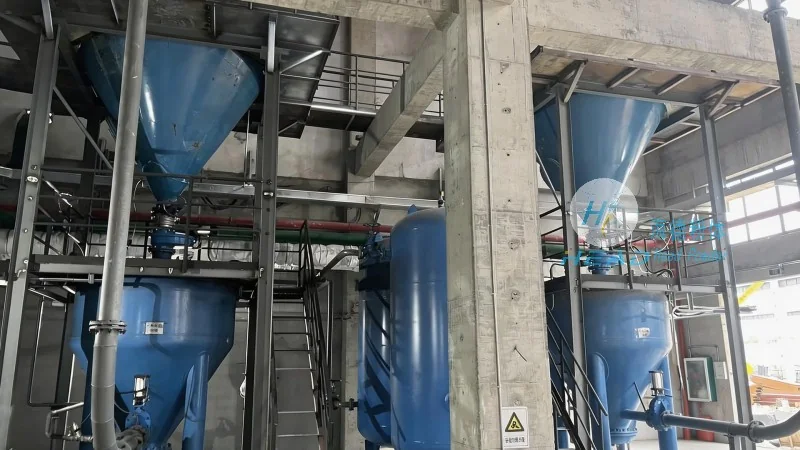
The automatic tonne bag feeding and powder conveying system from Shandong HeadPowder Engineering Co., Ltd. is distinguished by several advanced features that enhance its functionality and user experience. First, the system incorporates a robust bag handling mechanism that can accommodate various bag sizes and materials, ensuring versatility across different applications. The feeding hopper is designed with a wide inlet and a variable speed control, allowing for precise adjustment of the material flow rate, which is crucial for maintaining consistent product quality and preventing overloading of downstream equipment. Additionally, the system features an integrated dust collection and filtration system, which helps to minimize airborne particles and comply with environmental regulations. Safety is another key aspect, with the inclusion of emergency stop buttons, overload protection, and automatic shut-off in case of blockages, ensuring operator safety and equipment longevity. The system also offers easy maintenance, with accessible components and a modular design that allows for quick replacement of parts without disrupting the entire operation.
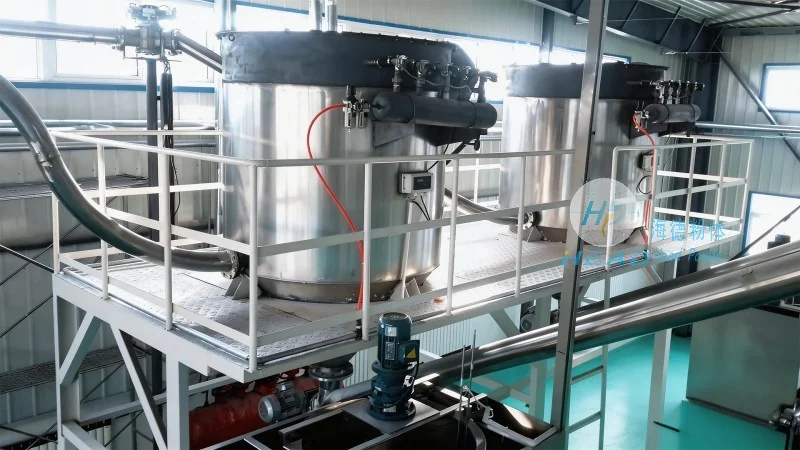
The implementation of this automatic system brings numerous benefits to industrial processes. By automating the bag opening and feeding process, it significantly reduces labor costs and the risk of human error, leading to higher operational efficiency. The precise control over material flow ensures consistent product quality, which is vital in industries like pharmaceuticals where uniformity is critical. Moreover, the system's ability to handle large tonne bags reduces the number of handling steps, minimizing the risk of material spillage and contamination. This is particularly advantageous in environments where hygiene and safety are top priorities. The system is widely applicable in various sectors, including chemical manufacturing, where it facilitates the transfer of reactive powders; in food processing, where it ensures the safe handling of ingredients; and in mining operations, where it aids in the transport of ore and other bulk materials. The adaptability of the system, combined with its reliability, makes it an ideal choice for businesses seeking to streamline their material handling processes and improve overall productivity.
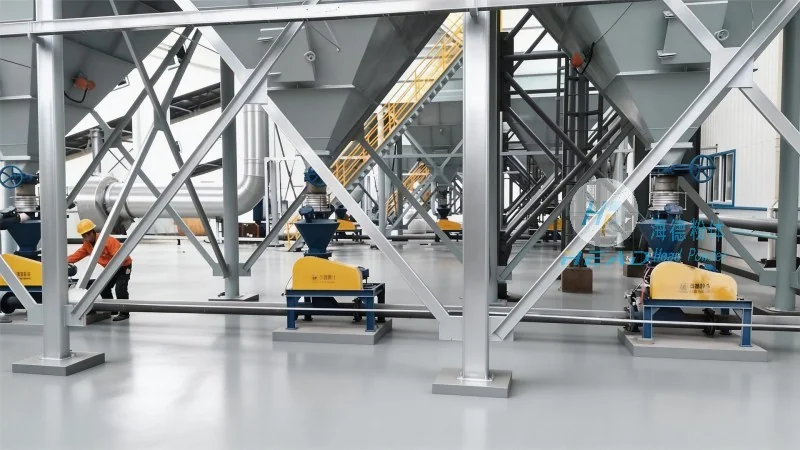
In conclusion, the automatic tonne bag feeding and powder conveying system developed by Shandong HeadPowder Engineering Co., Ltd. represents a significant advancement in bulk material handling technology. Its working principle, centered on automation and precision, combined with its comprehensive set of features, addresses the challenges faced by industries dealing with large volumes of powders. By integrating advanced sensors, control systems, and safety mechanisms, the system ensures efficient, safe, and reliable operation. For companies looking to enhance their material handling capabilities, this system offers a robust solution that not only improves productivity but also adheres to industry standards and environmental regulations. As a leading manufacturer based in Shandong, China, HeadPowder continues to innovate in this field, providing tailored solutions that meet the diverse needs of its global clientele.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top