Automated material handling equipment has become an indispensable component in modern industrial operations, streamlining processes and enhancing efficiency across various sectors. These systems are engineered to move, store, and manage materials with minimal human intervention, playing a crucial role in optimizing workflow and reducing operational costs. Understanding the core components and design principles behind such equipment is essential for businesses seeking to integrate advanced logistics solutions.
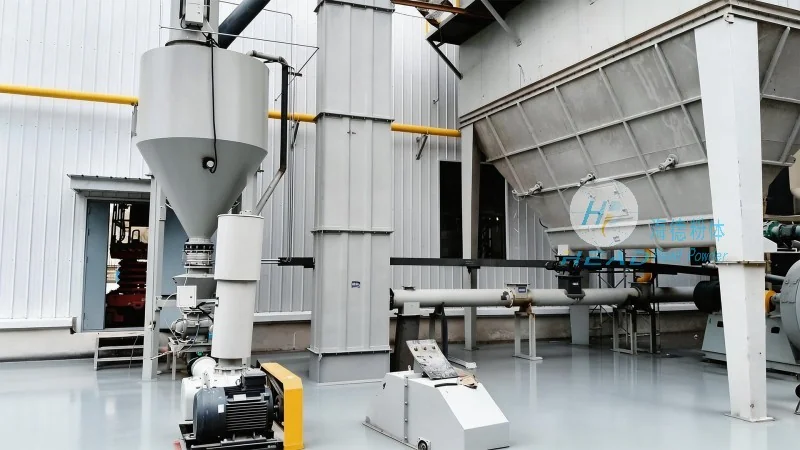
At the heart of fully automatic material handling equipment are several integrated components that work in tandem to ensure seamless operation. These typically include conveyor systems, robotic arms, automated storage and retrieval systems (AS/RS), and control software. Conveyor systems, such as belt or chain conveyors, transport materials horizontally or vertically, while robotic arms handle tasks like picking, placing, and sorting. AS/RS systems enable automated storage and retrieval of goods, optimizing warehouse space utilization. Control software, often integrated with sensors and IoT technology, monitors and adjusts the system's performance in real-time, ensuring precision and reliability.
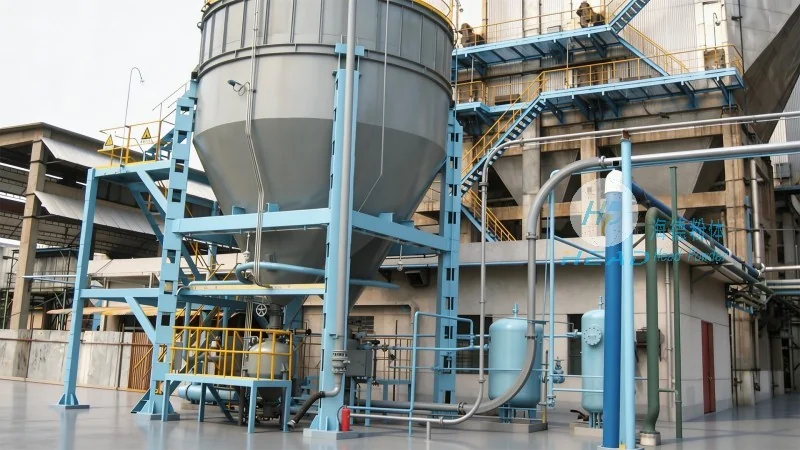
The design of fully automatic material handling equipment is guided by several key principles aimed at maximizing efficiency, safety, and adaptability. First, modularity allows for flexible configurations, enabling systems to be scaled or reconfigured to meet changing operational needs. Second, integration with existing infrastructure minimizes disruption during implementation, ensuring a smooth transition to automated processes. Third, energy efficiency is a critical consideration, with designs incorporating advanced motor controls and energy-saving features to reduce operational costs. Additionally, safety is paramount, with built-in sensors and emergency stop mechanisms to prevent accidents and protect personnel. The use of standardized interfaces and protocols also facilitates easy integration with other industrial systems, enhancing overall operational connectivity.
Fully automatic material handling equipment finds applications across diverse industries, including manufacturing, logistics, and warehousing. In manufacturing, these systems streamline the movement of raw materials to production lines and finished products to storage areas, reducing bottlenecks and improving production throughput. In logistics, automated conveyor networks and sorting systems enhance order processing speed and accuracy, while in warehousing, AS/RS systems optimize inventory management and retrieval times. The benefits of such equipment extend beyond efficiency, as they also contribute to improved workplace safety by minimizing manual handling tasks and reducing the risk of workplace injuries. Furthermore, the integration of data analytics and predictive maintenance capabilities allows for proactive system management, extending equipment lifespan and reducing downtime.
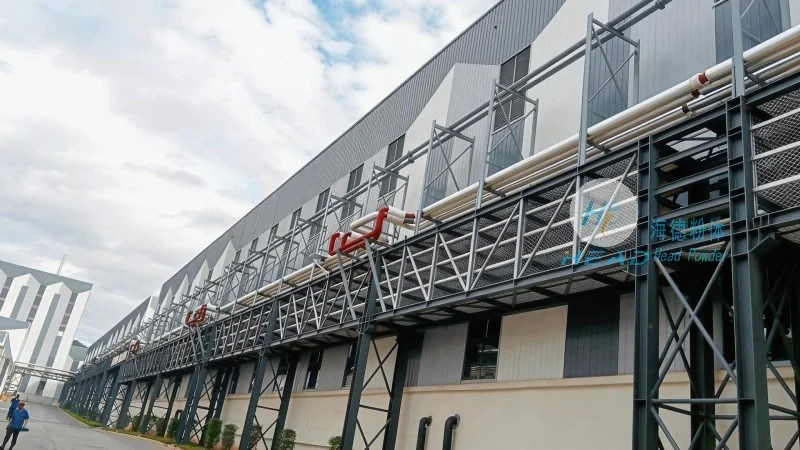
Shandong HeadPowder Engineering Co., Ltd., operating under the brand name headpowder, is a leading manufacturer specializing in the design, development, and supply of fully automatic material handling equipment. With a strong commitment to innovation and quality, the company leverages advanced engineering and technology to deliver customized solutions tailored to the unique needs of its clients. HeadPowder's products are engineered to meet international standards and are supported by comprehensive after-sales services, ensuring reliable performance and customer satisfaction. HeadPowder's headquarters is located in Shandong, China, where the company maintains state-of-the-art manufacturing facilities and a dedicated research and development team focused on advancing material handling technologies.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top