When it comes to transporting fine powders like bentonite powder, the choice of equipment plays a crucial role in ensuring efficiency, safety, and reliability. Pneumatic conveying systems have emerged as a preferred solution for such applications due to their ability to handle powders in a closed environment, minimizing dust emissions and providing a controlled flow. This article delves into the specifics of bentonite powder pneumatic conveying equipment, exploring its structure, working principles, and the key components that make it an effective solution for powder handling in various industries. Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer based in Shandong, China, specializes in the design and production of advanced pneumatic conveying systems for various industrial applications.
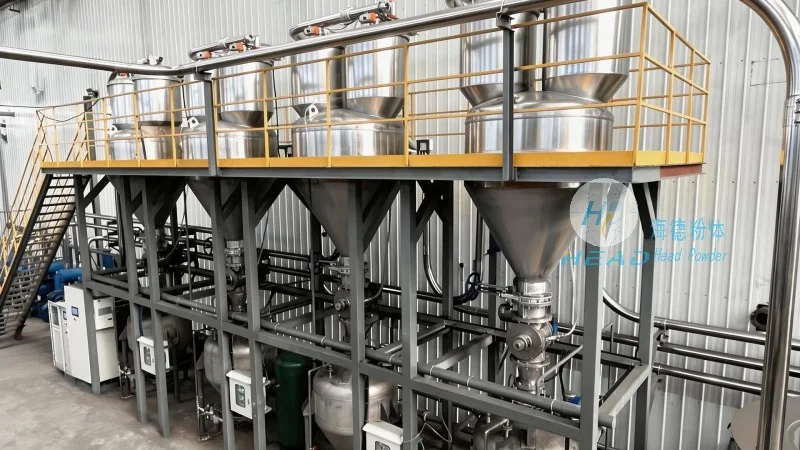
A typical bentonite powder pneumatic conveying system comprises several essential components that work in tandem to transport the material from the source to the destination. The primary components include the hopper, feeder, air compressor, conveying pipeline, and receiver. Each component has a specific function that contributes to the overall efficiency of the system.
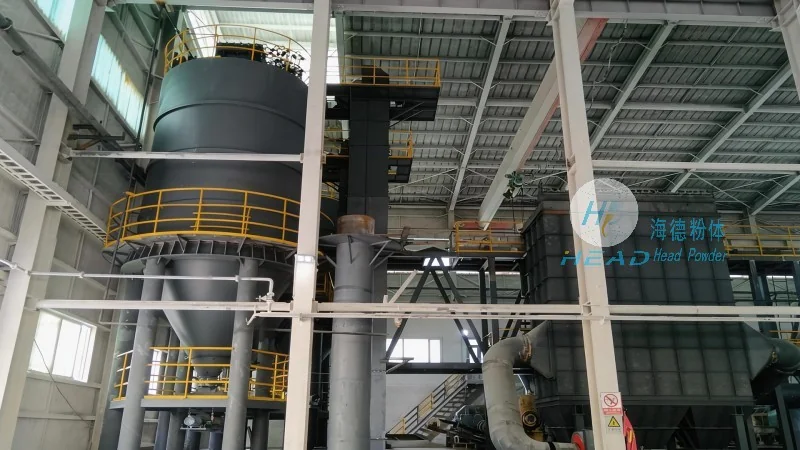
The hopper is the initial component where the bentonite powder is stored before it is fed into the conveying system. It is designed to hold a sufficient quantity of powder to ensure a continuous supply to the feeder. The hopper often features a conical or rectangular shape to facilitate the flow of powder and prevent clogging. In some designs, a rotary valve or a screw feeder is installed at the bottom of the hopper to control the discharge rate of the powder. This feeding mechanism is critical as it determines the uniformity and consistency of the powder flow into the conveying line.
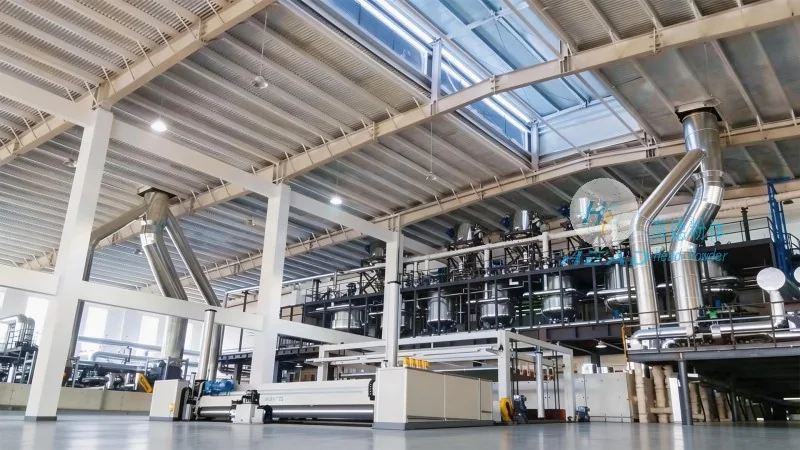
The feeder is responsible for regulating the flow of bentonite powder from the hopper into the air stream. There are different types of feeders used in pneumatic conveying systems, such as rotary valves, star feeders, or screw feeders. The choice of feeder depends on the characteristics of the powder, including its density, flowability, and moisture content. For bentonite powder, which can be prone to bridging or agglomeration, a rotary valve with a suitable design is often preferred. This type of feeder provides a consistent and controlled release of powder, preventing surges or blockages that could disrupt the conveying process.
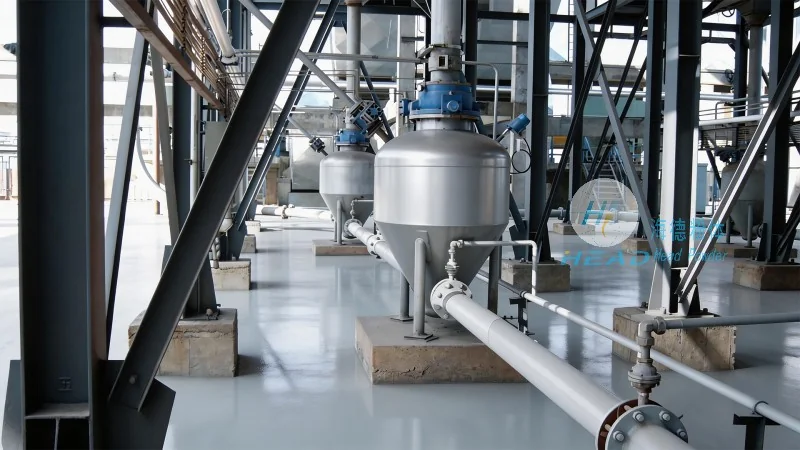
The air compressor is the heart of the pneumatic conveying system, responsible for generating the high-pressure air or gas that propels the bentonite powder through the pipeline. The compressor can be either a positive displacement type or a centrifugal type, depending on the system requirements. For fine powders like bentonite, a positive displacement compressor is commonly used as it provides a stable and consistent air flow at the required pressure. The air compressor is typically equipped with a filter and a moisture separator to ensure that the air is clean and free from contaminants that could affect the powder quality or the performance of the system.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top