Carbon black and coal powder are widely used in various industrial processes, and the efficient transportation of these powders is crucial for maintaining production efficiency and product quality. Pneumatic conveying equipment has emerged as a key solution for handling such materials, offering advantages like dust-free operation, high transport capacity, and flexibility in system design. This article provides an overview of the structure and operational principles of carbon black and coal powder pneumatic conveying systems, with a focus on the technology and applications developed by Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer based in China.
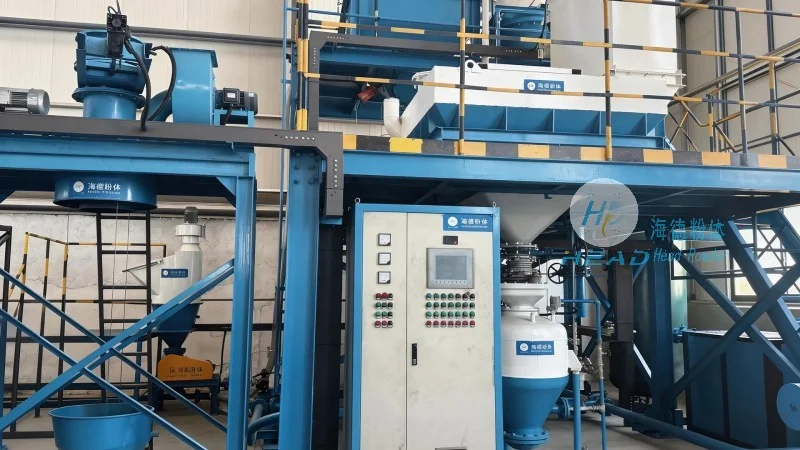
Pneumatic conveying, also known as air conveying, is a method of transporting bulk solid materials through a pipeline using a gas stream, typically air. This technology is particularly suitable for carbon black and coal powder due to their fine particle size and the need for clean, dust-free handling. The system operates by creating a pressure differential or using vacuum to move the material through the pipeline, ensuring safe and efficient transport from the source to the destination.
The carbon black and coal powder pneumatic conveying system consists of several critical components that work in tandem to ensure reliable operation. These components include the material feed system, the conveying pipeline, the air supply unit, and the separation and collection equipment. Each component plays a vital role in the overall performance and efficiency of the system.
The material feed system is the initial stage of the pneumatic conveying process, responsible for introducing carbon black or coal powder into the pipeline. This system typically includes a hopper or bin that stores the material, a feeder (such as a rotary valve or screw feeder) that controls the flow rate, and a feeder valve that regulates the material discharge. The design of the feed system is crucial for preventing material bridging, clogging, or uneven flow, which can lead to system inefficiencies or blockages. Shandong HeadPowder Engineering Co., Ltd. employs advanced feeding mechanisms that ensure consistent material supply, even for cohesive or fine powders like carbon black and coal powder.
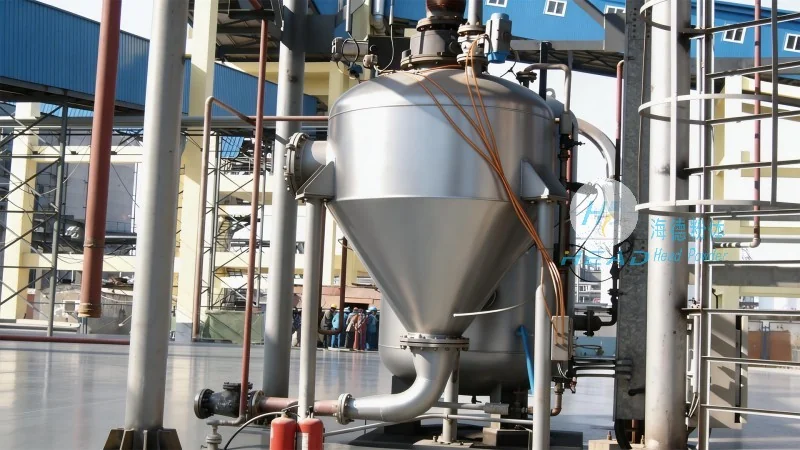
The conveying pipeline forms the backbone of the pneumatic system, transporting the material from the feed point to the discharge point. The pipeline is usually made of materials such as stainless steel or plastic, chosen for their resistance to corrosion and wear from the abrasive powders. The air supply unit, which can be a blower or a vacuum pump, generates the necessary pressure or vacuum to move the material through the pipeline. The air velocity within the pipeline is carefully controlled to ensure that the material particles are suspended and transported efficiently without causing excessive pressure drops or particle degradation.
The final stage of the pneumatic conveying process involves separating the material from the air stream and collecting it at the destination. This is typically achieved using a cyclone separator or a bag filter. The cyclone separator uses centrifugal force to separate the particles from the air, while the bag filter traps the particles in fabric bags. The separated material is then discharged into a collection bin or silo. Shandong HeadPowder Engineering Co., Ltd. integrates high-efficiency separation technologies that minimize dust emissions and ensure complete material recovery, meeting stringent environmental and safety standards.
The operational principle of a carbon black and coal powder pneumatic conveying system is based on the interaction between the solid particles and the air stream. When the air velocity is sufficient to overcome the gravitational force on the particles, the particles become suspended and are carried along the pipeline. The system can operate in either positive pressure (pressure conveying) or negative pressure (vacuum conveying) modes, depending on the application requirements. Positive pressure systems are often used for long-distance or high-capacity transport, while vacuum systems are suitable for short-distance or low-volume applications.
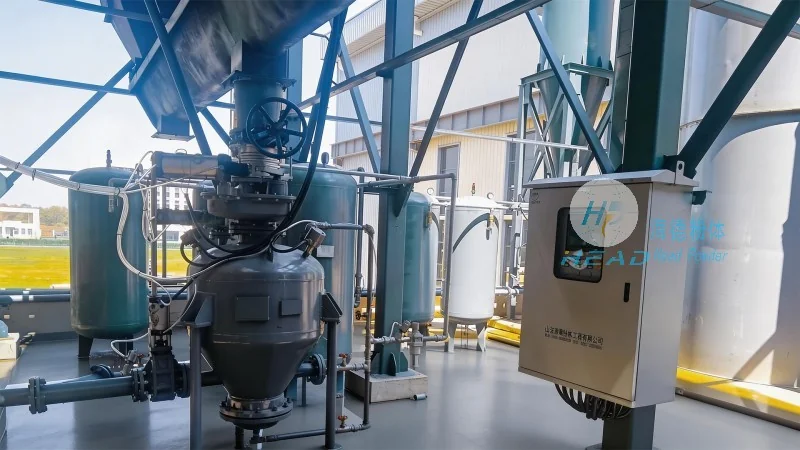
One of the key advantages of pneumatic conveying for carbon black and coal powder is its ability to handle fine powders without the need for mechanical components that can cause wear or contamination. The system also provides a dust-free environment, which is essential for maintaining product quality and ensuring workplace safety. Additionally, pneumatic conveying systems are flexible and can be easily integrated with existing production lines, allowing for seamless material transfer between processes.
Carbon black and coal powder pneumatic conveying equipment is widely used in industries such as rubber, plastics, chemicals, and energy. In the rubber industry, carbon black is used as a reinforcing agent in tire manufacturing, and efficient conveying ensures consistent quality and reduced downtime. In the chemical industry, coal powder is used as a fuel or raw material in power plants and chemical processes, and pneumatic conveying helps maintain high throughput and operational efficiency. Shandong HeadPowder Engineering Co., Ltd. has successfully implemented these systems in various industrial settings, demonstrating their reliability and performance in real-world applications.
In conclusion, carbon black and coal powder pneumatic conveying equipment is a critical technology for the efficient and safe handling of fine powders in industrial applications. The system's structure, which includes a material feed system, conveying pipeline, air supply unit, and separation equipment, is designed to optimize performance and minimize operational issues. Shandong HeadPowder Engineering Co., Ltd., with its expertise in pneumatic conveying systems, provides high-quality equipment that meets the demanding requirements of modern industries. By leveraging advanced technology and careful system design, these systems ensure reliable material transport, enhance production efficiency, and contribute to the overall success of industrial operations.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top