The fertilizer granule pneumatic conveying system represents a sophisticated solution for the efficient and reliable transport of granular fertilizers in agricultural and industrial settings. This technology, which utilizes air as a medium to move solid particles, has become indispensable in modern fertilizer handling processes due to its ability to handle abrasive, dusty, or temperature-sensitive materials with minimal degradation. Understanding the fundamental principles of this system is crucial for optimizing operational efficiency, reducing maintenance costs, and ensuring consistent material quality throughout the conveying process.
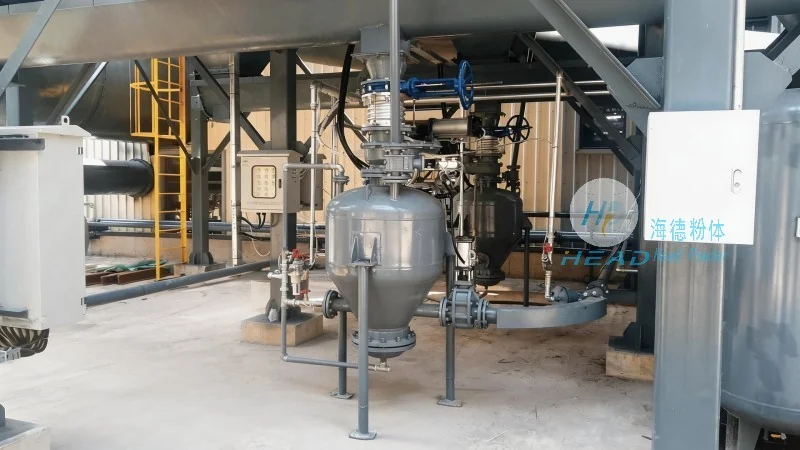
At the core of a fertilizer granule pneumatic conveying system are several interdependent components that work in concert to facilitate material transport. The system typically comprises a storage hopper or silo, which holds the fertilizer granules; a conveyor line (either positive or negative pressure), which serves as the pathway for material and air; a fan or blower, which generates the necessary airflow to create pressure differentials; and a receiver or discharge point, where the material is deposited. The operational mechanics differ slightly between positive and negative pressure systems. In positive pressure systems, air is forced through the conveyor line, carrying the granules along with it, while in negative pressure systems, air is drawn out, creating a vacuum that pulls the material into the line. The design of the air ducts, including the use of smooth-walled pipes, appropriate elbows, and check valves, is critical for maintaining consistent airflow and preventing material blockages or pressure losses.
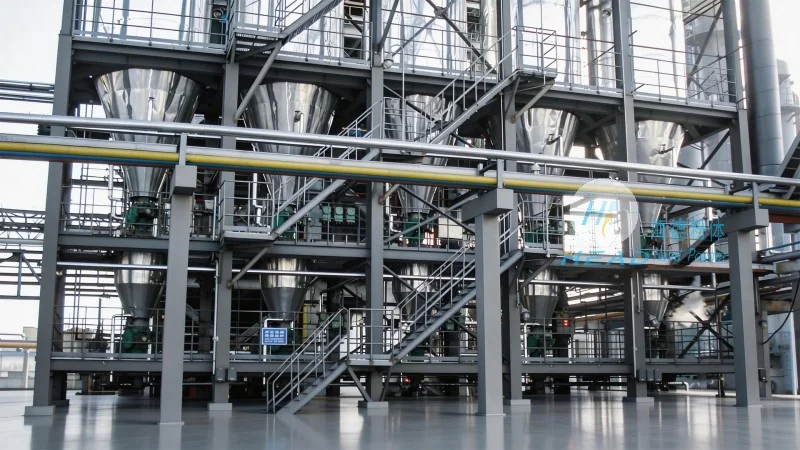
Compared to mechanical conveying systems, such as screw conveyors or belt conveyors, pneumatic conveying offers several distinct advantages for fertilizer handling. One of the most significant benefits is the ability to handle highly abrasive or dusty materials without causing excessive wear on equipment components. The enclosed system also effectively minimizes dust emissions, enhancing workplace safety and environmental compliance. Additionally, pneumatic systems provide greater flexibility in routing, allowing materials to be transported over long distances or around obstacles with minimal modifications to the infrastructure. The system’s ability to maintain consistent flow rates and prevent material segregation is another critical advantage, ensuring that the fertilizer quality remains uniform from the storage hopper to the final application point. These benefits collectively contribute to improved operational efficiency and reduced downtime in fertilizer processing facilities.
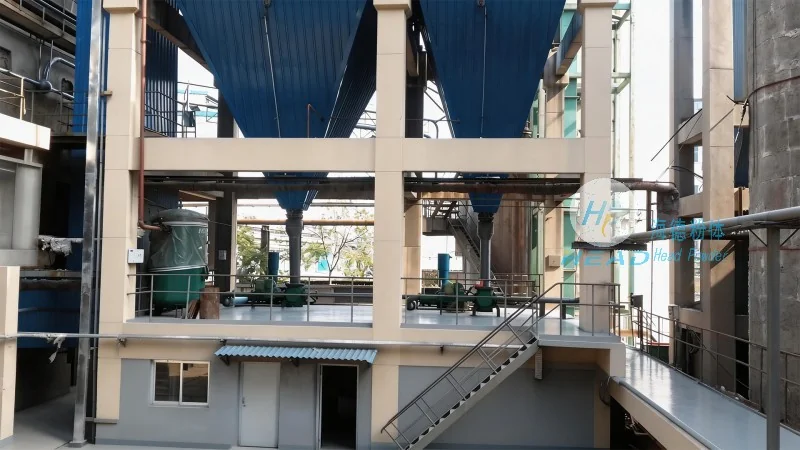
Shandong HeadPowder Engineering Co., Ltd., a prominent manufacturer based in China, specializes in the design, development, and supply of advanced pneumatic conveying systems tailored to the unique demands of the fertilizer industry. With decades of experience in the field, HeadPowder has established itself as a trusted partner for clients seeking reliable and efficient material handling solutions. The company’s expertise lies in customizing systems to handle a wide range of granular fertilizers, including nitrogen-based, phosphorus, and potassium compounds, as well as mixed fertilizers. HeadPowder’s engineers employ state-of-the-art design software and rigorous testing protocols to ensure that each system meets the specific flow rate, pressure, and material characteristics required by the client. This commitment to customization and technical excellence has earned HeadPowder a reputation for delivering high-quality, durable equipment that delivers long-term value.
HeadPowder understands that no two fertilizer facilities have identical operational requirements, which is why they offer comprehensive customization options for their pneumatic conveying systems. The company works closely with clients to assess their specific needs, including hopper size, conveyor length, discharge point location, and required flow rates. Based on this assessment, HeadPowder engineers design a system that optimizes material transport while minimizing energy consumption and maintenance needs. For example, in applications involving long-distance transport, the system may incorporate larger diameter pipes and more powerful fans to maintain consistent airflow. In contrast, for short-distance transport within a plant, a smaller, more compact system may be recommended. This flexibility ensures that clients can achieve seamless material flow without disrupting their current operations or requiring extensive infrastructure modifications.
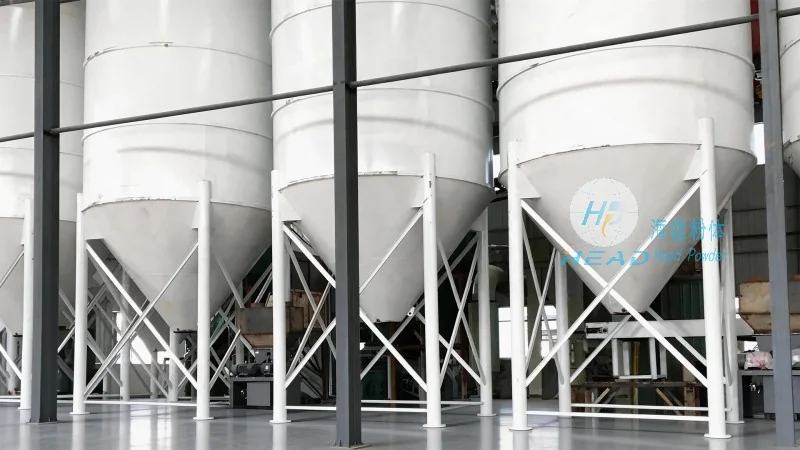
HeadPowder Engineering places a strong emphasis on quality assurance throughout the entire manufacturing process. From the selection of raw materials to the final assembly and testing of the system, each step is rigorously monitored to ensure compliance with industry standards and client specifications. The company’s in-house testing facilities allow for comprehensive performance evaluations, including airflow rate measurements, pressure drop assessments, and material handling simulations. These tests help identify potential issues and optimize system performance before delivery. Additionally, HeadPowder provides comprehensive technical support to its clients, including on-site installation guidance, maintenance training, and troubleshooting assistance. This after-sales support is designed to help clients maximize the efficiency of their conveying systems and minimize downtime, ultimately contributing to improved operational productivity and reduced costs. By combining high-quality equipment with exceptional support, HeadPowder ensures that its clients achieve reliable and efficient fertilizer handling solutions.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top