Compound fertilizer powder conveying systems are critical components in modern agricultural and industrial applications, designed to efficiently transport bulk powder materials such as fertilizers, chemicals, and other granular substances. These systems play a vital role in ensuring smooth material handling processes, enhancing operational efficiency, and reducing labor costs in various production and distribution settings. Understanding the equipment and its design principles is essential for optimizing performance and meeting the demands of contemporary agricultural and industrial sectors.
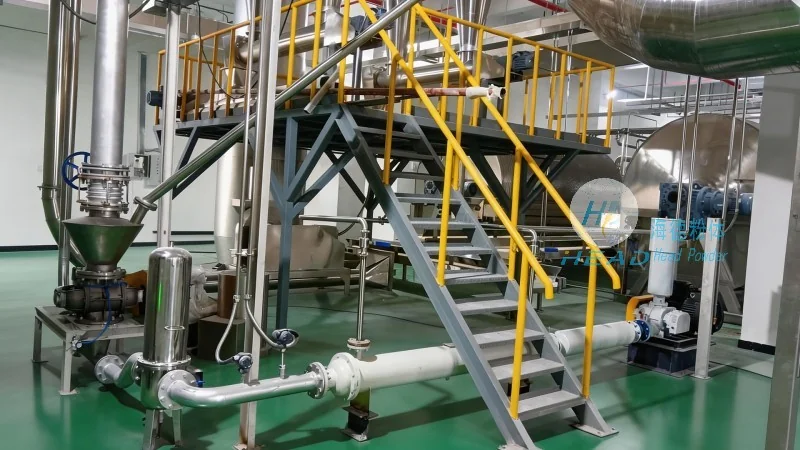
A compound fertilizer powder conveying system typically consists of several key components, including feeders, conveyors, control systems, and storage units. The primary function of these systems is to move bulk powder materials from one location to another with minimal loss, high accuracy, and consistent flow rates. The equipment is engineered to handle a wide range of powder characteristics, such as particle size, moisture content, and bulk density, ensuring reliable operation under diverse conditions.
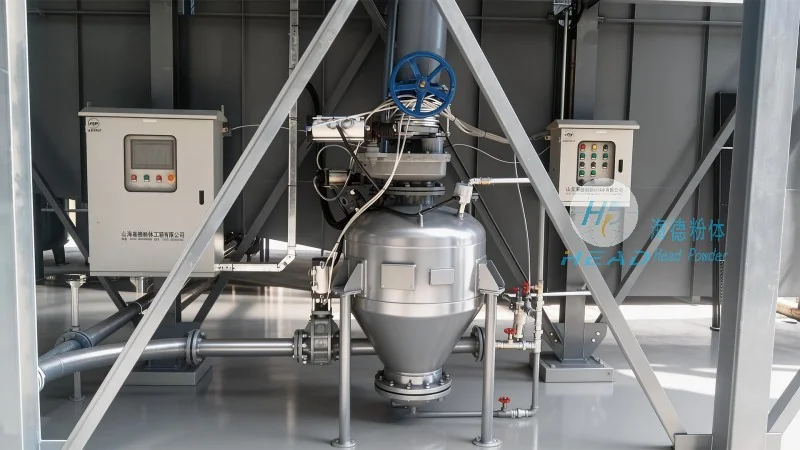
The core components of a compound fertilizer powder conveying system include: 1. Feeding Equipment: This component is responsible for uniformly feeding the powder material into the conveying system. Common types include screw feeders, rotary valves, and pneumatic feeders, each designed to handle specific powder properties and flow rates. 2. Conveying Mechanism: The heart of the system, this part transfers the powder through the pipeline. Options include pneumatic (air-assisted) conveyors, mechanical conveyors (like belt or chain conveyors), and hydraulic systems, depending on the material characteristics and operational requirements. 3. Control System: Advanced control systems monitor and regulate the conveying process, ensuring stable flow, preventing blockages, and optimizing energy consumption. These systems often integrate sensors, variable frequency drives (VFDs), and programmable logic controllers (PLCs) to maintain precise control over the operation. 4. Storage and Discharge Units: These components store the incoming powder and discharge it to the next stage of processing or packaging. Silos, hoppers, and discharge valves are commonly used to manage the material flow and maintain consistent pressure within the system.
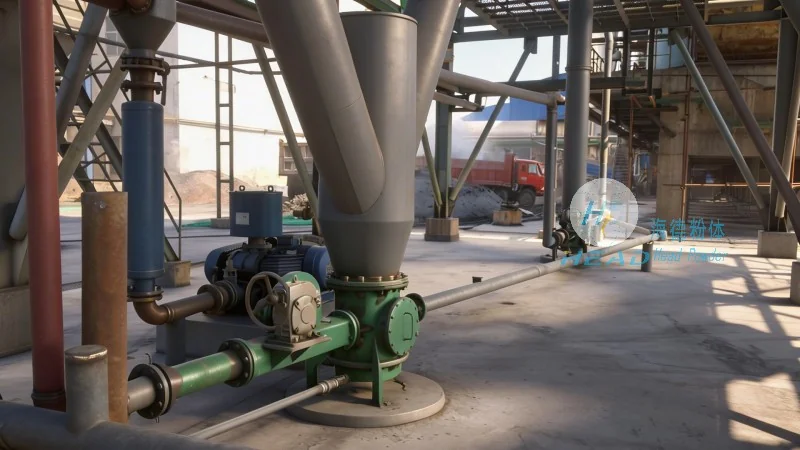
The design of a compound fertilizer powder conveying system is guided by several key principles to ensure optimal performance and reliability. First, material compatibility is a critical consideration. The system must be constructed from materials that are resistant to corrosion, abrasion, and chemical reactions with the fertilizer, such as stainless steel or specialized plastics. Second, airflow management is essential, especially in pneumatic conveying systems. Proper air velocity and pressure are maintained to prevent material segregation, caking, or blockages in the pipeline. Third, system integration is vital for seamless operation. The conveying system is often integrated with other equipment, such as mixers, granulators, or packaging machines, to form a cohesive production line. This integration ensures that the powder is conveyed efficiently from one stage to the next without interruptions or delays. Fourth, energy efficiency is a key design goal. Modern systems incorporate energy-saving features, such as variable speed drives and optimized air flow, to reduce operational costs and minimize environmental impact.
Compound fertilizer powder conveying systems are widely used in various industries, including agriculture, chemical manufacturing, and food processing. In agricultural applications, these systems are crucial for transporting bulk fertilizers from storage facilities to farms or processing plants. The ability to handle large volumes of powder with minimal waste makes them ideal for meeting the high demand for fertilizers in modern agriculture. In chemical manufacturing, the systems are used to transport raw materials and finished products, ensuring smooth production processes and reducing downtime. The benefits of using a compound fertilizer powder conveying system include: 1. Increased Efficiency: The system automates the material handling process, reducing the need for manual labor and increasing production throughput. 2. Reduced Downtime: By preventing blockages and ensuring consistent flow, the system minimizes equipment downtime and maintenance costs. 3. Improved Product Quality: The uniform feeding and conveying of powder materials result in consistent product quality and reduced segregation. 4. Enhanced Safety: The enclosed system design reduces dust exposure and improves workplace safety for operators. 5. Cost Savings: By optimizing energy use and reducing material loss, the system lowers operational costs over time.
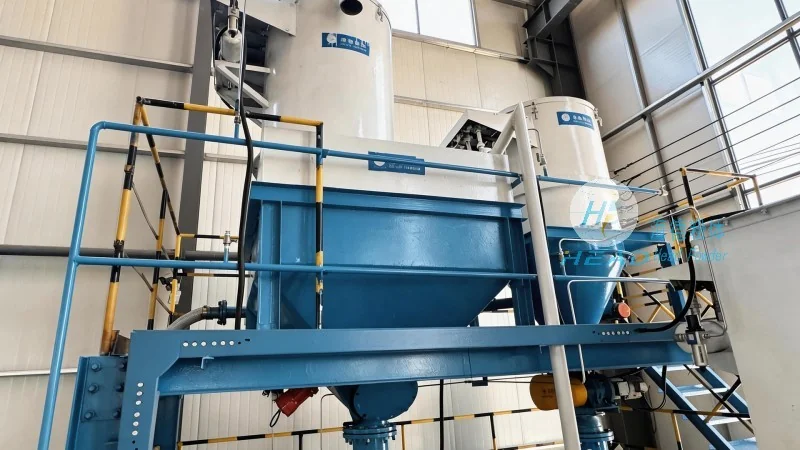
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading manufacturer and supplier of advanced powder handling equipment, including compound fertilizer powder conveying systems. With a strong focus on innovation and quality, HeadPowder has established itself as a trusted partner in the agricultural and industrial sectors. The company is headquartered in Shandong, China, and serves clients worldwide with customized solutions tailored to their specific needs. HeadPowder's commitment to research and development ensures that their products meet the latest industry standards and technological advancements, providing reliable and efficient solutions for powder handling challenges.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top