When it comes to efficient material handling in industrial and warehouse environments, floor conveyors represent a critical solution for optimizing workflow and enhancing operational efficiency. These systems, often referred to as floor-mounted or underfloor conveyors, are designed to transport goods and materials along the floor surface, integrating seamlessly with existing infrastructure. Understanding what floor conveyors are and their underlying design principles is essential for businesses seeking to improve their logistics operations.
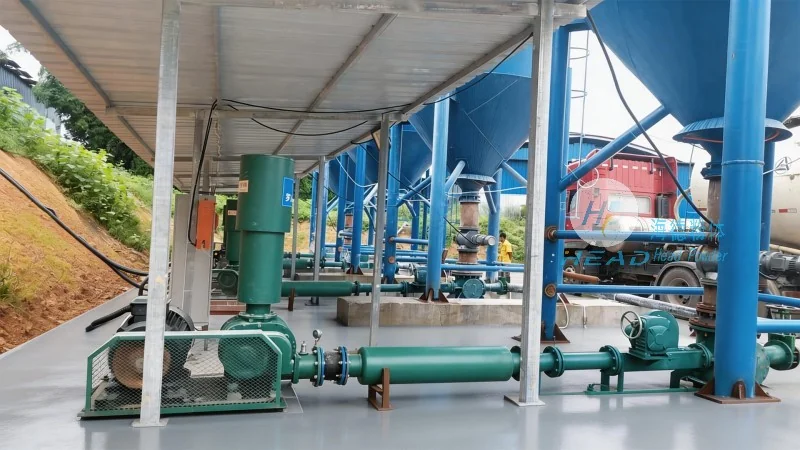
Floor conveyors, also known as floor-mounted or underfloor conveyor systems, are specialized equipment used to move materials horizontally or vertically within a facility. Unlike traditional overhead or belt conveyors, these systems are installed directly on the floor, making them ideal for spaces where vertical clearance is limited or where overhead structures are not feasible. The primary function of a floor conveyor is to facilitate the smooth transfer of products, packages, or bulk materials from one point to another, often integrating with other automation systems such as sorters, packing stations, or storage racks.
The design of floor conveyors is built upon several key principles that ensure reliability, efficiency, and adaptability. These principles include modular construction, allowing for flexible configurations to suit various operational needs; robust material handling capabilities, capable of supporting different types of loads, from lightweight packages to heavy industrial components; and integration with control systems, enabling automated operation and real-time monitoring. A critical aspect of floor conveyor design is the use of durable materials, such as stainless steel or heavy-duty plastic, to withstand the rigors of industrial environments and ensure long-term performance.
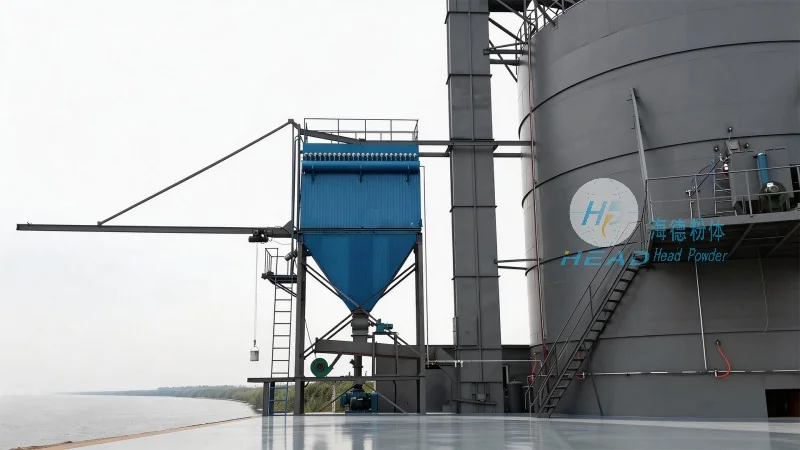
At the heart of any floor conveyor system are several essential components that work in tandem to achieve seamless material movement. These include drive mechanisms, which provide the necessary power to move the conveyor; idlers or rollers, which support the load and reduce friction; and control panels, which allow operators to monitor and adjust the system's operation. Additionally, many floor conveyors incorporate sensors and feedback systems to detect obstructions, adjust speed, or initiate safety protocols, enhancing overall safety and operational reliability. The modular design of these systems also allows for easy expansion or reconfiguration, making them suitable for evolving business needs and changing production requirements.
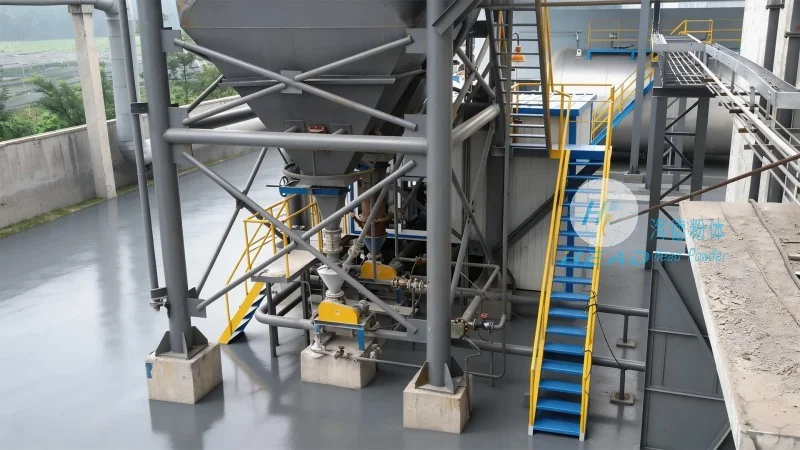
Floor conveyors find widespread application across various industries, including manufacturing, logistics, and warehousing. Their ability to operate in confined spaces and integrate with existing workflows makes them particularly valuable in environments where space is limited or where traditional overhead conveyors are impractical. The benefits of using floor conveyors include increased throughput, reduced labor costs, improved safety by minimizing manual handling, and enhanced flexibility in adapting to changing production demands. By streamlining material movement, these systems help businesses achieve higher productivity and maintain competitive advantages in their respective markets.
As a leading provider of advanced material handling solutions, Shandong HeadPowder Engineering Co., Ltd. specializes in designing, manufacturing, and implementing floor conveyor systems tailored to the unique needs of industrial clients. With a focus on innovation and quality, the company leverages decades of experience to deliver reliable, efficient, and cost-effective conveyor solutions. HeadPowder's commitment to customer satisfaction and technical excellence has established it as a trusted partner in the industry, serving clients across China and beyond. The company's headquarters is located in Shandong, China, where it continues to develop cutting-edge technologies and provide comprehensive support to its customers.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top