When it comes to efficient material handling in industrial settings, vacuum material handling systems have emerged as a reliable and versatile solution. These systems utilize vacuum technology to transport various materials, from powders and granules to small parts and bulk items, with precision and control. In this article, we will explore what vacuum material handling entails and delve into the fundamental design principles that underpin these advanced systems.
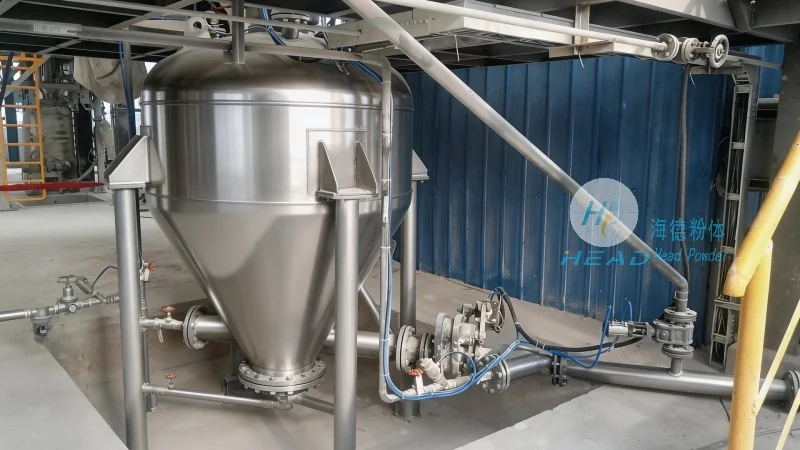
Vacuum material handling, also known as vacuum conveying, is a method of transporting bulk materials through a sealed pipeline using differential pressure. The process involves creating a vacuum in the receiving container or hopper, which draws material from a source, such as a silo or a bin, into the pipeline. The material is then transported to the destination, where the pressure is released, allowing the material to discharge. This technology is widely used in industries like pharmaceuticals, food processing, chemicals, and manufacturing, where handling delicate or abrasive materials requires a gentle and controlled approach.
At the core of any vacuum material handling system are several critical components that work in harmony to ensure smooth operation. These include the vacuum pump, which generates the necessary suction force; the conveying line, typically made of stainless steel or other corrosion-resistant materials to handle various materials; the inlet and outlet valves, which control the flow of material; and the filter or separator, which prevents dust and particles from entering the vacuum pump and ensuring clean operation. Additionally, many systems incorporate a rotary valve or a feeder to regulate the flow rate and prevent backflow, enhancing the overall efficiency and safety of the process.
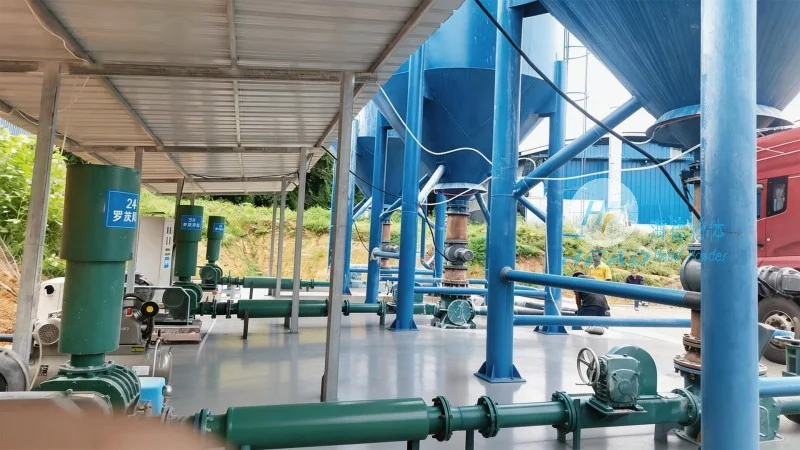
The design of a vacuum material handling system is crucial for achieving optimal performance, efficiency, and reliability. Several key principles guide the engineering and implementation of these systems. First, the system must be designed to handle the specific characteristics of the material being conveyed, such as particle size, density, and moisture content. This involves selecting the appropriate vacuum pump size and conveying line diameter to ensure adequate airflow and pressure. Second, the system should minimize pressure drop and energy consumption by optimizing the pipeline layout and using smooth, low-friction components. This includes avoiding sharp bends and using appropriate elbows or bends to maintain the material's flow without causing blockages or degradation. Third, the system must incorporate safety features, such as pressure relief valves and overpressure protection, to prevent accidents and ensure compliance with industrial safety standards. Finally, the design should allow for easy maintenance and cleaning, as many vacuum systems are used with materials that can cause clogging or contamination.
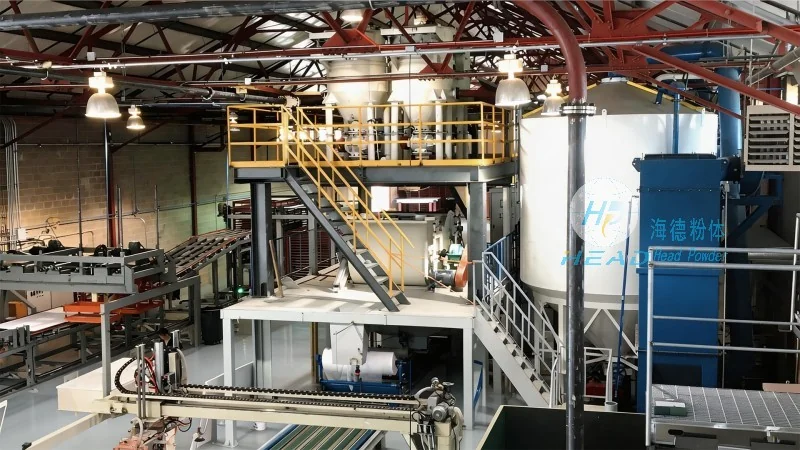
Vacuum material handling systems offer numerous benefits across a wide range of applications. One of the primary advantages is the gentle handling of delicate materials, which prevents breakage or degradation during transport. This is particularly important in industries like pharmaceuticals, where product integrity is paramount. Additionally, vacuum systems are highly efficient in terms of energy consumption compared to traditional methods like belt conveyors or pneumatic systems, as they use less air and require less maintenance. The sealed pipeline design also helps to contain dust and prevent contamination, making them suitable for applications where hygiene and environmental control are critical. Furthermore, these systems can handle a wide variety of materials, from fine powders to large bulk items, making them versatile and adaptable to different production needs.
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading provider of vacuum material handling solutions. With a strong commitment to innovation and quality, HeadPowder specializes in designing and manufacturing customized vacuum systems tailored to the unique needs of its clients. The company's team of experienced engineers and technicians works closely with customers to understand their material handling challenges and develop effective solutions that enhance productivity and efficiency. HeadPowder's products are known for their durability, reliability, and adherence to industry standards, making them a trusted choice for businesses in various sectors. With a focus on customer satisfaction and continuous improvement, HeadPowder continues to be at the forefront of vacuum material handling technology, helping industries achieve better results and meet their operational goals.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top