Dust-free automatic material handling systems have become increasingly vital in modern industrial and manufacturing environments. These sophisticated solutions are engineered to transport materials with minimal or no contamination, ensuring product integrity and operational efficiency. Understanding the core components and design principles behind such systems is crucial for businesses seeking to optimize their workflows and maintain stringent quality standards.
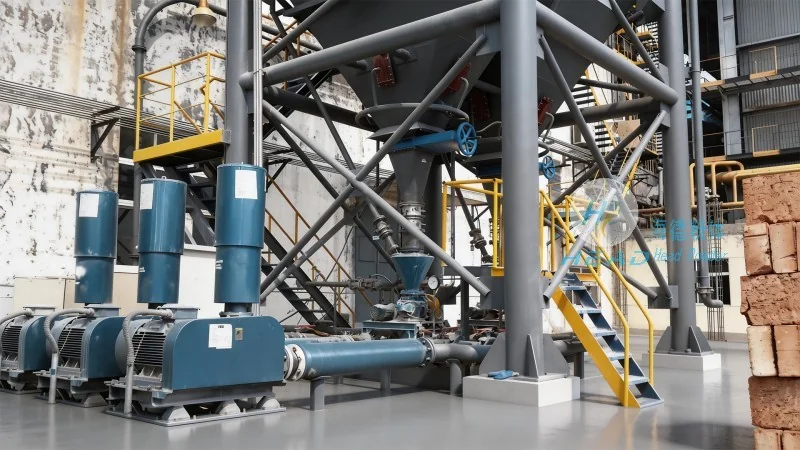
The foundation of any effective dust-free material handling system lies in its integrated components, each designed to minimize particle generation and prevent contamination. Key elements typically include enclosed conveyor systems, dust extraction mechanisms, and specialized material handling equipment. Enclosed conveyors, such as belt or chain conveyors, are often enclosed in airtight housings to contain dust and prevent it from escaping into the environment. Additionally, these systems may incorporate filtration and air purification units to ensure that any residual particles are captured before they can contaminate the workspace or materials being transported.
Another critical component is the material handling equipment itself, which may include automated guided vehicles (AGVs), robotic arms, or palletizers. These devices are designed to interact with materials in a controlled manner, reducing the risk of dust generation during loading, unloading, or sorting processes. For example, robotic palletizers can stack boxes or containers with precision, minimizing vibrations and friction that could otherwise generate dust particles.
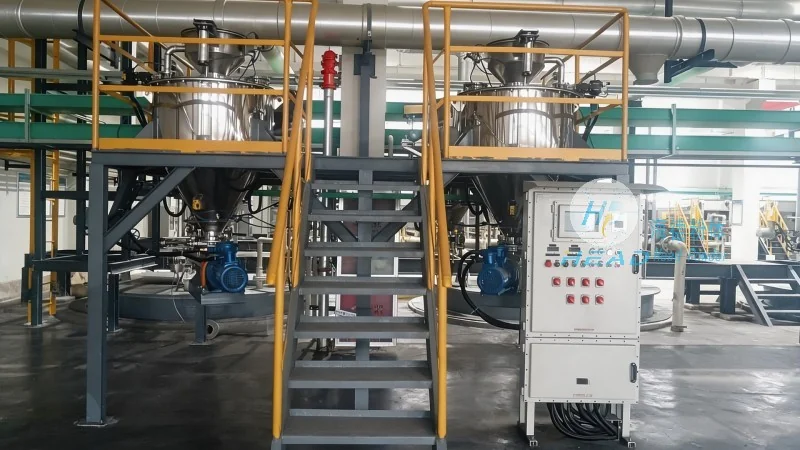
The design of dust-free material handling systems follows several key principles to ensure reliability and efficiency. One primary principle is the use of enclosed and sealed systems, which prevent dust from entering or exiting the system. This is achieved through robust housing materials, such as stainless steel or high-grade plastics, and tight-fitting seals that maintain a controlled internal environment. Additionally, the systems often incorporate negative pressure or filtered air circulation to keep the internal air clean and prevent contamination from external sources.
Another important design principle is the integration of dust extraction and filtration. Many systems are equipped with high-efficiency particulate air (HEPA) filters or other advanced filtration technologies that capture fine particles, ensuring that the air within the system remains clean. This not only protects the materials being handled but also safeguards the health and safety of personnel working in the area.
Efficiency is also a critical design consideration. Dust-free systems are engineered to minimize energy consumption while maintaining high throughput. This is achieved through optimized conveyor speeds, energy-efficient motors, and intelligent control systems that adjust operations based on real-time demand. For instance, variable frequency drives (VFDs) can adjust motor speed to match the required load, reducing energy waste and extending equipment lifespan.
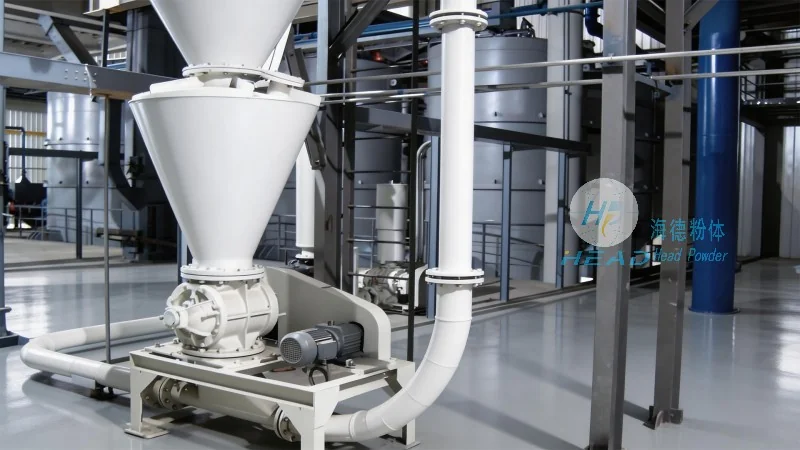
Dust-free automatic material handling systems find applications across a wide range of industries, including pharmaceuticals, food processing, electronics manufacturing, and cleanroom environments. In these sectors, maintaining a contamination-free environment is non-negotiable, as even minute dust particles can compromise product quality or safety. The benefits of such systems extend beyond just cleanliness; they also enhance operational efficiency, reduce downtime due to contamination-related issues, and improve overall productivity.
In pharmaceutical manufacturing, for example, dust-free systems are essential for handling raw materials and finished products to prevent cross-contamination and ensure compliance with regulatory standards. Similarly, in food processing facilities, these systems help maintain hygiene standards and prevent the spread of allergens or contaminants. The result is higher product quality, reduced waste, and increased customer trust.
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading provider of advanced material handling solutions tailored to meet the demands of modern industries. With a focus on innovation and precision engineering, HeadPowder specializes in designing and manufacturing dust-free automatic material handling systems that deliver superior performance and reliability. The company's headquarters is located in Shandong, China, where it leverages local expertise and resources to develop cutting-edge technologies that address the evolving needs of global markets.
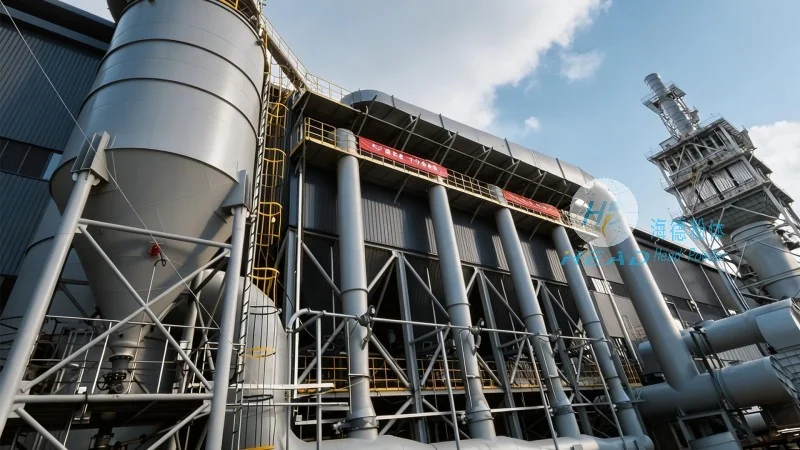
HeadPowder's commitment to quality is evident in its adherence to international standards and rigorous testing protocols. The company's products are engineered to withstand harsh industrial conditions while maintaining optimal performance. By integrating state-of-the-art materials and design principles, HeadPowder ensures that its systems not only meet but exceed industry expectations, providing customers with durable, efficient, and contamination-free material handling solutions.
For businesses seeking to enhance their operational efficiency and maintain stringent quality standards, HeadPowder offers comprehensive solutions that combine advanced technology with expert engineering. Whether for new installations or system upgrades, HeadPowder's team of professionals works closely with clients to understand their specific requirements and deliver customized solutions that align with their operational goals. With a strong presence in the industry and a reputation for excellence, HeadPowder continues to be a trusted partner for companies looking to optimize their material handling processes and achieve sustainable growth.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top