Positive pressure dilute phase pneumatic conveying is a critical industrial process used for transporting bulk materials over long distances with high efficiency and minimal product degradation. This method involves the use of compressed air to move particulate materials through a pipeline system, where the material is suspended in a dilute phase of air, ensuring smooth and continuous flow. Understanding the fundamentals of this technology, along with its design principles, is essential for industries that rely on reliable material handling solutions, particularly those served by companies like Shandong HeadPowder Engineering Co., Ltd.
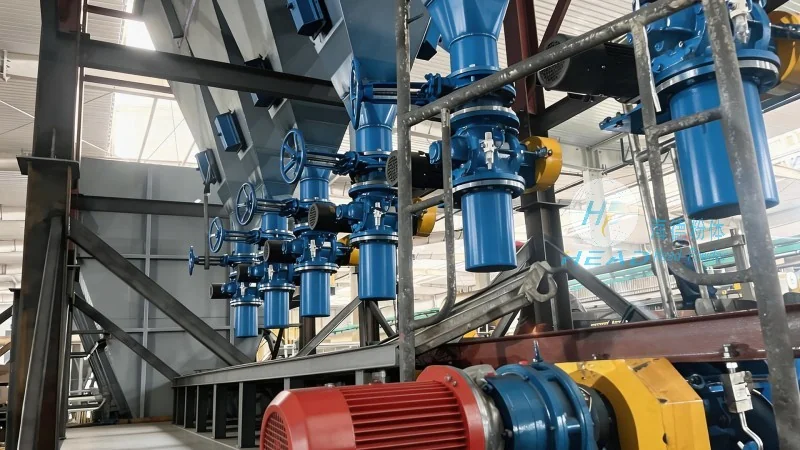
At its essence, positive pressure dilute phase conveying operates by injecting high-pressure air into a hopper or feeder, where bulk materials are introduced. The compressed air then lifts and transports the material through the pipeline, maintaining a consistent flow rate. Unlike negative pressure systems, which draw material into a vacuum, positive pressure systems push material forward, reducing the risk of clogging and improving overall system reliability. This method is particularly effective for transporting fine powders, granules, and other particulate materials that are prone to agglomeration or degradation under negative pressure conditions.
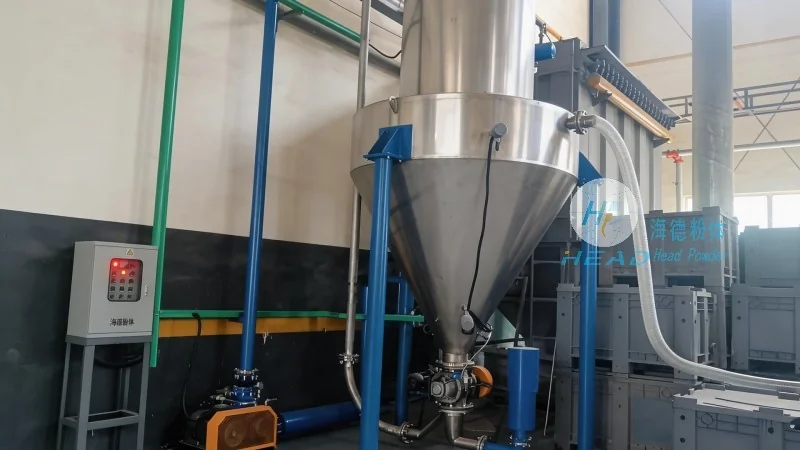
The design of a positive pressure dilute phase conveying system requires careful consideration of several critical factors to ensure optimal performance and longevity. First, the selection of appropriate air pressure and flow rate is paramount. The air pressure must be sufficient to lift and transport the material through the entire pipeline, accounting for elevation changes, pipe length, and material characteristics. Engineers typically use empirical formulas and material-specific data to determine the required air velocity, which is often maintained at a level that keeps the material in a suspended state, preventing settling or blockages. Second, the system's component selection is crucial. High-quality, corrosion-resistant materials are used for the hopper, feeder, and pipeline to withstand the abrasive nature of many bulk materials. Additionally, the inclusion of features such as in-line mixers, cyclones, and filter systems helps maintain material quality and system efficiency. Third, the layout of the pipeline is a key design consideration. The system is typically designed with a straight-line configuration to minimize pressure losses and ensure smooth material flow. However, for complex layouts, engineers incorporate pressure relief valves and surge tanks to manage pressure fluctuations and prevent system overloads. Finally, the integration of monitoring and control systems allows for real-time adjustment of air pressure and flow rate, enhancing system responsiveness and reducing downtime.
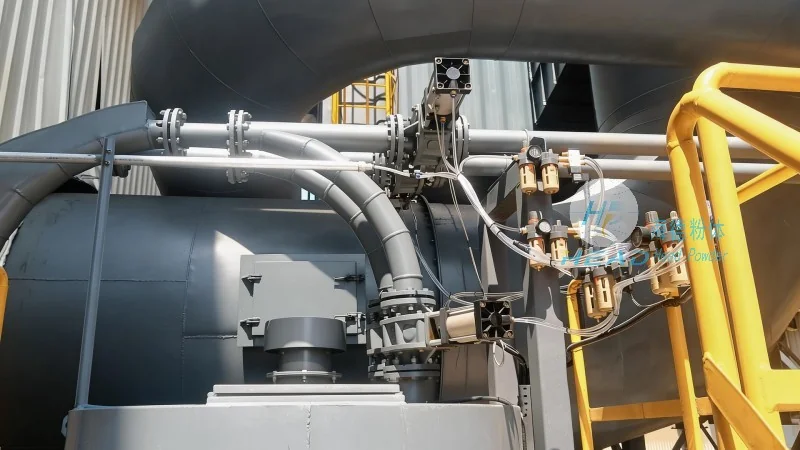
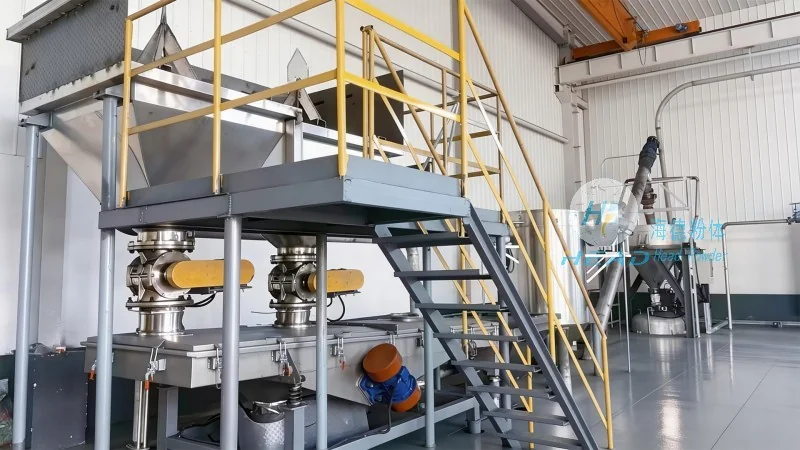
In practice, a positive pressure dilute phase conveying system begins with the material being fed into a hopper equipped with a rotary valve or screw feeder. The feeder regulates the material flow rate, ensuring a consistent supply to the conveying line. Compressed air is then introduced into the hopper, creating a high-pressure environment that lifts the material. As the material enters the pipeline, it is suspended in the air stream, traveling through the system at a controlled velocity. The pipeline may include bends, elbows, and other components, but the design ensures that the air velocity remains high enough to keep the material in suspension. At the discharge end, the material is separated from the air using a cyclone or filter system, and the air is either recirculated or vented to the atmosphere. The system's performance is monitored through pressure gauges, flow meters, and material level indicators, allowing operators to adjust settings as needed to maintain optimal operation. This continuous process ensures that bulk materials are transported efficiently and safely, with minimal product loss or degradation.
Shandong HeadPowder Engineering Co., Ltd., a leading engineering firm based in Shandong, China, specializes in the design, development, and implementation of advanced material handling systems, including positive pressure dilute phase conveying solutions. With a strong focus on innovation and customer satisfaction, HeadPowder has established itself as a trusted partner for industries seeking efficient and reliable bulk material transportation. The company's team of experienced engineers leverages cutting-edge technology and industry best practices to tailor conveying systems to the specific needs of each client. By integrating state-of-the-art components and rigorous testing protocols, HeadPowder ensures that its systems deliver optimal performance, durability, and safety. The company's commitment to quality is reflected in its adherence to international standards and its dedication to providing comprehensive after-sales support, including maintenance, spare parts, and technical assistance. Through its expertise and customer-centric approach, Shandong HeadPowder Engineering Co., Ltd. plays a pivotal role in advancing the efficiency and sustainability of material handling processes across various industries.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top