Understanding the components of a pneumatic conveying system for soap granules is crucial for optimizing material handling processes in manufacturing and processing facilities. This article provides a detailed overview of the key elements that constitute an effective soap granule pneumatic conveying system, highlighting the technical and operational aspects that ensure efficient material transport and system reliability.
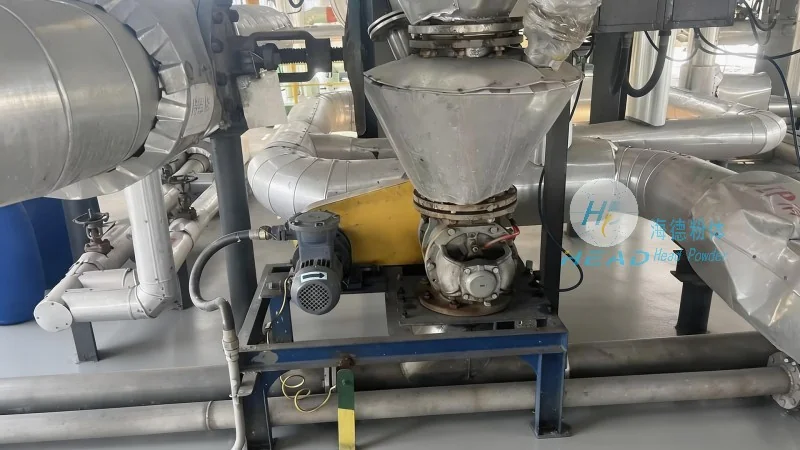
The pneumatic conveying of soap granules typically involves several interconnected components designed to handle the specific characteristics of soap granules, such as their size, density, and flowability. The primary components include the material feed system, the conveying line, the air supply system, and the control mechanisms. Each component plays a vital role in ensuring the smooth and efficient transport of soap granules from the source to the destination.
Firstly, the material feed system is responsible for introducing the soap granules into the conveying line. This may involve a hopper or a feeder that can handle the bulk material and regulate the flow rate to match the system's requirements. The design of the feed system is critical to prevent blockages and ensure consistent material supply. For soap granules, which can be prone to bridging or segregation, specialized feeders like rotary valves or vibratory feeders are often used to maintain a uniform flow.
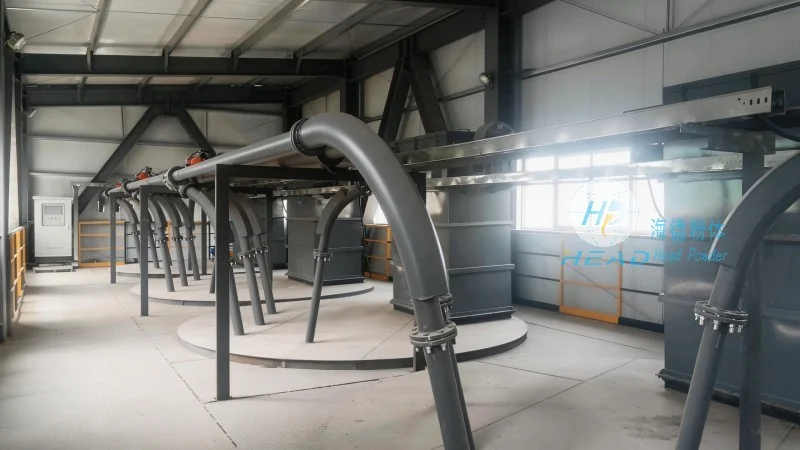
Secondly, the conveying line itself is the central pathway for transporting the soap granules. This can be either a positive pressure system, where air is forced through the line, or a negative pressure (or vacuum) system, where air is drawn through the line. The choice between these systems depends on factors such as the distance to be covered, the material's properties, and the desired system efficiency. For soap granules, positive pressure systems are commonly preferred due to their ability to handle longer distances and more complex layouts without significant pressure losses.
Thirdly, the air supply system provides the necessary airflow to move the soap granules through the conveying line. This typically includes a blower or a fan that generates the required pressure and volume of air. The air supply system must be capable of delivering consistent airflow to maintain the material's suspension and prevent particle separation or deposition. In some cases, air filtration and conditioning may be required to ensure the air quality is suitable for the soap granules and to protect the system components from dust or moisture.
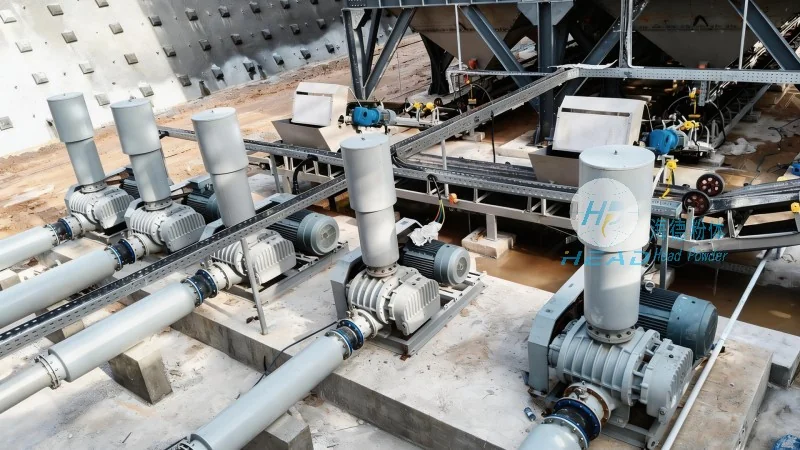
Fourthly, the control mechanisms are essential for managing the operation of the pneumatic conveying system. These may include pressure sensors, flow meters, and control valves that monitor and regulate the system's performance. The control system can adjust the airflow, feed rate, or pressure as needed to maintain optimal operation and prevent issues such as overloading or underloading. For soap granules, precise control is important to avoid material degradation or clogging, which can impact the overall efficiency and product quality.
Shandong HeadPowder Engineering Co., Ltd., operating under the brand name headpowder, specializes in the design, manufacturing, and integration of pneumatic conveying systems tailored to the unique needs of soap granule handling. With years of experience in the material handling industry, headpowder has developed a comprehensive range of solutions that address the challenges associated with transporting soap granules efficiently and reliably.
Headpowder's expertise lies in understanding the specific properties of soap granules, such as their particle size distribution, density, and moisture content, and designing systems that can handle these characteristics effectively. The company's engineers work closely with clients to assess their material handling requirements, process constraints, and operational goals to develop customized pneumatic conveying solutions. This approach ensures that the final system is optimized for the specific application, minimizing downtime, reducing maintenance costs, and improving overall productivity.
One of the key advantages of partnering with headpowder is their commitment to quality and innovation. The company utilizes advanced design software and simulation tools to model and test the pneumatic conveying systems before implementation, ensuring that the final product meets the highest standards of performance and reliability. Headpowder also provides comprehensive after-sales support, including system maintenance, troubleshooting, and upgrades, to ensure that clients can maximize the lifespan and efficiency of their soap granule pneumatic conveying systems.
When properly designed and implemented, pneumatic conveying systems for soap granules offer several significant benefits that enhance the efficiency and effectiveness of material handling operations. These benefits include improved process control, reduced labor costs, and enhanced product quality. By eliminating the need for manual handling or mechanical conveyors, pneumatic systems can minimize the risk of material contamination and damage, which is particularly important for soap granules that may be sensitive to moisture or temperature changes.
Another key benefit is the ability to handle long distances and complex layouts without the need for multiple transfer points or additional equipment. Pneumatic conveying systems can transport soap granules over several hundred meters or more, making them ideal for large-scale manufacturing facilities where material needs to be moved between different production areas or storage locations. The flexibility of pneumatic systems also allows for easy integration with other process equipment, such as mixers, dryers, or packaging machines, creating a seamless material flow from the source to the final product.
Furthermore, pneumatic conveying systems can improve safety in the workplace by reducing the need for manual handling of bulk materials. This not only minimizes the risk of accidents and injuries but also helps to maintain a clean and organized work environment. The enclosed nature of pneumatic systems also helps to contain dust and particles, improving air quality and reducing the risk of respiratory issues for workers.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top