Urea pneumatic conveying systems are complex yet efficient solutions for transporting urea, a critical fertilizer, from production sites to distribution points. Understanding the key components that make up such a system is essential for optimizing performance, ensuring safety, and maintaining operational efficiency. This article will explore the primary elements that constitute a typical urea pneumatic conveying setup, providing insights into how each component contributes to the overall functionality of the system.
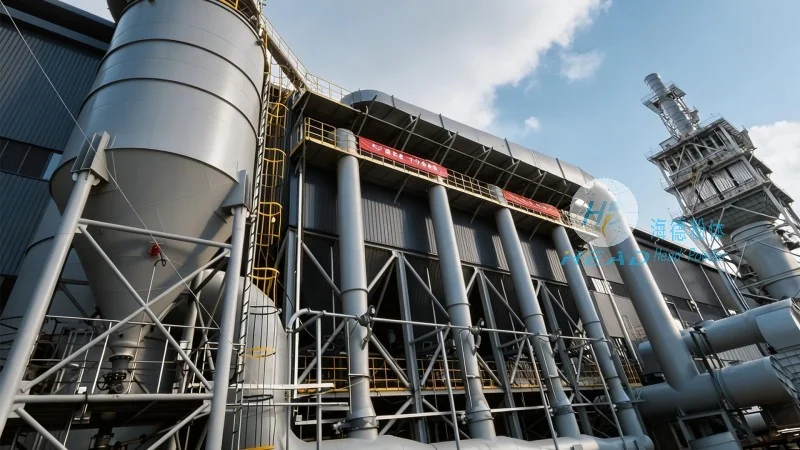
The core components of a urea pneumatic conveying system are designed to handle the unique properties of urea, including its granular nature, dust potential, and the need for controlled flow. These components work in tandem to ensure reliable and safe transportation. The main elements typically include:
The urea hopper serves as the storage and feeding unit for the material. It is designed to hold a sufficient quantity of urea to support continuous operation, with dimensions and capacity tailored to the specific production and conveying requirements. The feeder, often a rotary valve or a screw feeder, regulates the flow of urea from the hopper into the conveying line. This component is critical for maintaining a consistent feed rate, which directly impacts the system's throughput and overall efficiency. The hopper and feeder are usually constructed from materials resistant to urea's chemical properties, such as stainless steel or specialized coatings, to prevent corrosion and material degradation.
The conveying line, typically made of high-quality plastic or metal tubing, forms the pathway for the urea particles. The choice of material depends on factors like the urea's abrasiveness, the required pressure, and the system's operating conditions. The tubing is often equipped with bends and elbows that are carefully designed to minimize pressure loss and prevent material buildup. In some systems, the line may include sections with internal coatings or liners to enhance durability and reduce friction. The length and diameter of the tubing are calculated based on the system's capacity and the distance between the hopper and the discharge point, ensuring optimal performance without excessive energy consumption.
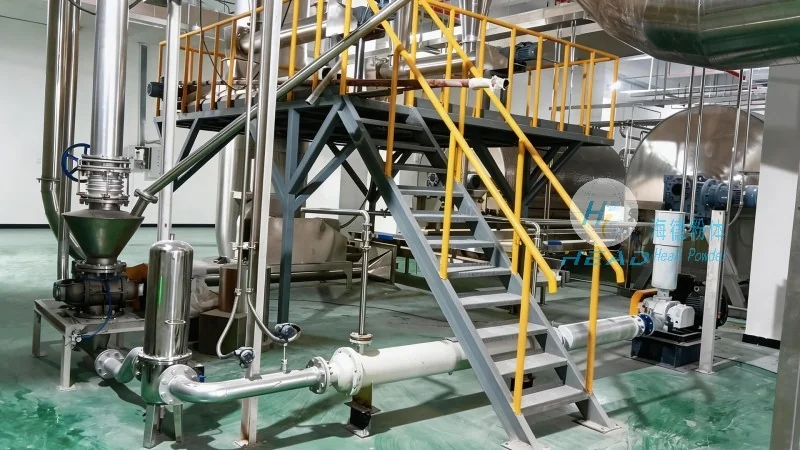
The air supply system is a vital component that provides the necessary pressure and volume of air to move the urea particles through the conveying line. The blower or compressor generates the airflow, which can be either positive or negative pressure, depending on the system design. Positive pressure systems force air into the line, pushing the urea particles forward, while negative pressure systems create a vacuum that pulls the material through the line. The blower's capacity and pressure rating are determined by the system's required airflow rate and the pressure drop across the conveying line. Efficient air management is crucial to minimize energy consumption and ensure consistent material transport. The system may also include air filters and moisture separators to maintain air quality and prevent contamination of the urea.
Urea pneumatic conveying systems often incorporate solids handling equipment to manage any potential blockages or material accumulation. This may include cyclones or separators that separate the urea particles from the air stream, allowing the air to be recycled or vented while the urea is collected for further processing. The design of these components is critical to prevent material buildup and ensure smooth operation. In some cases, the system may include a rotary valve or a rotary airlock at the discharge end to control the flow of urea into the receiving hopper or storage silo. This equipment helps maintain a consistent discharge rate and prevents overfilling or underfilling of the receiving container.
Modern urea pneumatic conveying systems are equipped with advanced control and monitoring systems to ensure optimal performance and safety. These systems may include sensors for pressure, flow, and level, as well as control panels that allow operators to adjust system parameters in real-time. The control system can monitor the entire conveying process, from the hopper feed to the discharge, and alert operators to any deviations or issues that may affect performance. This level of automation helps reduce downtime, improve efficiency, and enhance safety by preventing overpressure or material blockages. The monitoring data can also be used for maintenance planning and system optimization, ensuring the system operates at peak performance over its lifespan.
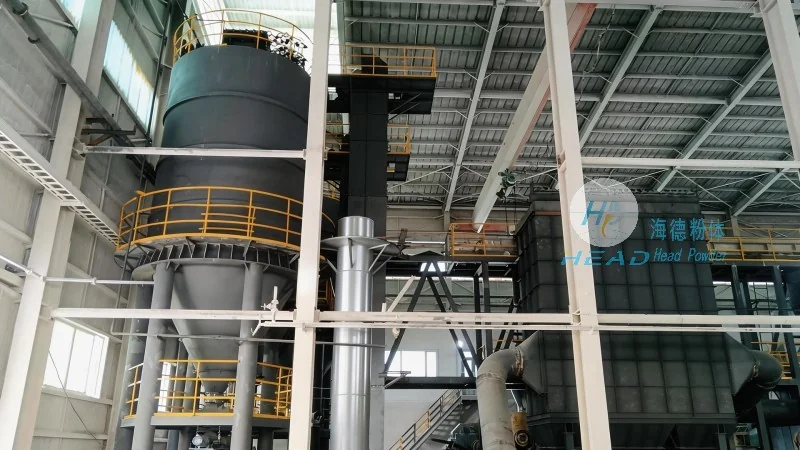
Given the nature of urea as a fine, dust-like material, safety and environmental considerations are paramount in pneumatic conveying systems. The system is designed with features to minimize dust emissions and prevent the release of urea particles into the environment. This may include dust collection systems, such as baghouses or cartridge filters, that capture any airborne urea particles and return them to the conveying line. The system may also include explosion-proof components and emergency shut-off valves to prevent accidents and ensure operator safety. Compliance with local regulations regarding dust control and material handling is essential for maintaining a safe and environmentally responsible operation.
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading provider of engineering solutions for material handling systems, including urea pneumatic conveying. With a focus on innovation and customer-centric design, HeadPowder specializes in developing customized solutions that meet the specific needs of clients in the fertilizer industry. The company's expertise lies in the design, manufacturing, and installation of high-quality pneumatic conveying systems, ensuring reliable and efficient transport of urea from production to distribution. HeadPowder's commitment to quality and safety is reflected in their adherence to industry standards and rigorous testing protocols, which help ensure the longevity and performance of their systems. The company's location in Shandong, China, provides access to a skilled workforce and advanced manufacturing capabilities, enabling them to deliver competitive and reliable solutions to clients worldwide.
In summary, a urea pneumatic conveying system comprises several key components, each playing a critical role in the efficient and safe transport of urea. From the hopper and feeder to the air supply and solids handling equipment, every element is designed to work together to optimize performance and minimize operational challenges. The integration of advanced control systems and safety features further enhances the reliability and efficiency of these systems. For businesses in the fertilizer industry seeking to improve their material handling processes, understanding the components of a urea pneumatic conveying system is essential. Companies like Shandong HeadPowder Engineering Co., Ltd. offer specialized expertise and customized solutions to meet these needs, ensuring that clients can achieve optimal performance and operational efficiency in their urea transport operations.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top