Xiaomixi pneumatic conveying systems, provided by Shandong HeadPowder Engineering Co., Ltd., are engineered to efficiently transport bulk materials through a pressurized air system. The comprehensive design of these systems ensures reliability and performance in various industrial applications. Understanding the key components is essential for optimizing operation and maintenance.
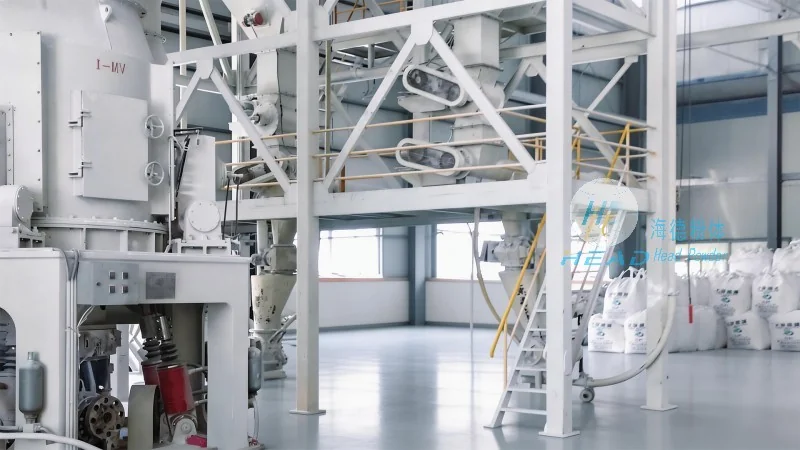
The core elements of a Xiaomixi pneumatic conveying system include several critical components that work in tandem to facilitate material transport. These components are meticulously designed to handle diverse material characteristics and operational requirements.
The feeding and metering unit is the initial stage of the system, responsible for introducing bulk materials into the conveying line. This component ensures consistent material flow by controlling the rate at which materials are fed into the system. For different material types, such as powders or granules, specialized feeders like rotary valves or screw feeders may be employed to maintain uniformity and prevent blockages. The metering unit plays a crucial role in regulating the material quantity, which directly impacts the system's efficiency and overall throughput.
The air supply and compressing system is another vital component, responsible for generating the necessary pressure and airflow to move materials through the pipeline. Typically, this system includes an air compressor, air dryer, and filtration equipment. The air compressor boosts the air pressure to the required level, while the dryer removes moisture to prevent material clumping or equipment corrosion. Filtration systems ensure that the air is clean, protecting both the material and the conveying components from contaminants. The efficiency of the air supply system directly influences the system's energy consumption and operational stability.
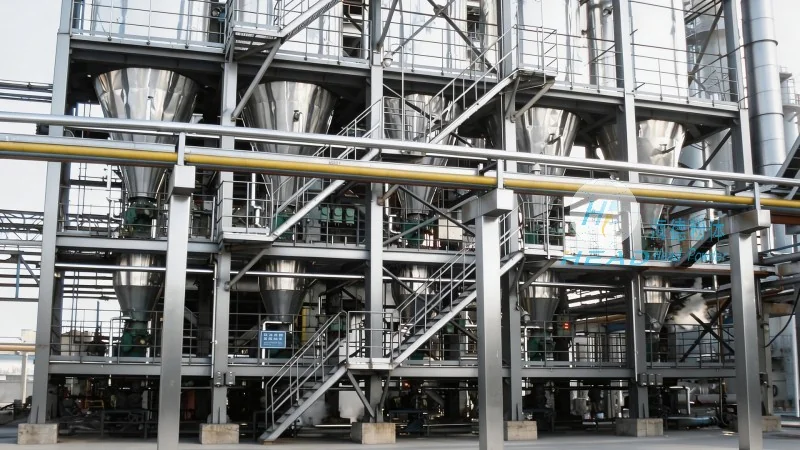
The conveying pipeline forms the main pathway for material transport within the system. Made from durable materials like stainless steel or plastic, the pipeline is designed to withstand the pressure and friction generated during material movement. The choice of tubing material depends on the material being conveyed, as well as the operating conditions. For abrasive or corrosive materials, stainless steel is preferred for its resistance to wear and chemical attack. The pipeline is typically arranged in a loop or straight configuration, with appropriate bends and elbows to guide the material flow. Proper sizing of the pipeline is essential to maintain optimal air velocity and prevent material deposition or blockages.
The material separation and collection unit is the final stage of the system, responsible for separating the conveyed material from the air and collecting it in a designated container. This component includes a cyclone separator or a baghouse filter, depending on the material's properties. The cyclone separator uses centrifugal force to separate particles from the air stream, while the baghouse filter captures fine particles through a series of fabric bags. The collected material is then discharged into a storage bin or silo. The efficiency of the separation unit is critical to maintaining material purity and preventing dust emissions, which is essential for compliance with environmental regulations.
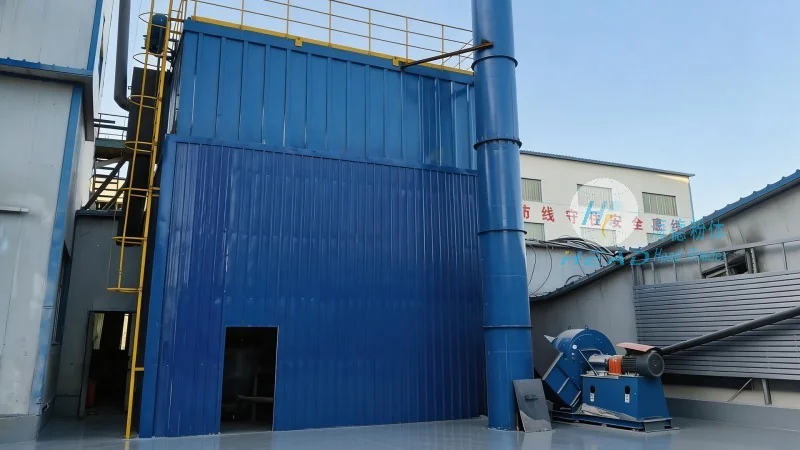
The control and monitoring system provides the necessary automation and oversight to ensure the pneumatic conveying system operates smoothly. This component includes sensors, control panels, and programmable logic controllers (PLCs). Sensors monitor parameters such as pressure, flow rate, and temperature, providing real-time data to the control system. The PLCs manage the operation of various components, such as the feeder and compressor, based on the input from sensors. The control system allows for remote monitoring and adjustment, enabling operators to optimize performance and troubleshoot issues quickly. Advanced control systems may also include features like automatic start-up and shutdown, as well as alarms for abnormal conditions.
In addition to the main components, Xiaomixi pneumatic conveying systems may include auxiliary equipment and accessories to enhance functionality and adaptability. These may include pressure relief valves, air filters, and vacuum pumps. Pressure relief valves prevent over-pressurization by releasing excess air when the system pressure exceeds a set limit. Air filters maintain the cleanliness of the air system, protecting components from dust and debris. Vacuum pumps are used in some systems to create a negative pressure environment for material suction. These auxiliary components contribute to the overall reliability and longevity of the system, ensuring consistent performance over time.
Shandong HeadPowder Engineering Co., Ltd. specializes in the design, manufacturing, and installation of Xiaomixi pneumatic conveying systems, with a focus on providing customized solutions tailored to specific industrial needs. The company's expertise in material handling and pneumatic technology ensures that each system is optimized for efficiency, durability, and safety. With a commitment to quality and customer satisfaction, HeadPowder delivers reliable solutions for a wide range of applications, including food processing, pharmaceuticals, and chemical industries. The comprehensive understanding of the system components, as outlined above, underscores the importance of each element in achieving successful material transport and operational excellence.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top