Efficient and reliable material handling is crucial in industrial processes, especially when dealing with bulk materials like anhydrous sodium sulfate. The equipment designed for transporting this chemical plays a vital role in ensuring smooth operations across various industries. This article explores the underlying principles of anhydrous sodium sulfate material handling systems and highlights the key characteristics of their operational environments.
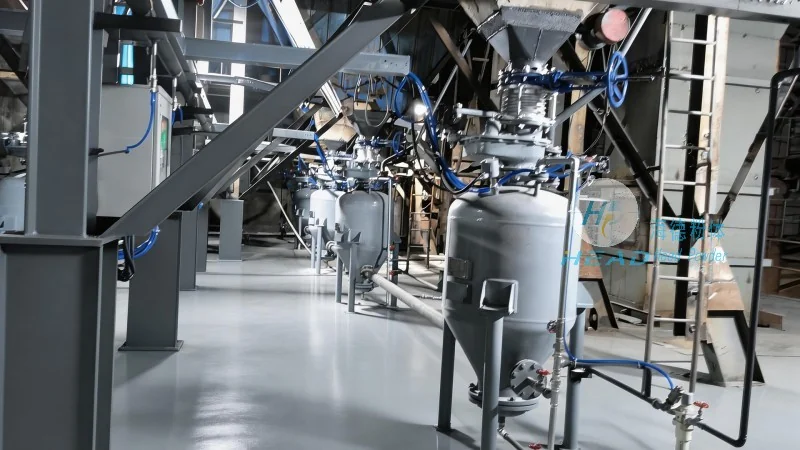
Anhydrous sodium sulfate, also known as Glauber's salt or white powder, is a widely used chemical in industries such as glass manufacturing, paper production, and chemical synthesis. Its handling requires specialized equipment to maintain safety, efficiency, and product integrity. The material handling systems for anhydrous sodium sulfate are engineered to address the unique properties of this substance, including its granular structure, flow characteristics, and potential for dust generation. By understanding the principles behind these systems, industries can optimize their processes and enhance overall productivity.
At Shandong HeadPowder Engineering Co., Ltd., we specialize in designing and manufacturing advanced material handling equipment tailored to the needs of various industries. With our headquarters located in Shandong, China, our team of experts combines years of experience and cutting-edge technology to deliver solutions that meet the highest standards of performance and reliability. Our commitment to quality and customer satisfaction has made us a trusted partner for businesses worldwide seeking efficient material handling systems for anhydrous sodium sulfate and other bulk materials.
The fundamental principle of anhydrous sodium sulfate material handling systems is to ensure the safe and efficient transport of the material from one point to another within a production facility. This involves several key components and operational strategies. First, the system must account for the material's physical properties, such as its density, particle size distribution, and angle of repose. These characteristics influence the choice of equipment, including conveyor belts, screw conveyors, and pneumatic systems. For example, belt conveyors are commonly used for horizontal and slight incline transport due to their ability to handle large volumes and maintain a consistent flow. Screw conveyors, on the other hand, are ideal for vertical or inclined transport, as they can lift and move material with minimal space requirements. Pneumatic conveying systems are often employed for dusty or fine materials, providing a dust-free and hygienic transport method.
Another critical principle is the integration of safety features to prevent accidents and protect personnel. Anhydrous sodium sulfate, while generally non-toxic, can cause respiratory issues if inhaled as dust. Therefore, the systems are equipped with dust suppression mechanisms, such as enclosed conveyor housings and dust collection systems. Additionally, the equipment is designed with robust construction to withstand the abrasive nature of the material, ensuring long-term durability and minimal maintenance.
The operational environments where anhydrous sodium sulfate material handling systems are deployed vary significantly, each presenting unique challenges and requirements. Understanding these characteristics is essential for selecting the right equipment and optimizing its performance.
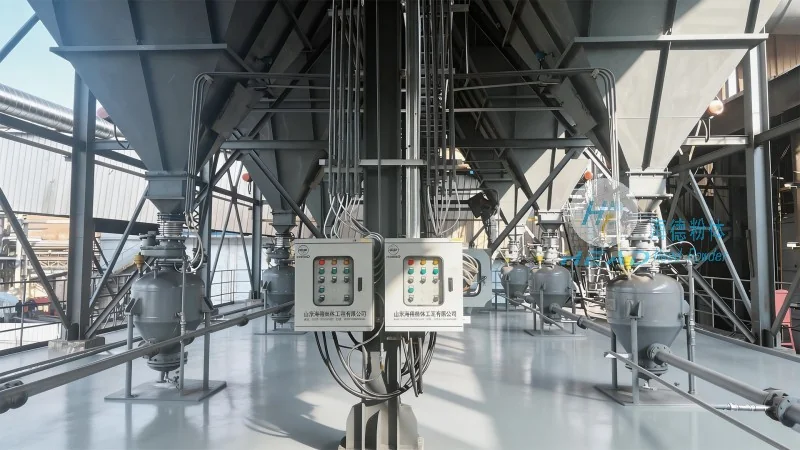
1. Industrial Manufacturing Plants: In glass manufacturing, anhydrous sodium sulfate is used as a flux to lower the melting point of silica. The material handling systems in these plants must be capable of handling large quantities of the chemical and integrating with existing production lines. The systems are often designed to operate continuously, with minimal downtime for maintenance. The conveyor systems are typically enclosed to prevent dust from contaminating the glass-making process and to protect workers from exposure.
2. Paper and Pulp Industries: Anhydrous sodium sulfate is used in the paper industry as a filler and a sizing agent. The material handling systems in these facilities must be able to handle the material in bulk and transport it to the paper-making machines. The systems are designed to maintain a consistent flow rate to ensure uniform distribution of the filler in the paper. Additionally, the equipment is often equipped with moisture control features to prevent the material from clumping or caking.
3. Chemical Production Facilities: In chemical synthesis, anhydrous sodium sulfate is used as a drying agent and a reagent. The material handling systems in these plants must be able to handle the material in various forms, including powder and granules. The systems are designed to integrate with other chemical processing equipment, such as reactors and distillation units. The equipment is also equipped with temperature control features to prevent the material from degrading or reacting with other chemicals.
4. Storage and Distribution Centers: In storage and distribution centers, anhydrous sodium sulfate is stored in bulk and transported to various locations. The material handling systems in these facilities are designed to handle large volumes of the material and ensure efficient loading and unloading from trucks and storage silos. The systems are equipped with safety features, such as load sensors and emergency stop buttons, to prevent accidents during handling.
HeadPowder's material handling systems for anhydrous sodium sulfate offer several advantages that make them ideal for industrial applications. These features include:
• Customizable Design: Our systems are designed to meet the specific requirements of each client, including the size of the material, the distance to be transported, and the operational environment. This ensures that the equipment is optimized for maximum efficiency and minimal downtime.
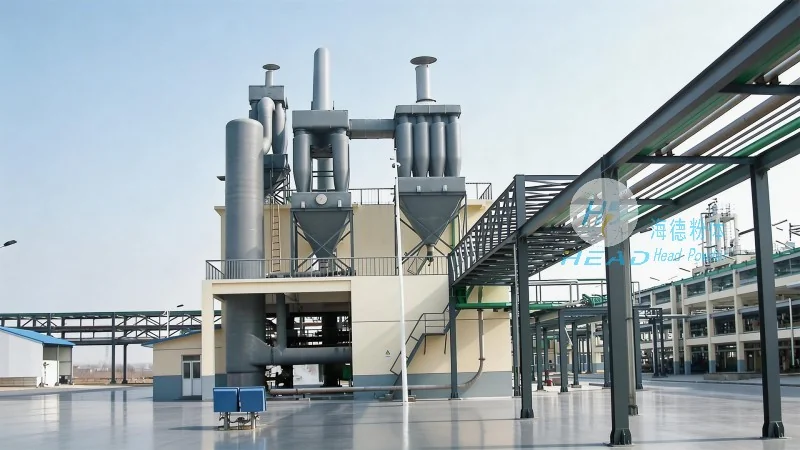
• Robust Construction: The equipment is constructed from high-quality materials, such as stainless steel and abrasion-resistant polymers, to withstand the harsh conditions of industrial use. This results in longer service life and lower maintenance costs.
• Advanced Control Systems: Our systems are equipped with advanced control systems that allow for precise control of the material flow rate and direction. This ensures consistent performance and reduces the risk of material buildup or blockages.
• Dust Suppression and Safety Features: The systems are designed with dust suppression mechanisms and safety features to protect workers and the environment. This includes enclosed conveyor housings, dust collection systems, and emergency stop buttons.
• Energy Efficiency: Our systems are designed to be energy-efficient, reducing operating costs and minimizing the environmental impact. This includes the use of variable speed drives and optimized conveyor designs.
Anhydrous sodium sulfate material handling systems are critical components of industrial processes, ensuring the efficient and safe transport of this important chemical. By understanding the principles behind these systems and the characteristics of their operational environments, industries can select the right equipment and optimize their operations. HeadPowder, with its expertise and commitment to quality, provides reliable and efficient material handling solutions that meet the needs of various industries. Whether for glass manufacturing, paper production, or chemical synthesis, our systems are designed to enhance productivity and ensure safety.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top