HeadPowder, a leading provider in the field, specializes in advanced solutions for efficient powder handling, particularly through pneumatic conveying systems integrated with ash silos. This article delves into the fundamental principles behind this technology and explores the key characteristics of its application scenarios.
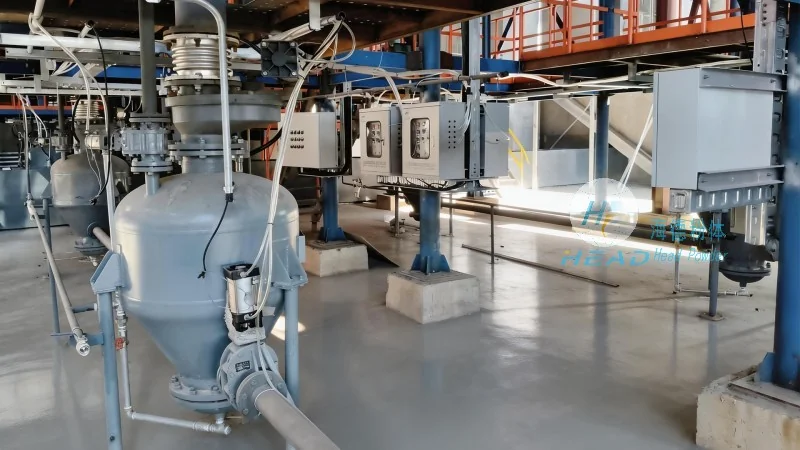
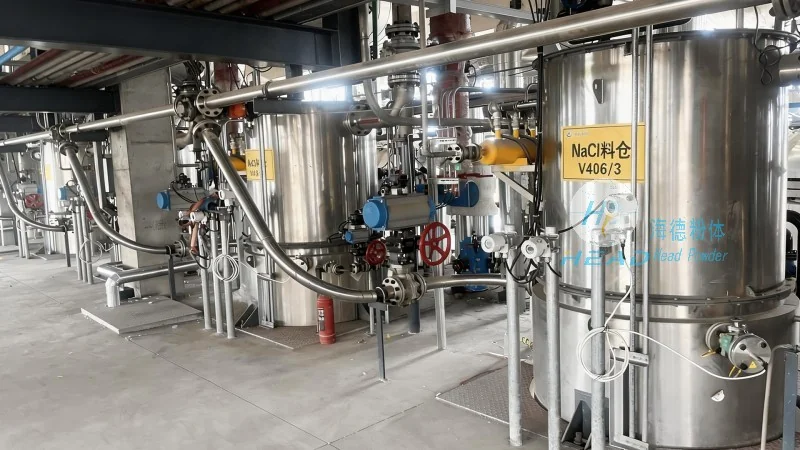
The pneumatic conveying system for ash silos operates on the principle of using compressed air to transport bulk powders, such as fly ash or other fine particulates, from the silo to downstream processing equipment. This method eliminates the need for mechanical components like conveyor belts or buckets, reducing maintenance costs and enhancing operational reliability. The system typically consists of several key components: the ash silo, a blower or compressor to generate the air flow, a conveying line, and a receiver or discharge point. The process begins when the silo is filled with the powder. As the air is introduced into the silo, it creates a low-pressure zone that draws the powder particles into the conveying line. The air then transports the powder through the line, maintaining a consistent flow by controlling the air pressure and velocity. The receiver at the end of the line collects the powder, completing the transfer. This principle ensures a smooth, continuous transfer of material, minimizing dust generation and ensuring compliance with environmental regulations.
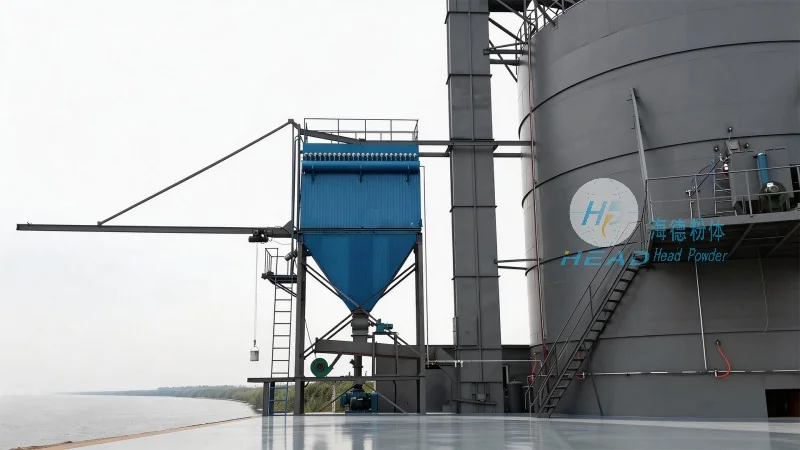
When considering the application of pneumatic conveying systems in ash silo operations, several distinct characteristics define the working scenarios. First, the system is highly adaptable to various ash types, including fly ash, bottom ash, and other industrial powders, making it versatile for different industrial settings. Second, the technology offers significant advantages in terms of space efficiency, as it requires minimal floor space compared to traditional mechanical conveyors. This is particularly beneficial in facilities with limited room for large equipment. Third, the system provides excellent dust control, which is crucial for maintaining a safe and clean working environment. The enclosed nature of the conveying line prevents dust from escaping into the air, reducing the risk of respiratory issues and environmental contamination. Fourth, the system enhances operational safety by eliminating the need for moving parts that could pose a hazard to personnel. The absence of exposed gears, belts, or chains minimizes the risk of accidents, making it suitable for environments where worker safety is a top priority. Additionally, the system offers flexibility in terms of layout, allowing for horizontal, vertical, or inclined conveying paths, which can be tailored to the specific geometry of the ash silo and the downstream processing equipment. This adaptability ensures that the system can be integrated seamlessly into existing infrastructure without major modifications.
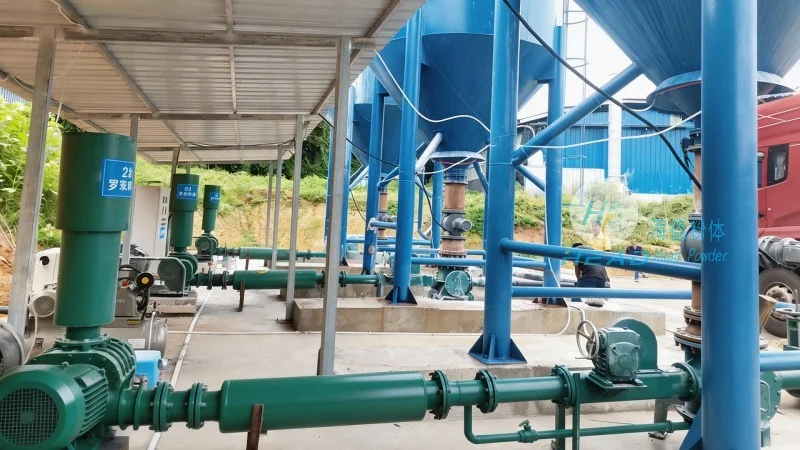
HeadPowder Engineering, based in Shandong, China, is a reputable company specializing in the design, manufacturing, and installation of advanced powder handling systems. With a focus on innovation and customer satisfaction, HeadPowder provides tailored solutions for various industrial applications, including ash silo pneumatic conveying. The company's expertise lies in developing efficient, reliable, and environmentally friendly systems that meet the diverse needs of its clients. By leveraging cutting-edge technology and adhering to strict quality standards, HeadPowder ensures that its products deliver optimal performance and long-term value. The company's commitment to excellence has earned it a strong reputation in the industry, making it a trusted partner for businesses seeking to improve their powder handling processes.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top