Grain silo pneumatic conveying systems are essential equipment in modern agricultural and food processing industries. These systems are designed to efficiently transport bulk materials such as grains, powders, and other dry products within storage facilities. The primary function of a pneumatic conveying system is to move materials from one location to another using air pressure or suction, eliminating the need for mechanical components like belts or buckets. This technology offers significant advantages in terms of hygiene, speed, and operational flexibility, making it a preferred choice for many food and grain handling operations.
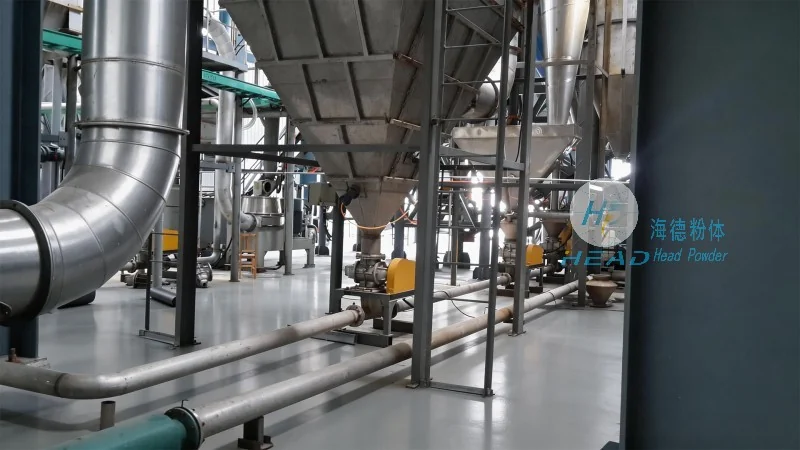
HeadPowder, a leading manufacturer based in Shandong, China, specializes in the design, manufacturing, and supply of advanced pneumatic conveying systems for grain silos. With years of experience in the industry, HeadPowder has established itself as a trusted partner for businesses seeking reliable and efficient material handling solutions. The company's commitment to quality and innovation ensures that their products meet the highest standards of performance and durability.
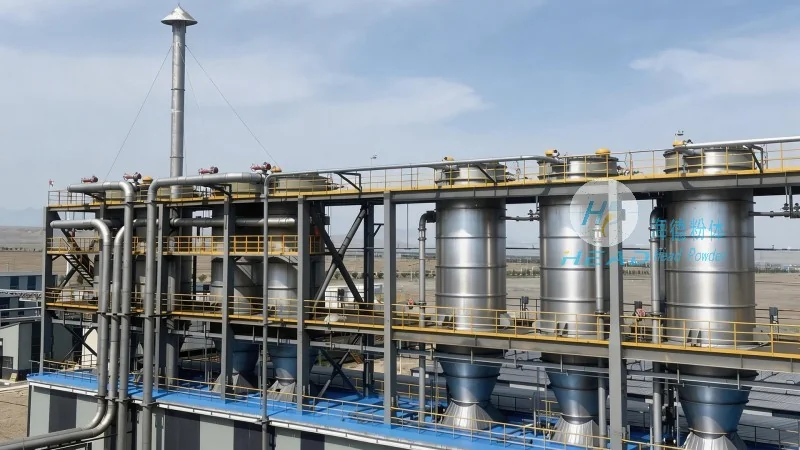
The design of a grain silo pneumatic conveying system involves several key principles that ensure optimal performance and efficiency. The system typically consists of a hopper, a conveying line, a control unit, and a discharge point. The hopper is where the material is stored and fed into the system. The conveying line, often made of stainless steel or other corrosion-resistant materials, transports the material using air pressure. The control unit manages the flow of air and material, ensuring smooth operation. The discharge point is where the material is released into the next stage of processing or storage.
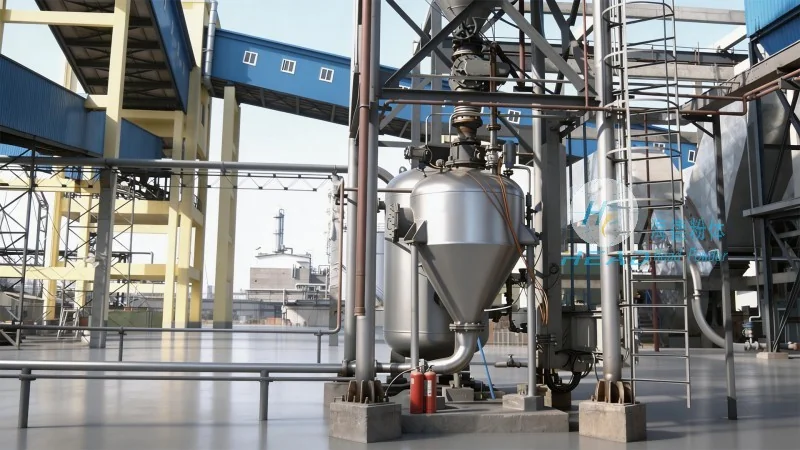
Each component of a pneumatic conveying system plays a crucial role in its overall operation. The hopper is responsible for storing the bulk material and providing a consistent feed to the system. The air compressor or blower generates the necessary air pressure to move the material through the conveying line. The filter and separator are used to remove any dust or debris from the air, ensuring clean operation and preventing contamination of the material. The control system, often equipped with sensors and automation, monitors the system's performance and adjusts the air flow as needed to maintain optimal conditions.
Compared to traditional mechanical conveying systems, pneumatic conveying offers several advantages. These include improved hygiene, as there are no moving parts that can come into contact with the material, reducing the risk of contamination. The systems are also more flexible, allowing for changes in the layout of the facility without major modifications. Additionally, pneumatic conveying systems can handle a wide range of materials, from fine powders to larger granules, with minimal maintenance requirements. The ability to operate in a closed system also helps in controlling dust and odors, making it suitable for food processing applications.
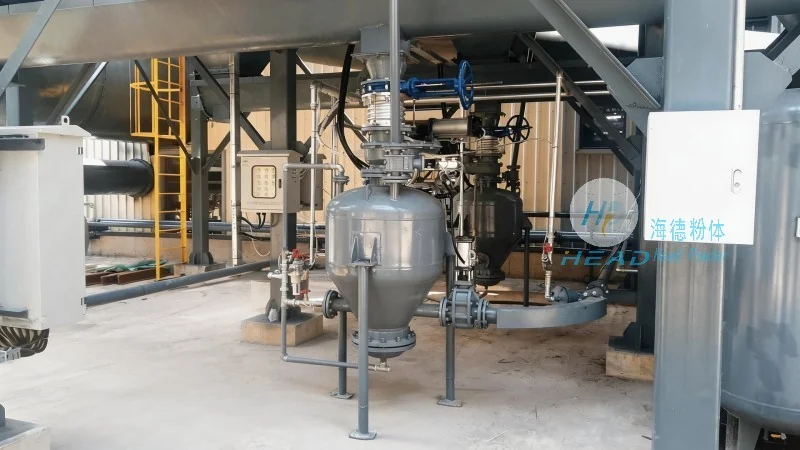
Grain silo pneumatic conveying systems are a vital part of modern material handling, offering efficient, hygienic, and flexible solutions for transporting bulk materials. HeadPowder, with its expertise and commitment to quality, provides reliable systems that meet the needs of various industries. By understanding the design principles and components of these systems, businesses can make informed decisions about implementing effective material handling solutions that enhance productivity and ensure product quality.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top