HeadPowder, a leading provider in the field of bulk material handling solutions, specializes in the design, manufacturing, and integration of advanced metering bin pump systems for pneumatic conveying applications. This article delves into the fundamental principles behind these systems and highlights the key working scene characteristics that make them indispensable in various industrial settings.
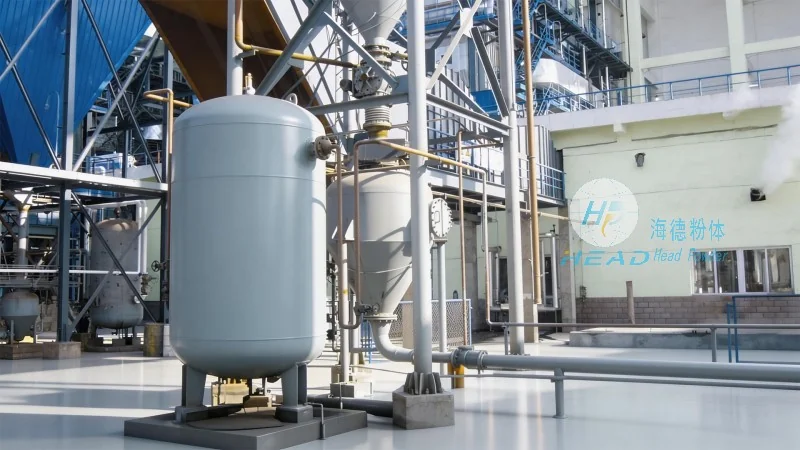
The metering bin pump, also known as a pressure bin or pressure vessel pump, operates on the principle of creating a pressure differential to transport dry bulk materials through a pipeline. Unlike traditional vacuum or pressure conveying systems, the metering bin pump combines the functions of a storage bin, a metering device, and a pump into a single, compact unit. This integration enhances efficiency and reduces the complexity of material handling processes.
At the heart of the system is a hopper or bin that stores the bulk material. The bin is equipped with a valve mechanism that controls the flow of material into the pump chamber. As the material is discharged from the bin, it falls into the pump's chamber, where it is compressed by a piston or diaphragm. The compression process increases the pressure within the chamber, forcing the material through the conveying pipeline to the destination point. The metering function is achieved by precisely controlling the volume of material entering the pump chamber, ensuring consistent and controlled flow rates.
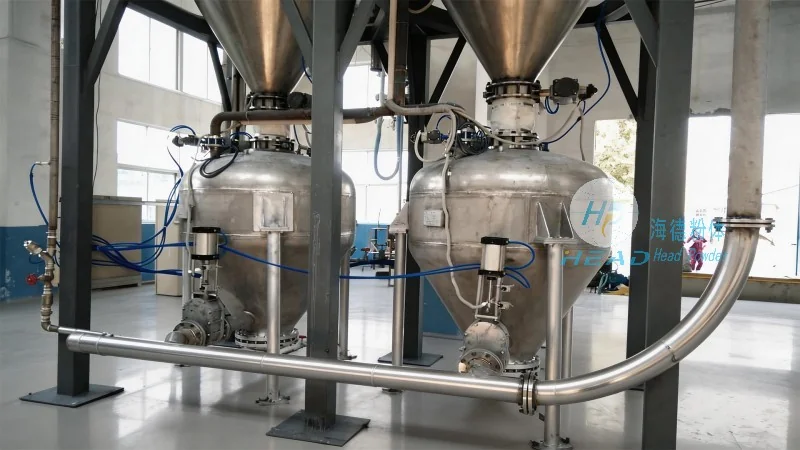
One of the most significant advantages of metering bin pumps is their ability to handle a wide range of dry bulk materials, including powders, granules, and fine particles. This versatility makes them suitable for diverse industrial applications, from chemical processing and pharmaceutical manufacturing to food processing and mining operations. The equipment's design allows for the handling of materials with varying flow properties, such as cohesive or non-cohesive powders, without the need for extensive modifications.
A critical working scene characteristic is the system's ability to maintain a consistent flow rate, even under varying pressure conditions. This is achieved through the precise metering mechanism, which ensures that the material is discharged at a controlled rate, preventing overloading or underloading of the conveying pipeline. The consistent flow rate is particularly important in applications where process control is essential, such as in chemical reactions or food production lines.
Another key characteristic is the system's ability to handle long-distance conveying with minimal pressure drop. The metering bin pump's design, with its high-pressure capability, allows for the transportation of materials over significant distances without the need for intermediate booster stations. This reduces operational costs and increases the overall efficiency of the material handling system.
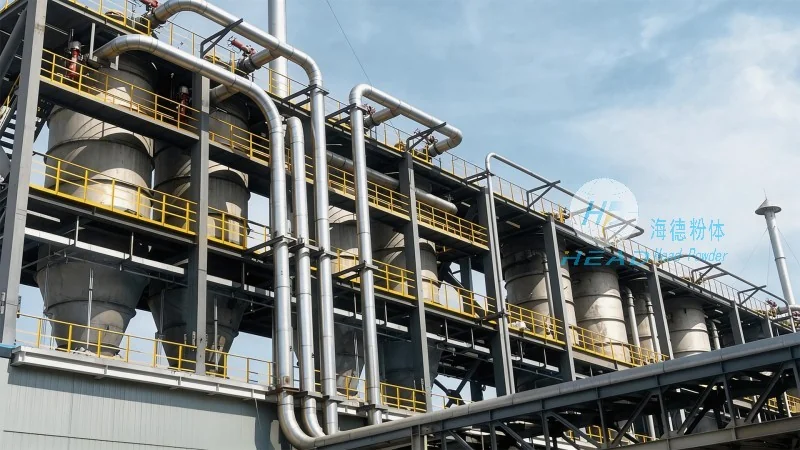
HeadPowder's metering bin pumps are widely used in various industrial sectors, each with unique working scene requirements. For instance, in the chemical industry, these pumps are used to transport reactive powders and chemicals to reactors, ensuring precise dosing and minimizing the risk of material degradation. In the pharmaceutical industry, the equipment is employed to handle active pharmaceutical ingredients (APIs) and excipients, maintaining strict contamination control and dosage accuracy.
In the food processing industry, metering bin pumps are utilized to convey ingredients such as flour, sugar, and spices, ensuring consistent quality and preventing cross-contamination. The system's ability to handle hygienic materials makes it suitable for applications where food safety is paramount. Similarly, in the mining sector, these pumps are used to transport ore and other minerals from storage bins to processing facilities, improving the efficiency of material handling operations.
From a working scene perspective, the metering bin pump offers several advantages that enhance operational performance. The compact design of the system allows for easy integration into existing facilities, reducing the need for extensive infrastructure modifications. The system's low maintenance requirements and long service life contribute to lower operational costs over time. Additionally, the ability to handle a wide range of materials without the need for pre-drying or pre-screening makes it a cost-effective solution for many industrial applications.
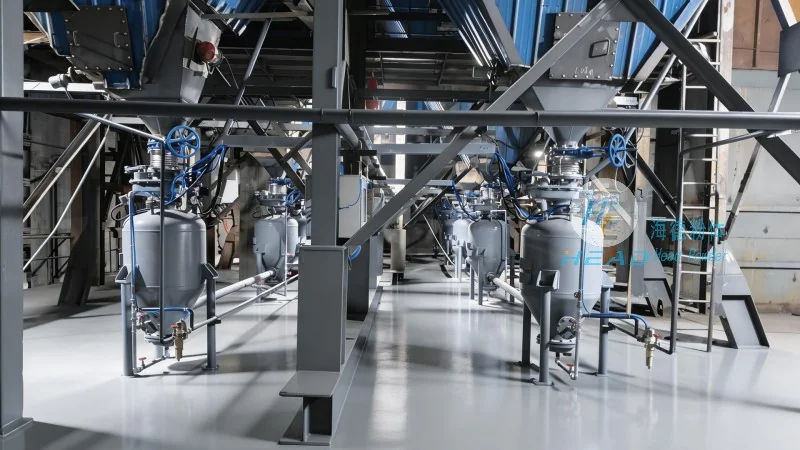
HeadPowder's commitment to quality and innovation is reflected in the performance of their metering bin pumps. The company's engineering team continuously optimizes the design of the equipment to meet the evolving needs of the industrial market. By focusing on precision, reliability, and efficiency, HeadPowder ensures that their products deliver superior performance in various working scenes, providing customers with a competitive edge in their respective industries.
In conclusion, the metering bin pump is a sophisticated piece of equipment that combines the principles of storage, metering, and pumping to efficiently transport dry bulk materials. The working scene characteristics of these systems, including their versatility, consistent flow rate, and long-distance conveying capabilities, make them a preferred choice in numerous industrial applications. HeadPowder, with its expertise in bulk material handling, continues to provide high-quality metering bin pump solutions that meet the diverse needs of its clients, ensuring optimal performance and operational efficiency in various working scenes.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top